Tag: Plant Design

  • Plant Safety Systems: Key Design Considerations for Industrial Plants

    Plant Safety Systems: Key Design Considerations for Industrial Plants

    Safety is not an add-on to plant design. It is a fundamental requirement that shapes every decision, from layout and equipment selection to operating procedures and maintenance practices. Safety systems are the engineered safeguards that protect people, the environment, and the plant itself when something goes wrong.

    For small to medium-scale industrial plants, safety systems are especially critical because there is less redundancy and fewer resources to absorb the consequences of an incident. A single safety failure can cause injury, environmental damage, or plant destruction.

    This article covers the key considerations in safety system design for industrial plants: hazard identification, risk assessment, layers of protection, safety instrumented systems, fire and gas detection, fire protection, pressure relief, emergency shutdown, alarm management, management of change, human factors, and emergency response.

    What Are Safety Systems?

    Safety systems are the engineered and procedural measures that prevent incidents, detect them when they occur, and mitigate their consequences.

    • Prevention systems: Design features, procedures, and controls that prevent hazardous conditions.
    • Detection systems: Sensors, alarms, and monitoring that detect abnormal conditions.
    • Mitigation systems: Equipment and procedures that reduce the consequences of an incident.
    • Emergency response systems: Equipment, procedures, and training for responding to incidents.

    Safety systems are not just hardware. They include procedures, training, management systems, and safety culture.

    The Layers of Protection
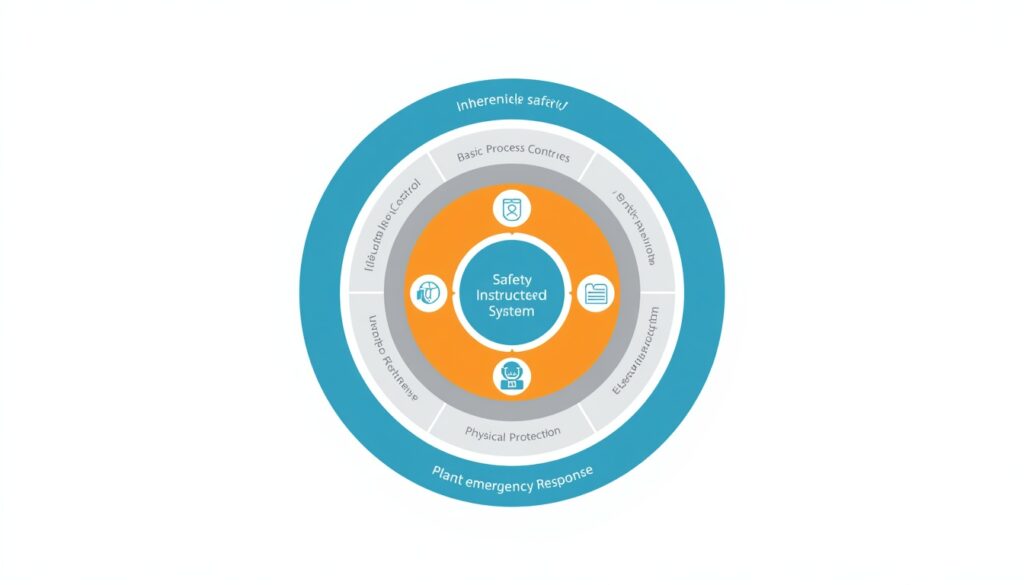
    Layers of protection in industrial plant safety design

    Safety is typically designed in layers, so that if one layer fails, others remain. This concept is called layers of protection.

    Layer Description Examples
    1. Inherent safety Design features that eliminate or reduce hazards Using less hazardous materials, reducing inventory
    2. Basic process control Control systems that keep the process within safe limits Control loops, process alarms
    3. Critical alarms and operator response Alarms that prompt operator action before a trip High-priority alarms with defined response procedures
    4. Safety instrumented systems Independent systems that bring the plant to a safe state Emergency shutdown systems
    5. Physical protection Devices that contain or relieve pressure Relief valves, rupture discs, dikes
    6. Plant emergency response Procedures and equipment for responding to incidents Fire fighting, evacuation
    7. Community emergency response External response for major incidents Fire department, emergency services

    The layers work together. No single layer is perfect, but together they provide defense in depth.

    Independence matters. In a formal analysis such as LOPA, a layer is credited as an independent protection layer (IPL) only if it is independent of the initiating event and the other layers, specific to the hazard, dependable, and auditable. For example, if the same control loop both causes a deviation and is relied on to prevent it, the two layers are not independent. Community emergency response is generally not credited as an IPL, because it does not prevent the incident.

    Hazard Identification

    Safety system design begins with hazard identification. You cannot protect against hazards you have not identified.

    Method Description Best For
    HAZOP Systematic review of process deviations using guide words Process systems
    HAZID Structured early-stage identification of hazards Concept and layout stages
    What-if analysis Brainstorming “what if” scenarios Any system
    Checklist Review against a list of known hazards Routine operations
    FMEA Identifying failure modes and their effects Equipment and systems

    For small plants, a combination of HAZOP for process systems and checklists for routine operations is often practical. HAZID is useful at the concept stage, and FMEA is used for higher-consequence equipment and systems.

    Process hazard analyses (PHAs) are not one-time exercises. They should be revalidated periodically (commonly every five years, or as required by local regulation) and whenever significant changes occur.

    Hazardous area classification. Where flammable gases, vapors, or dusts may be present, the plant must be classified into hazardous zones (for example, under IEC 60079 or NFPA 70/NEC). Classification determines the electrical equipment and ignition-source controls required, and it should be completed early, because it affects layout and equipment selection.

    Risk Assessment

    Hazard identification is followed by risk assessment. Risk is the combination of:

    • Likelihood: How likely is the hazard to cause harm?
    • Consequence: How severe would the harm be?

    Risk assessment approaches:

    • Qualitative: Using descriptive categories (high, medium, low).
    • Semi-quantitative: Using numerical scales for likelihood and consequence, such as a risk matrix or LOPA.
    • Quantitative: Using numerical probabilities and consequences (QRA).

    For most plant applications, a risk matrix or LOPA is sufficient. The result is compared with the owner’s tolerable risk criteria and determines how much protection is needed. Many organizations apply the ALARP principle (as low as reasonably practicable) to risks in the intermediate range.

    Layer of Protection Analysis (LOPA) is commonly used to determine the SIL required for a SIF. It compares the frequency of the initiating event and the protection layers already in place against the tolerable risk, and the remaining gap defines the risk reduction the SIF must provide.

    Safety Instrumented Systems (SIS)
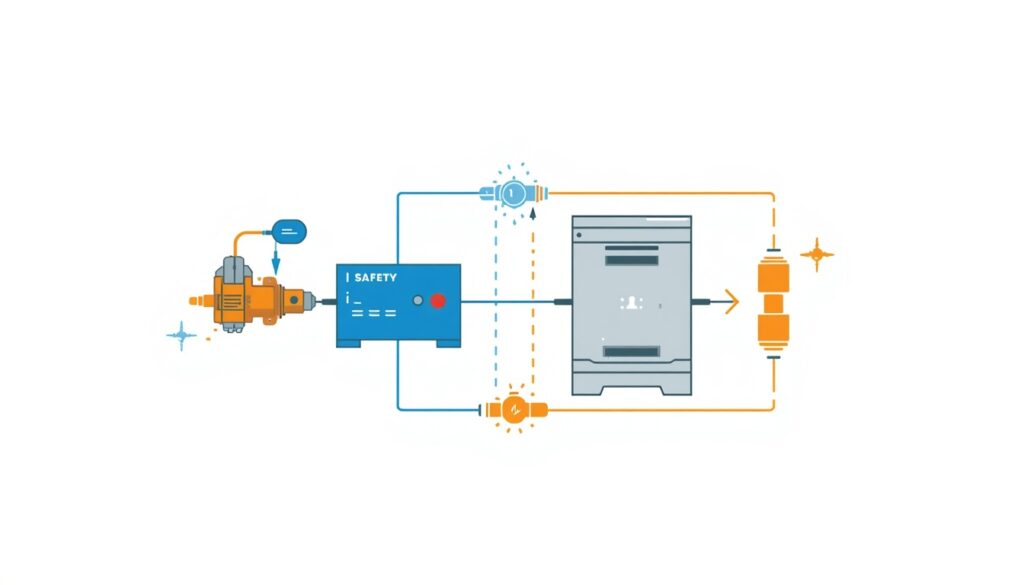
    Safety instrumented system independence from basic process control

    A Safety Instrumented System (SIS) is an independent system designed to bring the plant to a safe state when abnormal conditions occur. It is separate from the basic process control system (BPCS).

    A SIS consists of three parts:

    • Sensors: Measure process conditions (pressure, temperature, level, flow).
    • Logic solver: Evaluates the sensor signals and decides when to act.
    • Final elements: Carry out the safety action (shutdown valves, motor trips).

    Key concepts:

    • Safety Instrumented Function (SIF): A specific safety function, such as closing a valve or tripping a pump.
    • Safety Integrity Level (SIL): A measure of the reliability required for a SIF. SIL 1 is the lowest and SIL 4 the highest.
    • Proof testing: Periodic testing to verify that the SIS functions correctly and to reveal dangerous failures not detected by diagnostics.
    • Independence: The SIS must be separate from the BPCS. Any sharing of components must be justified and its effect on integrity assessed.

    SIL levels (low-demand mode):

    SIL Average Probability of Failure on Demand (PFDavg) Risk Reduction Factor Notes
    SIL 1 10⁻¹ to 10⁻² 10 to 100 Lowest required reliability
    SIL 2 10⁻² to 10⁻³ 100 to 1,000 Common in process plants
    SIL 3 10⁻³ to 10⁻⁴ 1,000 to 10,000 For the highest-consequence hazards
    SIL 4 10⁻⁴ to 10⁻⁵ 10,000 to 100,000 Outside the scope of IEC 61511; rarely applicable in process plants

    The SIL of a SIF is set by the risk reduction it must deliver, not by the general “riskiness” of the plant. For small to medium-scale plants, most SIFs are SIL 1 or SIL 2, and SIL 3 is used for the highest-consequence hazards. If a SIF would need SIL 3 or higher, consider whether the process can be made inherently safer first.

    Architecture and diagnostics. The achieved SIL depends on the failure rates of the components, the voting architecture (such as 1oo1, 1oo2, or 2oo3), diagnostic coverage, and the proof test interval. Redundant architectures can improve safety, and voting schemes such as 2oo3 can also reduce spurious trips, which are themselves a hazard because shutdowns and restarts stress the plant.

    Bypasses and overrides. Bypasses are sometimes necessary for maintenance or startup, but they remove protection. They should be authorized, time-limited, alarmed, and tracked, with compensating measures in place while they are active.

    Functional Safety Management

    SIS reliability depends not just on design but on management over the lifecycle. Functional safety management covers the entire SIS lifecycle, from hazard identification through design, installation, operation, and maintenance. It includes procedures for change management, proof testing, and competency of personnel.

    In practice, this means a defined functional safety plan, assigned responsibilities, periodic functional safety audits and assessments, and records that show each SIF continues to perform as required.

    Fire and Gas Detection

    Fire and gas detection systems detect fires, flammable gas releases, and toxic gas releases.

    Fire detection:

    • Smoke detectors: Detect smoke from combustion.
    • Heat detectors: Detect temperature rise.
    • Flame detectors: Detect ultraviolet or infrared radiation from flames.
    • Manual call points: Allow people to raise the alarm.

    Gas detection:

    • Flammable gas detectors: Detect combustible gas or vapor, typically alarming at a fraction of the lower flammable limit.
    • Toxic gas detectors: Detect toxic gases at concentrations relevant to exposure limits.

    Key considerations:

    • Coverage: Detectors must cover all areas where hazards may occur. Placement should reflect the gas density, ventilation, and likely leak sources.
    • Redundancy and voting: Critical areas may require redundant detectors and voting logic to balance reliability against spurious activation.
    • Alarm logic: Detection should trigger alarms and, where appropriate, automatic protective actions, such as shutdown, isolation, ventilation change, or suppression release.
    • Testing: Detectors must be tested and calibrated periodically.

    Fire Protection Systems

    Fire protection includes both passive and active systems.

    Passive fire protection:

    • Fire-resistant construction: Materials and assemblies that resist fire spread.
    • Fire walls and barriers: Physical barriers that contain fire.
    • Fire doors: Doors that resist fire spread.
    • Cable protection: Fire-resistant coatings or enclosures.
    • Structural fireproofing: Protection of supports for vessels and pipe racks.
    • Containment and drainage: Dikes and drainage that limit the spread of burning liquids.

    Active fire protection:

    • Sprinkler and water spray systems: Automatic water-based suppression and cooling.
    • Foam systems: For flammable liquid fires.
    • Gas suppression systems: For electrical or control rooms (for example, inert gases or clean agents). CO₂ can be lethal in occupied spaces, so it requires pre-discharge alarms, time delays, lockouts, and strict life-safety controls.
    • Fire hydrants and monitors: For manual fire fighting.
    • Fire pumps and water supply: Ensure adequate water quantity and pressure for the design fire scenario.

    For small plants, the fire protection strategy should be based on the fire hazards present, the value of the assets, and local regulations and codes (such as NFPA standards where applicable). Passive protection is especially valuable because it works without power, detection, or human action.

    Siting and layout. Spacing between units, separation of ignition sources, location of control rooms and occupied buildings, and access for emergency vehicles all reduce the consequences of an incident before any active system is needed. Layout decisions made early are the cheapest safety measures.

    Emergency Shutdown Systems

    Emergency shutdown (ESD) systems bring the plant to a safe state quickly when a serious abnormal condition occurs.

    Key considerations:

    • Shutdown philosophy: What conditions trigger a shutdown? What is the safe state?
    • Shutdown levels: Different levels for different severities (for example, unit shutdown vs. plant shutdown).
    • Valve closure times: How quickly must valves close, and do they fail to the safe position?
    • Depressurization: Where is depressurization or blowdown required?
    • Manual initiation: Push buttons in safe, accessible locations.
    • Restart procedures: How is the plant restarted safely after a shutdown?

    ESD systems are typically part of the SIS and must meet the required SIL. They are normally linked to the fire and gas system, but the interface must be clearly defined so that a detection event triggers the intended level of shutdown.

    Pressure Relief Systems

    Pressure relief systems protect equipment from overpressure. They are the last line of defense against overpressure.

    Relief device types:

    • Spring-loaded pressure relief valves: Open when pressure exceeds the set point and reclose when it falls.
    • Rupture discs: Burst at a set pressure and do not reclose.
    • Pilot-operated relief valves: Use a pilot valve to control the main valve.

    Key considerations:

    • Scenario identification: Determine credible overpressure causes, such as blocked outlet, fire exposure, thermal expansion, control valve failure, and tube rupture.
    • Sizing: Relief devices must be sized for the governing (maximum) relief case, following recognized standards such as API 520/521 and ASME Section VIII.
    • Set pressure: Set at or below the equipment’s maximum allowable working pressure (MAWP), with allowance for accumulation.
    • Discharge location: Relief discharge must be routed to a safe location, such as a flare, scrubber, or safe vent, with attention to backpressure and reaction forces.
    • Isolation valves: Block valves upstream or downstream of relief devices must be locked or car-sealed open, or otherwise controlled.
    • Testing: Relief devices must be inspected, tested, and maintained periodically.
    • Documentation: Sizing, testing, and maintenance must be documented.

    Safety Instrumented System Design

    Designing a SIS requires several steps.

    Step Description
    1. Identify SIFs Which safety functions are required?
    2. Determine SIL What SIL is required for each SIF?
    3. Prepare the safety requirements specification (SRS) What must each SIF do, how fast, and what is the safe state?
    4. Design the SIS What sensors, logic solvers, and final elements are needed?
    5. Verify SIL Does the design meet the required SIL, considering architecture, failure rates, and test intervals?
    6. Implement Install, configure, and test the SIS.
    7. Validate Confirm that the SIS functions as specified in the SRS.
    8. Operate and maintain Proof test, manage bypasses, and maintain the SIS over its life.

    SIS design must follow applicable standards, such as IEC 61511 (process industry) or IEC 61508 (general functional safety). Equivalent national adoptions, such as ANSI/ISA-61511 (formerly ISA-84), are also widely used.

    Alarm Management

    Alarms are a key layer of protection, but poorly managed alarms can overwhelm operators. Alarm management ensures that alarms are meaningful and actionable. Too many alarms, or alarms that operators routinely ignore, undermine the protection they are meant to provide.

    Good alarm management practice includes:

    • Rationalization: Each alarm has a purpose, a defined operator response, and a priority.
    • Prioritization: Critical alarms stand out from advisory ones.
    • Limiting alarm floods: Alarms during upsets should be manageable and not overwhelm the operator.
    • Change control: Alarm limits and priorities are not changed without review.
    • Performance monitoring: Alarm rates and frequently occurring “bad actors” are tracked and corrected.

    Recognized guidance includes ISA-18.2 and IEC 62682. Alarms should not be used as a substitute for a SIF where independent, automatic protection is required.

    Management of Change (MOC)

    Changes to equipment, procedures, or operating conditions can invalidate safety analyses. Management of change (MOC) ensures that changes are reviewed for safety impact before implementation. A change that seems minor can affect the validity of a HAZOP, an SIS design, or a relief system sizing.

    An effective MOC process includes:

    • Defining what counts as a change (temporary and permanent, including software and set point changes).
    • Reviewing safety, health, and environmental impact before approval.
    • Updating documentation such as P&IDs, procedures, cause-and-effect charts, and relief calculations.
    • Training affected personnel before the change is implemented.
    • Closing out temporary changes so they do not become permanent by default.

    Human Factors

    Human factors engineering considers how people interact with systems. It covers control room design, alarm presentation, procedure clarity, and workload. Good human factors design reduces the likelihood of operator error.

    Practical examples include clear and consistent control displays, logical equipment labeling, procedures that can be followed under stress, sensible shift and staffing arrangements, and operator input during design reviews. Even a well-engineered safety system can fail if operators cannot understand or use it when it matters.

    Emergency Response Planning

    Even well-designed plants must be prepared for incidents. Emergency response planning connects the plant’s safety systems with people and procedures.

    Key elements:

    • Emergency plan: Defined roles, communication, and decision authority.
    • Scenarios: Plans based on credible incidents identified in the hazard analysis (fire, toxic release, explosion, spill).
    • Alarms and communication: Ways to alert everyone on site and contact external services.
    • Evacuation and muster: Clear routes, assembly points, and headcount procedures.
    • Equipment and resources: Fire fighting equipment, first aid, spill response, and personal protective equipment.
    • Training and drills: Regular exercises, including coordination with local emergency services.
    • Review: Lessons from drills and incidents are captured and applied.

    Safety Culture

    Safety systems are only effective if they are supported by a strong safety culture.

    Key elements of safety culture:

    • Leadership commitment: Safety starts at the top.
    • Employee involvement: Workers at all levels participate in safety.
    • Open reporting: Incidents and near-misses are reported without fear.
    • Learning organization: Lessons are captured and applied.
    • Continuous improvement: Safety performance is measured and improved.

    Safety culture is not a document. It is the way people behave when no one is watching.

    Common Mistakes in Safety System Design

    Even experienced designers make mistakes. Common ones include:

    • Incomplete hazard identification: Missing hazards that later cause incidents.
    • Underestimating risk: Assuming hazards are less likely or less severe than they are.
    • Inadequate independence: SIS not truly independent of the basic control system, or protection layers that share a common cause of failure.
    • Poor proof testing: Safety systems that are not tested, or tested incorrectly.
    • Ignoring human factors: Designing systems that operators cannot use effectively.
    • Poor alarm management: Alarm floods and nuisance alarms that operators learn to ignore.
    • Weak management of change: Modifications that quietly invalidate earlier safety analyses.
    • Uncontrolled bypasses: Protection disabled and never restored.
    • Weak safety culture: Systems in place, but not respected or followed.
    • Insufficient documentation: Making it difficult to maintain and verify safety systems.

    These mistakes can have catastrophic consequences. They must be avoided through careful design, testing, and management.

    How Japanese EPC Firms Approach Safety Systems

    Japanese engineering firms are known for their disciplined approach to safety. Common characteristics include:

    • Thorough hazard identification: Hazards are identified systematically, with input from all disciplines.
    • Conservative design margins: Safety systems are designed with adequate margin for uncertainty.
    • Detailed documentation: Safety analyses, designs, and test records are carefully maintained.
    • Comprehensive testing: Safety systems are tested thoroughly before startup and periodically thereafter.
    • Disciplined change control: Changes are reviewed and documented before implementation.
    • Strong safety culture: Safety is embedded in every aspect of design, construction, and operation.
    • Long-term focus: Safety systems are maintained and improved over the plant’s life.

    For plant owners, this often means fewer incidents, better regulatory compliance, and a safer workplace.

    How to Evaluate Safety System Design

    When reviewing safety system design, ask:

    Question Why It Matters
    Have all hazards been identified? You cannot protect against unknown hazards
    Has risk been assessed consistently against defined criteria? Determines how much protection is needed
    Are protection layers independent? Ensures defense in depth
    Is the SIS designed and verified to the required SIL? Ensures safety functions are reliable enough
    Is there a functional safety management plan? Ensures reliability is maintained over the lifecycle
    Are fire and gas detection systems adequate? Detects incidents early
    Are relief systems properly sized and routed? Prevents overpressure failure
    Are alarms rationalized and manageable? Keeps operators effective during upsets
    Is there an MOC process, and is it followed? Keeps analyses valid after changes
    Is proof testing planned and performed? Verifies that safety systems work
    Are bypasses controlled? Prevents protection from being lost unnoticed
    Are emergency response plans tested? Ensures people can act when needed
    Is safety culture strong? Ensures systems are respected and followed

    A plant that addresses these questions is likely to have effective safety systems.

    Key Takeaways

    • Safety systems protect people, the environment, and the plant
    • Layers of protection provide defense in depth, but only if the layers are truly independent
    • Hazard identification is the foundation of safety design
    • Safety instrumented systems must be independent and designed to the required SIL
    • Functional safety management, alarm management, and management of change keep safety systems effective over the plant’s life
    • Human factors design reduces the likelihood of operator error
    • Fire protection includes both passive and active systems
    • Pressure relief systems are the last line of defense against overpressure
    • Safety culture determines whether systems are respected and followed
    • Japanese EPC firms emphasize thorough hazard identification and comprehensive testing

    Conclusion

    Safety systems are essential to protecting people, the environment, and the plant itself. For small to medium-scale industrial plants, safety system design deserves careful attention from the earliest stages of design.

    By focusing on hazard identification, risk assessment, layers of protection, SIS design and functional safety management, fire protection, alarm management, management of change, and safety culture, owners and designers can ensure that the plant operates safely throughout its life.
  • Plant Commissioning: Key Steps and Considerations for Successful Startup

    Plant Commissioning: Key Steps and Considerations for Successful Startup

    Commissioning is the bridge between construction and operation. It is the process of verifying that every system in the plant works as designed, that safety systems function correctly, and that the plant can operate reliably at its specified performance. A successful commissioning phase means the plant starts up smoothly, meets its performance guarantees, and is ready for handover to the owner’s operations team.

    For small to medium-scale industrial plants, commissioning is especially critical because there is less redundancy and fewer resources to manage unexpected problems. A poorly executed commissioning phase leads to delays, cost overruns, and operational problems that persist long after startup.

    This article covers the key steps and considerations in plant commissioning, from pre-commissioning checks to performance testing and handover.

    What Is Commissioning?

    Commissioning is the systematic process of testing and verifying that plant systems and equipment function according to design intent and contract requirements. It includes:

    • Pre-commissioning: Static checks, cleaning, and preparation before energization or startup.
    • Commissioning: Functional testing of individual systems and equipment.
    • Integrated testing: Testing of interconnected systems under operating conditions.
    • Performance testing: Verifying that the plant meets its contractual performance guarantees.
    • Handover: Transferring the plant to the owner’s operations team.

    Commissioning is not just a technical exercise. It is also a contractual milestone, often tied to payment and acceptance.

    Why Commissioning Matters

    Commissioning determines whether the plant:

    • Operates safely: Safety systems are tested and verified.
    • Meets design performance: Output, efficiency, and emissions are confirmed.
    • Is reliable: Equipment and systems function as intended.
    • Is ready for operation: The owner’s team is trained and documentation is complete.
    • Meets contractual requirements: Performance guarantees are verified.

    A successful commissioning phase reduces the risk of operational problems after handover. A poor one creates problems that may take months or years to resolve.

    The Commissioning Process

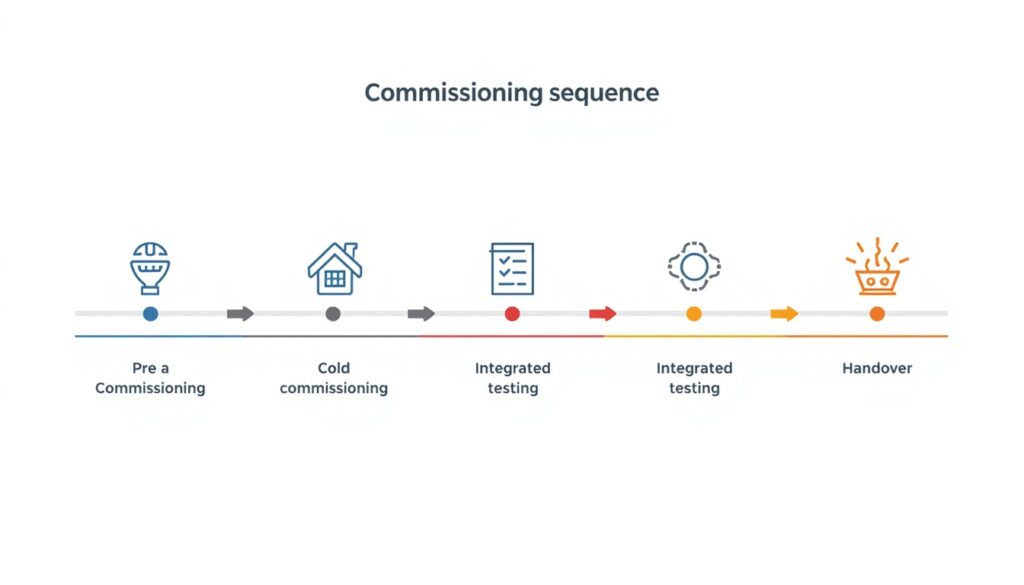
    Commissioning process sequence diagram for industrial plants

    Commissioning typically follows a structured sequence, though the exact steps depend on the plant type and contract.

    Phase Activities
    Pre-commissioning Static checks, cleaning, flushing, pressure testing, instrument calibration
    Cold commissioning Testing without process fluids or at ambient conditions
    Hot commissioning Testing with process fluids at operating conditions
    Integrated testing Testing interconnected systems under load
    Performance testing Verifying contractual performance guarantees
    Handover Documentation, training, and formal acceptance

    Each phase builds on the previous one. Skipping or rushing a phase creates problems that surface later.

    In larger projects, systems are turned over from construction to commissioning in stages, system by system, rather than all at once. This allows commissioning to begin on completed systems — such as a fuel gas system or a cooling water system — while construction continues elsewhere on the site. Staged turnover requires a clear handoff process: each system is inspected, documented, and formally accepted by the commissioning team before work on it begins, so that responsibility and accountability for that system are never ambiguous.

    Pre-Commissioning

    Pre-commissioning is the preparation phase. It includes:

    Static checks:

    • Verifying that equipment is installed correctly.
    • Checking that instruments are installed and connected.
    • Verifying that electrical connections are correct.
    • Checking that valves are in the correct position.

    Cleaning and flushing:

    • Removing debris, scale, and contaminants from piping and equipment.
    • Flushing oil systems, water systems, and process lines.
    • Cleaning tanks and vessels.

    Pressure testing:

    • Hydrostatic or pneumatic testing of piping and vessels.
    • Verifying that systems can withstand design pressure without leaking.

    Instrument calibration:

    • Calibrating instruments to ensure accurate measurement.
    • Verifying signal transmission and control system response.

    Safety system checks:

    • Verifying that safety interlocks and shutdown systems function correctly.
    • Testing alarms and trips.

    Pre-commissioning is often the most time-consuming phase. Rushing it leads to problems during commissioning.

    Equipment that is installed but not yet commissioned must be preserved according to vendor requirements during this period. This includes protection from moisture, corrosion, and mechanical damage — for example, maintaining nitrogen purges on idle piping, running space heaters in motors and switchgear, and keeping rotating equipment on periodic turning or lubrication cycles. Preservation gaps are easy to overlook on a busy site, but they can cause damage that only shows up once a system is finally started, well after the responsible party has moved on to other work.

    Cold Commissioning

    Cold commissioning tests systems without process fluids or at ambient conditions. It includes:

    • Motor rotation checks: Verifying that motors rotate in the correct direction.
    • Pump and fan testing: Verifying that equipment operates without load.
    • Control loop testing: Verifying that control loops respond correctly.
    • Valve operation: Verifying that valves open, close, and modulate correctly.
    • Interlock testing: Verifying that safety interlocks function correctly.

    Cold commissioning verifies that systems work mechanically and electrically before introducing process fluids.

    Hot Commissioning

    Hot commissioning tests systems with process fluids at operating conditions. It includes:

    • System startup: Starting up individual systems and verifying operation.
    • Process parameter verification: Confirming that temperature, pressure, flow, and other parameters meet design values.
    • Control loop tuning: Tuning controllers for stable, responsive control.
    • Equipment performance: Verifying that equipment operates within design parameters.
    • Emissions testing: Initial checks that emissions are within expected ranges under real operating conditions.

    Hot commissioning is where many problems surface. It requires close coordination between the contractor, owner, and equipment vendors.

    Integrated Testing

    Integrated testing verifies that interconnected systems work together under operating conditions. It includes:

    • Full plant operation: Operating the plant as a whole, not just individual systems.
    • Load testing: Operating at various loads to verify performance across the operating range.
    • Transient testing: Testing response to load changes, trips, and other disturbances.
    • Safety system verification: Verifying that safety systems function correctly under realistic conditions.

    Integrated testing is where the plant is proven as a complete system, not just a collection of components.

    Performance Testing

    Performance testing during plant commissioning

    Performance testing verifies that the plant meets its contractual performance guarantees. It includes:

    • Output testing: Verifying that the plant produces the guaranteed output.
    • Heat rate testing: Verifying that the plant meets its guaranteed efficiency.
    • Emissions testing: Verifying that emissions meet guaranteed or regulatory limits, under the formal test conditions specified in the contract.
    • Availability and reliability: Some contracts require demonstration of availability or reliability over a defined period.

    Performance testing must follow the procedures specified in the contract, including reference conditions, test methods, and measurement uncertainty.

    Handover

    Handover is the formal transfer of the plant from the contractor to the owner. It includes:

    • Documentation: As-built drawings, equipment manuals, operating procedures, and maintenance schedules.
    • Training: Training the owner’s operations and maintenance team.
    • Spare parts: Delivering spare parts and consumables.
    • Warranty documentation: Confirming warranty terms and procedures.
    • Formal acceptance: Signing off that the plant meets contractual requirements.

    Incomplete handover documentation is a common source of problems during the first years of operation.

    Operator training often begins during commissioning, not just at handover. Operators who participate in commissioning — observing cold and hot commissioning, and ideally assisting with integrated testing — gain valuable familiarity with the plant’s actual behavior before they take over operation. This hands-on exposure is generally far more effective than classroom training alone, since it lets operators see how the plant actually responds rather than only how it is supposed to respond on paper.

    A punch list is a record of outstanding items that must be completed before handover. Items are typically categorized by priority, with safety-critical items addressed first, followed by performance-affecting items, and finally minor or cosmetic items. The punch list is developed collaboratively by the contractor, owner, and commissioning team throughout the commissioning process, not just compiled at the end, and it is cleared — or formally accepted with an agreed completion plan for any remaining items — before formal acceptance.

    Key Considerations for Successful Commissioning

    1. Planning

    Commissioning must be planned from the earliest stages of the project. The commissioning plan defines sequence, responsibilities, resources, and milestones.

    2. Roles and Responsibilities

    Clear roles and responsibilities are essential. The contractor, owner, equipment vendors, and commissioning specialists must all know what they are responsible for.

    A commissioning manager is typically appointed to lead the commissioning effort. This person coordinates between the contractor, owner, vendors, and commissioning specialists, and is responsible for the commissioning plan, schedule, and documentation. On smaller projects this role may be combined with other project responsibilities, but the function itself — a single point of accountability for commissioning progress and decisions — should not be skipped, since fragmented ownership of commissioning is a common cause of delay.

    3. Safety

    Commissioning involves energizing equipment, introducing process fluids, and operating at high temperatures and pressures. Safety procedures must be in place and followed.

    4. Documentation

    Commissioning records must be complete and accurate. These records support performance testing, handover, and future maintenance.

    5. Coordination

    Commissioning requires coordination between multiple parties. Regular meetings and clear communication help avoid delays and misunderstandings.

    6. Contingency Planning

    Problems arise during commissioning. Contingency plans help address them without derailing the schedule.

    Common Problems During Commissioning

    Even well-planned commissioning encounters problems. Common ones include:

    • Incomplete pre-commissioning: Leading to problems during hot commissioning.
    • Instrument calibration errors: Causing inaccurate readings and poor control.
    • Control loop tuning problems: Causing instability or poor response.
    • Equipment failures: Leading to delays and rework.
    • Safety system issues: Requiring redesign or modification.
    • Documentation gaps: Making handover difficult.
    • Schedule pressure: Leading to rushed testing and missed problems.

    These problems are costly to resolve after startup. They are much cheaper to avoid through careful planning and execution.

    How Japanese EPC Firms Approach Commissioning

    Japanese engineering firms are known for their disciplined approach to commissioning. Common characteristics include:

    • Thorough pre-commissioning: Static checks, cleaning, and calibration are completed carefully before startup.
    • Detailed planning: Commissioning sequences, responsibilities, and contingencies are planned in advance.
    • Comprehensive documentation: Commissioning records, test results, and as-built documentation are carefully maintained.
    • Integrated teams: Contractor, owner, and vendor personnel work closely together.
    • Long-term focus: Commissioning is treated as the foundation for reliable long-term operation, not just a milestone to pass.

    For plant owners, this often means a smoother startup, fewer surprises, and a plant that is ready for reliable operation from day one.

    How to Evaluate Commissioning Planning

    When reviewing commissioning planning, ask:

    Question Why It Matters
    Is there a detailed commissioning plan? Defines sequence, responsibilities, and milestones
    Are roles and responsibilities clear? Avoids confusion and delays
    Is pre-commissioning thorough? Prevents problems during hot commissioning
    Are safety procedures in place? Protects personnel and equipment
    Is documentation complete? Supports performance testing and handover
    Are contingencies planned? Helps address problems without derailing schedule
    Is the owner involved early? Ensures smooth handover and operation

    A commissioning plan that addresses these questions is likely to deliver a successful startup.

    Key Takeaways

    • Commissioning verifies that systems work as designed before handover.
    • The process includes pre-commissioning, cold, hot, integrated, and performance testing.
    • Pre-commissioning is often the most time-consuming phase, and equipment awaiting commissioning must be properly preserved.
    • In larger projects, systems are turned over from construction to commissioning in stages.
    • A commissioning manager provides a single point of accountability for the commissioning effort.
    • Operator training often begins during commissioning, not just at handover.
    • Punch lists track outstanding items by priority and are cleared before formal acceptance.
    • Performance testing verifies contractual guarantees.
    • Handover includes documentation, training, and formal acceptance.
    • Japanese EPC firms emphasize thorough pre-commissioning and detailed planning.

    Conclusion

    Commissioning is the bridge between construction and operation. It determines whether the plant starts up smoothly, meets its performance guarantees, and is ready for reliable operation. For small to medium-scale industrial plants, commissioning deserves careful planning and execution from the earliest stages of the project.

    By focusing on pre-commissioning, phased testing, documentation, and coordination, owners and contractors can ensure a successful startup and a smooth transition to operation.

  • Insulation and Refractory Systems for Industrial Plants: Key Design Considerations

    Insulation and Refractory Systems for Industrial Plants: Key Design Considerations

    Insulation and refractory systems are essential to plant efficiency, safety, and equipment longevity. Insulation reduces heat loss from hot surfaces and prevents heat gain on cold surfaces. Refractory protects equipment from extreme temperatures and chemical attack. Together, they determine how much energy the plant consumes, how safe it is to operate, and how long critical equipment lasts.

    For small to medium-scale industrial plants, insulation and refractory design is especially critical because there is less margin for error and fewer resources to manage unexpected failures. Poor insulation increases operating cost and creates safety hazards. Poor refractory leads to equipment damage and unplanned outages.

    This article covers the key considerations in insulation and refractory system design for industrial plants, from material selection to installation and maintenance.

    The Role of Insulation

    Insulation serves several essential functions in an industrial plant:

    Energy efficiency: Reducing heat loss from hot surfaces and heat gain on cold surfaces.

    Personnel protection: Preventing burns from hot surfaces and frostbite from cold surfaces.

    Process control: Maintaining process temperatures within required limits.

    Condensation control: Preventing condensation on cold surfaces.

    Freeze protection: Preventing liquids from freezing in cold weather.

    Noise reduction: Some insulation materials also provide acoustic insulation.

    Without proper insulation, a plant consumes more energy, operates less safely, and may not meet process requirements.

    The Role of Refractory

    Refractory materials protect equipment from extreme temperatures and chemical attack. They are used in:

    Boilers and furnaces: Lining the combustion chamber.

    Incinerators: Protecting the shell from high-temperature gases.

    Kilns: Lining the rotating drum.

    Reactor vessels: Protecting the shell from process temperatures.

    Ductwork and stacks: Protecting from hot exhaust gases.

    Refractory must withstand high temperatures, thermal cycling, chemical attack, and mechanical abrasion. Failure leads to equipment damage, energy loss, and safety hazards.

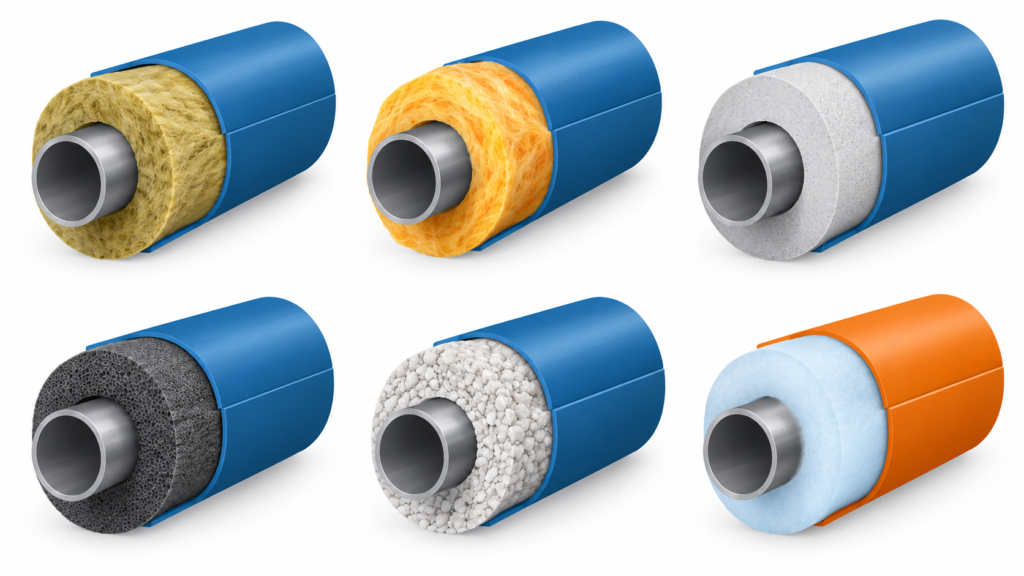
    Insulation Materials

    Common insulation materials for industrial plants

    Common insulation materials for industrial plants

    Insulation materials vary widely in temperature range, thermal conductivity, and cost.

    Material Temperature Range Characteristics Typical Use
    Mineral wool Up to 650°C Good thermal performance, fire-resistant Pipes, vessels, equipment
    Fiberglass Up to 450°C Lightweight, economical Pipes, ducts, equipment
    Calcium silicate Up to 650°C High strength, moisture-resistant Pipes, vessels
    Cellular glass Up to 430°C Closed-cell, moisture-resistant Cold surfaces, underground
    Perlite Up to 650°C Lightweight, thermal-resistant Vessels, equipment
    Aerogel Up to 650°C Excellent thermal performance, thin profile Space-constrained applications
    Polyurethane foam Up to 120°C Excellent for cold service Cold pipes, tanks
    Elastomeric foam Up to 120°C Flexible, closed-cell HVAC, cold service

    Selection depends on temperature, environment, mechanical requirements, and cost.

    Insulation Forms

    Insulation is supplied in several forms, each suited to different applications.

    Form Characteristics Typical Use
    Board Rigid or semi-rigid panels Vessels, tanks, large ducts
    Blanket Flexible, rolled Large surfaces, irregular shapes
    Pipe section Pre-formed cylindrical Pipes
    Block Rigid, molded Vessels, equipment
    Foam Sprayed or poured Complex shapes, voids

    The form affects installation speed, fit, and performance. Pre-formed pipe sections are faster to install than blankets on pipes, but blankets may be better for irregular shapes.

    Refractory Materials

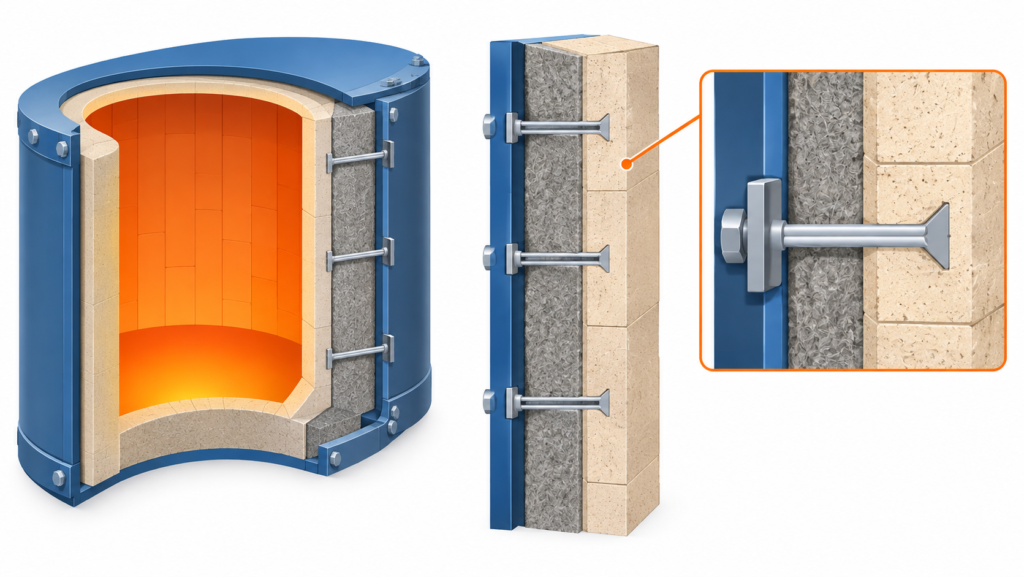
    Refractory lining cross-section for industrial furnaces

    Refractory lining cross-section for industrial furnaces

    Refractory materials are classified by their chemical composition and temperature resistance.

    Material Temperature Range Characteristics Typical Use
    Fireclay brick Up to 1,400°C Economical, moderate resistance Boilers, furnaces
    High-alumina brick Up to 1,800°C High temperature resistance High-temperature furnaces
    Silica brick Up to 1,700°C Resistance to acid slags Glass furnaces, coke ovens
    Magnesia brick Up to 2,000°C Resistance to basic slags Steel furnaces
    Castable refractory Varies Easy to install, complex shapes Boilers, incinerators
    Ceramic fiber Up to 1,400°C Lightweight, low thermal mass Furnace linings, seals

    Selection depends on temperature, atmosphere, slag composition, and mechanical requirements.

    Key Design Considerations for Insulation

    1. Temperature Range

    Insulation must be rated for the maximum operating temperature and any transient excursions.

    2. Thermal Performance

    Insulation thickness determines heat loss or gain. Thicker insulation reduces energy loss but increases cost and space requirements. The economic thickness of insulation is the thickness that minimizes total cost—capital cost plus the present value of energy losses over the plant’s life. It depends on energy prices, insulation cost, and the expected service life.

    3. Moisture Resistance

    Moisture reduces insulation performance and causes corrosion under insulation (CUI). Closed-cell materials and vapor barriers help prevent moisture ingress. Cold service insulation must prevent condensation and ice formation. Vapor barriers are critical to keep moisture out, and closed-cell materials are often preferred because they do not absorb water.

    4. Mechanical Protection

    Insulation must be protected from mechanical damage by metal jacketing, cladding, or coatings.

    5. Fire Safety

    Insulation materials must meet fire safety requirements. Some materials are non-combustible; others require fire-retardant treatments.

    6. Installation and Maintenance

    Insulation must be installed correctly and maintained over time. Damaged insulation must be repaired promptly.

    Key Design Considerations for Refractory

    1. Temperature and Atmosphere

    Refractory must withstand the maximum temperature and the chemical composition of the atmosphere (oxidizing, reducing, or corrosive).

    2. Thermal Cycling

    Refractory in cycling service experiences thermal expansion and contraction. Design must accommodate this without cracking or spalling.

    3. Mechanical Loads

    Refractory must withstand mechanical loads from the process, including abrasion from solids and impact from materials.

    4. Anchoring

    Refractory must be properly anchored to the equipment shell. Anchors must withstand temperature and corrosion. Refractory anchors are typically made from heat-resistant alloys or ceramics. They must be designed to withstand thermal expansion, corrosion, and mechanical loads without failing.

    5. Installation

    Refractory installation requires skilled labor and careful quality control. Improper installation leads to premature failure. New refractory must be dried out gradually before service. A controlled heat-up schedule removes moisture and allows the refractory to cure without cracking. Skipping this step can cause premature failure.

    6. Maintenance

    Refractory degrades over time and requires inspection and repair. Regular inspection helps detect problems before failure.

    Common Problems

    Insulation problems:

    Corrosion under insulation (CUI): Hidden corrosion caused by moisture trapped against the metal surface.

    Insulation damage: Mechanical damage, water ingress, or UV degradation.

    Thermal bridging: Heat conducting through supports or penetrations.

    Incorrect thickness: Insufficient insulation causing excessive heat loss.

    Poor installation: Gaps, compression, or inadequate fastening.

    Refractory problems:

    Cracking: Due to thermal cycling or thermal shock.

    Spalling: Surface layers breaking away.

    Erosion: Gradual wear from abrasive materials.

    Chemical attack: Reaction with slags, gases, or liquids.

    Anchor failure: Corrosion or thermal fatigue of anchors.

    These problems reduce efficiency, increase maintenance cost, and can lead to equipment failure.

    Key Design Considerations for Both Systems

    1. Material Compatibility

    Insulation and refractory materials must be compatible with the process environment, temperature, and chemicals.

    2. Expansion and Contraction

    Both systems must accommodate thermal expansion and contraction without damage.

    3. Support and Attachment

    Insulation and refractory must be properly supported and attached. Supports must withstand temperature and corrosion.

    4. Access for Maintenance

    Insulation and refractory must be accessible for inspection and repair. Access panels and removable sections help.

    5. Documentation

    Material specifications, installation procedures, inspection records, and maintenance history must be documented.

    Common Mistakes in Insulation and Refractory Design

    Even experienced designers make mistakes. Common ones include:

    Underspecifying insulation thickness: Leading to excessive energy loss.

    Ignoring CUI: Failing to design insulation to prevent moisture ingress.

    Wrong refractory for the application: Causing premature failure.

    Inadequate anchoring: Leading to refractory failure.

    Poor installation: Gaps, compression, or inadequate fastening.

    No access for maintenance: Making inspection and repair difficult.

    Insufficient documentation: Making it difficult to troubleshoot and maintain.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Insulation and Refractory

    Japanese engineering firms are known for their disciplined approach to insulation and refractory design. Common characteristics include:

    Thorough material selection: Materials are selected for the specific temperature, atmosphere, and mechanical conditions.

    Detailed specifications: Insulation thickness, refractory composition, anchoring, and installation procedures are carefully specified.

    Quality control during installation: Installation is inspected and documented.

    Comprehensive maintenance planning: Inspection intervals, repair procedures, and replacement schedules are planned.

    Long-term reliability focus: Designs prioritize reliability and maintainability over lowest initial cost.

    For plant owners, this often means lower energy costs, longer equipment life, and fewer unplanned outages.

    How to Evaluate Insulation and Refractory Design

    When reviewing insulation and refractory design, ask:

    Question Why It Matters
    Are materials rated for the actual temperature and environment? Ensures reliable performance
    Is insulation thickness optimized for energy and cost? Balances capital and operating cost
    Is CUI prevention addressed? Prevents hidden corrosion
    Is refractory suitable for the process atmosphere? Prevents premature failure
    Is anchoring designed for thermal and mechanical loads? Prevents refractory failure
    Is access provided for inspection and maintenance? Enables long-term reliability
    Is documentation complete? Supports troubleshooting and maintenance

    A design that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Insulation reduces energy loss, protects personnel, and controls process temperature
    • Refractory protects equipment from extreme temperatures and chemical attack
    • Material selection depends on temperature, environment, and mechanical requirements
    • CUI prevention is critical for insulation design
    • Refractory anchoring and dry-out are critical for reliable performance
    • Japanese EPC firms emphasize thorough material selection and quality control during installation

    Conclusion

    Insulation and refractory systems are essential to plant efficiency, safety, and equipment longevity. For small to medium-scale industrial plants, insulation and refractory design deserves careful attention from the earliest stages of design. By focusing on material selection, installation quality, and maintenance planning, owners and designers can ensure reliable performance for decades.

  • Corrosion Control in Industrial Plants: Materials, Coatings, and Cathodic Protection

    Corrosion Control in Industrial Plants: Materials, Coatings, and Cathodic Protection

    Corrosion is one of the most persistent and costly problems in industrial plants. It attacks pipes, tanks, structures, and equipment, reducing their strength, causing leaks, and eventually leading to failure. According to industry studies, corrosion costs industrial plants billions of dollars annually in maintenance, repair, and lost production.

    For small to medium-scale industrial plants, corrosion control is especially critical because there is less redundancy and fewer resources to manage unexpected failures. A corroded pipe that leaks or bursts can shut down the plant, create safety hazards, and require costly repairs.

    This article covers the fundamentals of corrosion control in industrial plants, including the mechanisms of corrosion, material selection, coatings, cathodic protection, and monitoring.

    What Is Corrosion?

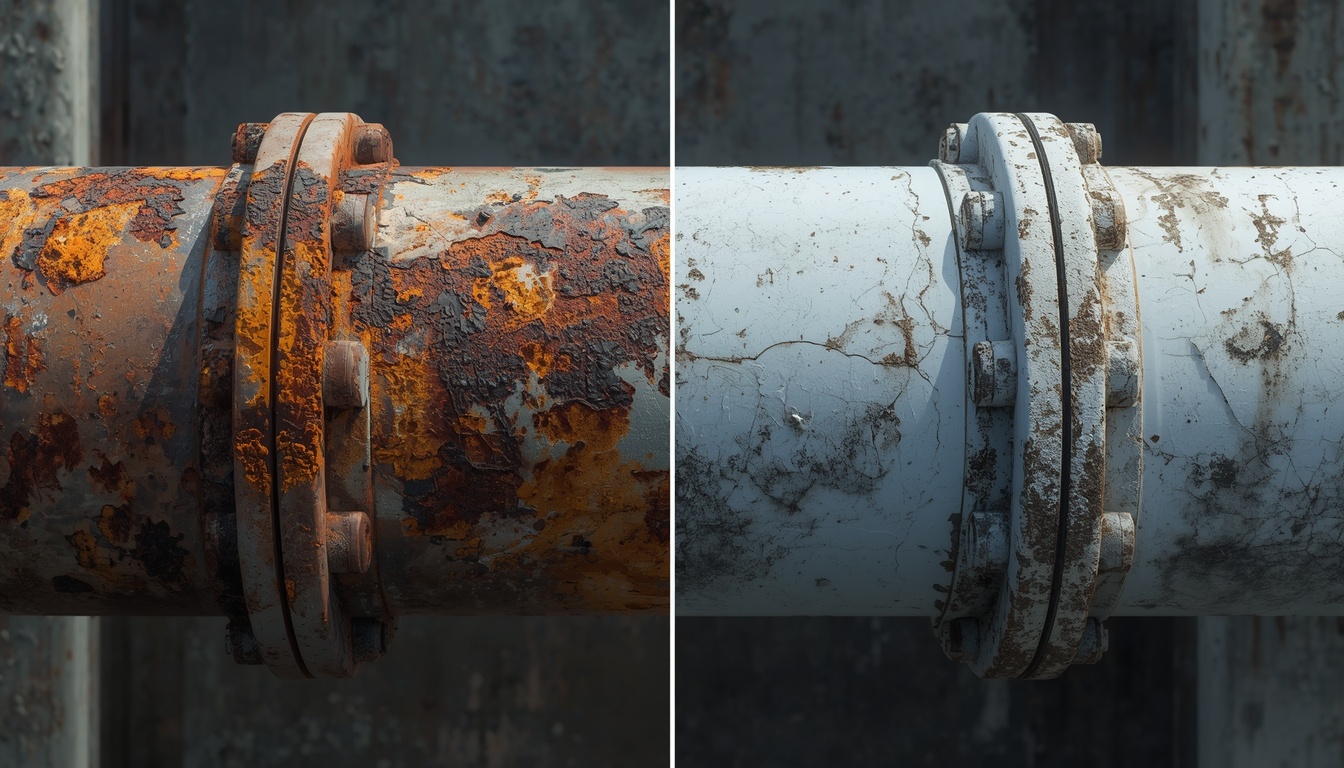
    Corrosion is the deterioration of a material—usually a metal—due to chemical or electrochemical reaction with its environment. For iron and steel, corrosion typically takes the form of rust, which is iron oxide.

    Corrosion occurs when three conditions are present:

    • An anode: The site where metal dissolves.
    • A cathode: The site where reduction occurs.
    • An electrolyte: A conductive medium (water, soil, or humid air) that connects the anode and cathode.

    If any of these three is eliminated, corrosion stops. Corrosion control strategies work by interrupting one or more of these conditions.

    Common Types of Corrosion

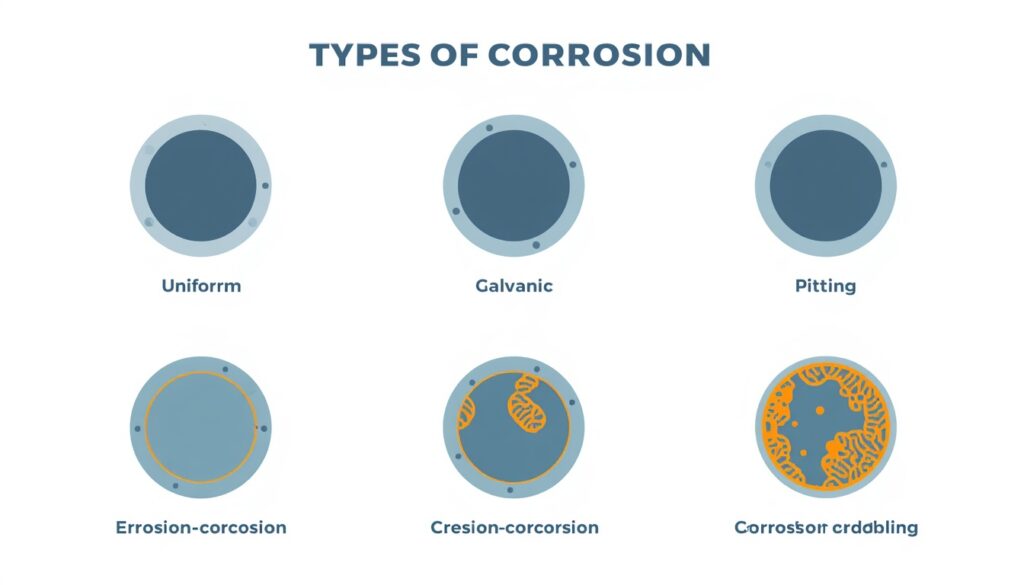
    Types of corrosion in industrial plants

    Corrosion takes many forms. Understanding the type helps in selecting the right control method.

    Type Description Typical Locations
    Uniform corrosion Even attack over the entire surface Carbon steel in general service
    Galvanic corrosion Attack at the junction of dissimilar metals Flanges, fittings, transitions
    Pitting corrosion Localized attack creating deep pits Stainless steels in chloride environments
    Crevice corrosion Attack in stagnant crevices Gaskets, bolt holes, under deposits
    Erosion-corrosion Accelerated attack due to flow Pumps, bends, tees
    Stress corrosion cracking Cracking under combined stress and corrosive environment High-temperature, chloride environments
    Microbiologically influenced corrosion (MIC) Corrosion caused by microorganisms Cooling water, stagnant areas

    Different types of corrosion require different control strategies. A single approach is rarely sufficient.

    One form worth calling out on its own is corrosion under insulation (CUI). It is a particularly insidious form of corrosion because it is hidden from view. Insulation can trap moisture against the metal surface, causing corrosion that goes undetected until failure. Proper insulation design, including vapor barriers and drainage, is essential. (This topic is covered in more detail in the piping systems article.)

    Material Selection

    The first line of defense against corrosion is selecting the right material.

    Common materials and their corrosion resistance:

    Material Corrosion Resistance Typical Use
    Carbon steel Low to moderate General service with protective measures
    Stainless steel High (with limitations) Corrosive fluids, food and pharmaceutical
    Duplex stainless steel Very high Chloride environments, seawater
    Nickel alloys Excellent Highly corrosive environments
    Titanium Excellent Seawater, oxidizing chemicals
    Copper alloys Moderate to high Heat exchangers, potable water
    Plastics (PVC, CPVC, HDPE) High Chemicals, water
    FRP (fiberglass reinforced plastic) High Corrosive chemicals

    Material selection depends on:

    • Fluid composition: What chemicals are present, and at what concentration?
    • Temperature: Higher temperatures usually accelerate corrosion.
    • Pressure: Higher pressures require stronger materials.
    • Environment: External corrosion from salt air, chemicals, or soil.
    • Cost: Material cost and life-cycle cost both matter.

    In piping and vessel design, a corrosion allowance is often added to wall thickness to account for expected metal loss over the plant’s life. This is extra wall thickness added to piping and vessels to account for expected metal loss over the design life. The allowance depends on the corrosion rate, the design life, and the required safety margin.

    Protective Coatings

    Coatings provide a barrier between the metal and the corrosive environment. They are one of the most common and cost-effective corrosion control methods.

    Common coating types:

    Coating Type Characteristics Typical Use
    Epoxy Excellent adhesion, chemical resistance Tanks, pipes, structures
    Polyurethane Good weather resistance External surfaces
    Zinc-rich primers Sacrificial protection Steel structures, tanks
    Fusion-bonded epoxy (FBE) Excellent for buried pipelines Buried pipe
    Concrete Mechanical protection, alkaline Buried pipe, marine structures

    Key considerations for coatings:

    • Surface preparation: The surface must be clean, dry, and properly profiled.
    • Application: Coating must be applied at the correct thickness and under the right conditions.
    • Inspection: Coating defects must be detected and repaired.
    • Maintenance: Coatings degrade over time and require repair or replacement.

    Coating failures are often due to poor surface preparation, not the coating itself.

    Cathodic Protection

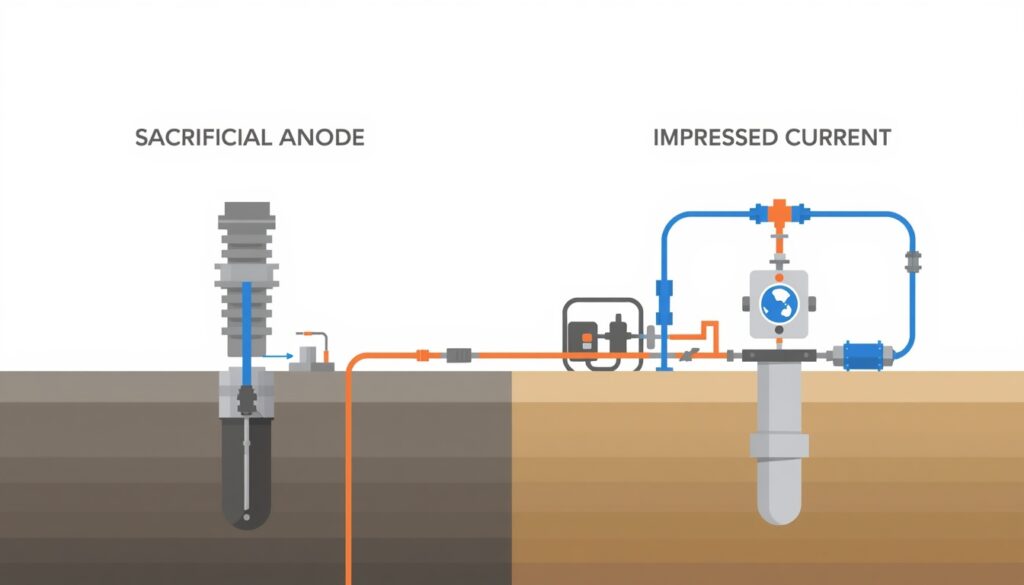
    Sacrificial anode and impressed current cathodic protection systems

    Cathodic protection (CP) is an electrochemical method of corrosion control. It works by making the metal to be protected the cathode of an electrochemical cell, so that it does not corrode.

    There are two main types:

    1. Sacrificial anode systems: A more active metal (such as zinc, aluminum, or magnesium) is connected to the protected structure. The anode corrodes instead of the structure.

    • Simple, no external power required.
    • Suitable for small structures and low-resistivity environments.
    • Anodes must be replaced periodically.

    2. Impressed current systems: An external DC power source supplies current to the structure through an inert anode.

    • Suitable for large structures and high-resistivity environments.
    • Requires external power and regular maintenance.
    • Can be adjusted to meet changing conditions.

    Cathodic protection is commonly used for:

    • Buried pipelines
    • Storage tank bottoms
    • Marine structures
    • Underground tanks

    Corrosion Inhibitors

    Corrosion inhibitors are chemicals that reduce corrosion rates by forming protective films on metal surfaces or by altering the environment. Common types include anodic inhibitors, cathodic inhibitors, and mixed inhibitors. Selection depends on the fluid, material, and operating conditions.

    Corrosion Monitoring

    Monitoring helps detect corrosion before it causes failure.

    Common monitoring methods:

    Method What It Measures Typical Use
    Visual inspection Visible corrosion Accessible surfaces
    Ultrasonic thickness Wall thickness Pipes, tanks, vessels
    Coupons Corrosion rate Process streams
    Electrical resistance probes Corrosion rate Process streams
    Linear polarization resistance (LPR) Corrosion rate Cooling water, process water
    Hydrogen probes Hydrogen permeation High-temperature, sour service

    Monitoring data helps schedule maintenance, adjust treatment programs, and verify that corrosion control measures are working.

    Corrosion Control in Specific Systems

    Different plant systems require different corrosion control strategies.

    Cooling water systems:

    • Chemical inhibitors (corrosion inhibitors, scale inhibitors, biocides)
    • Material selection (stainless steel, copper alloys)
    • Cathodic protection for critical components

    Boiler systems:

    • Water treatment (oxygen removal, pH control)
    • Chemical treatment (oxygen scavengers, pH adjusters)
    • Material selection

    Piping systems:

    • Material selection
    • Coatings (internal and external)
    • Cathodic protection for buried pipes
    • Corrosion monitoring (ultrasonic thickness)
    • Insulation design that avoids trapping moisture, to prevent corrosion under insulation (CUI)

    Storage tanks:

    • Coatings (internal and external)
    • Cathodic protection (tank bottoms)
    • Corrosion monitoring

    Structures:

    • Coatings (external)
    • Cathodic protection (buried or submerged)
    • Material selection

    Key Design Considerations

    1. Corrosion Risk Assessment Identify where corrosion is likely to occur and what type is expected. This determines the control strategy.

    2. Material Selection Select materials compatible with the fluid, temperature, pressure, and environment.

    3. Protective Measures Combine coatings, cathodic protection, and chemical treatment as needed. No single method is sufficient for all situations.

    4. Monitoring Implement monitoring to detect corrosion before it causes failure.

    5. Maintenance Inspect, repair, and replace coatings and anodes as needed.

    6. Documentation Record material selection, coating specifications, cathodic protection design, and monitoring data.

    Corrosion Management Programs

    Corrosion control is not just a design issue. It requires an ongoing program. An effective corrosion management program includes regular inspection, monitoring, maintenance, and documentation. It assigns responsibility for corrosion control and ensures that issues are identified and addressed before they cause failure.

    Common Mistakes in Corrosion Control

    Even experienced designers make mistakes. Common ones include:

    • Selecting the wrong material: Incompatible with the fluid or environment.
    • Poor surface preparation: Causing coating failure.
    • Inadequate cathodic protection design: Failing to protect the entire structure.
    • Ignoring monitoring: Discovering corrosion only after failure.
    • Skipping maintenance: Letting coatings and anodes degrade.
    • Incomplete documentation: Making it difficult to troubleshoot and maintain.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Corrosion Control

    Japanese engineering firms are known for their disciplined approach to corrosion control. Common characteristics include:

    • Thorough risk assessment: Corrosion risks are identified early in design.
    • Conservative material selection: Materials are selected with adequate margin for the expected environment.
    • Detailed coating specifications: Surface preparation, application, and inspection are carefully specified.
    • Comprehensive monitoring: Corrosion is monitored throughout the plant’s life.
    • Long-term maintenance focus: Corrosion control is treated as an ongoing responsibility, not a one-time design decision.

    For plant owners, this often means lower maintenance costs and fewer unexpected failures over the plant’s life.

    How to Evaluate Corrosion Control Design

    When reviewing corrosion control design, ask:

    Question Why It Matters
    Has a corrosion risk assessment been performed? Identifies where corrosion is likely
    Are materials compatible with the fluid and environment? Prevents corrosion from the start
    Are coatings properly specified? Ensures effective barrier protection
    Is cathodic protection designed correctly? Ensures complete protection
    Is monitoring in place? Detects corrosion before failure
    Is maintenance planned? Ensures long-term effectiveness
    Is documentation complete? Supports troubleshooting and maintenance

    A design that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Corrosion requires an anode, a cathode, and an electrolyte
    • Common types include uniform, galvanic, pitting, crevice, erosion-corrosion, and MIC
    • Material selection is the first line of defense
    • Coatings provide a barrier between metal and environment
    • Cathodic protection uses sacrificial anodes or impressed current
    • Monitoring detects corrosion before failure
    • Japanese EPC firms emphasize thorough risk assessment and conservative material selection

    Conclusion

    Corrosion is a persistent and costly problem in industrial plants, but it can be controlled. By combining material selection, coatings, cathodic protection, and monitoring, owners and designers can protect equipment and structures from corrosion and extend their service life.

    For small to medium-scale industrial plants, where margins are tight, corrosion control deserves careful attention from the earliest stages of design.

  • Piping Systems for Industrial Plants: Key Design Considerations

    Piping Systems for Industrial Plants: Key Design Considerations

    Piping systems are the circulatory system of an industrial plant. They transport fluids—water, steam, fuel, chemicals, and gases—between equipment and processes. A well-designed piping system ensures reliable flow, minimizes pressure loss, and operates safely for decades. A poorly designed system causes pressure drops, vibration, corrosion, and leaks that disrupt operations and create safety hazards.

    For small to medium-scale industrial plants, piping design is especially critical because there is less redundancy and fewer resources to manage complexity. Piping often represents a significant portion of total plant cost, and mistakes are expensive to correct after construction.

    This article covers the key considerations in piping system design for industrial plants, from material selection to layout, support, and testing.

    The Role of Piping Systems

    Piping systems perform several essential functions:

    • Transport: Moving fluids from one point to another.
    • Containment: Keeping fluids safely contained under pressure and temperature.
    • Isolation: Allowing sections of the system to be isolated for maintenance or emergencies.
    • Control: Working with valves and instruments to regulate flow, pressure, and temperature.
    • Protection: Safely relieving excess pressure through relief valves and venting.

    Piping is not just a collection of pipes. It is a system that includes pipe, fittings, valves, flanges, gaskets, supports, insulation, and instruments. All components must work together to ensure safe, reliable operation.

    Piping Materials

    Material selection is one of the most important decisions in piping design. The material must be compatible with the fluid, temperature, pressure, and environment.

    Common piping materials include:

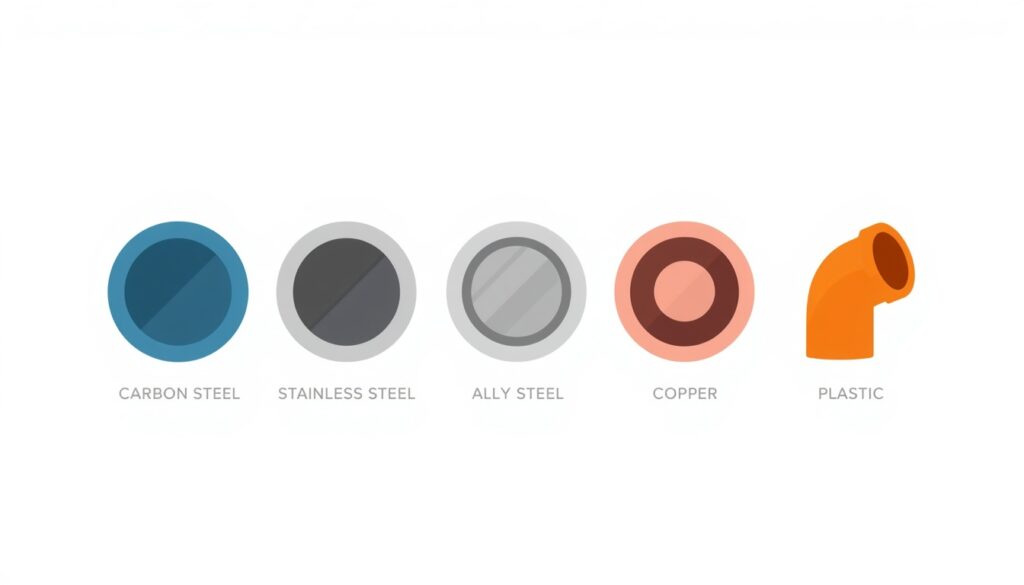
    Material Typical Use Key Characteristics
    Carbon steel Steam, water, oil, gas Strong, economical, but corrodes
    Stainless steel Corrosive fluids, high temperature Corrosion-resistant, expensive
    Alloy steel High-temperature, high-pressure service Retains strength at high temperature
    Copper Instrument air, potable water Corrosion-resistant, but limited temperature range
    Plastic (PVC, CPVC, HDPE) Water, chemicals Corrosion-resistant, limited temperature and pressure
    Fiberglass reinforced plastic (FRP) Corrosive chemicals Corrosion-resistant, lightweight

    Material selection depends on:

    • Fluid composition: Corrosive, abrasive, or reactive fluids require special materials.
    • Temperature: High temperature reduces material strength and increases corrosion rates.
    • Pressure: High pressure requires thicker walls and stronger materials.
    • Environment: External corrosion from salt air, chemicals, or soil must be considered.
    • Cost: Material cost and life-cycle cost both matter.

    Pipe Sizing

    Pipe size affects pressure drop, flow velocity, and cost. Pipes that are too small cause excessive pressure drop; pipes that are too large waste material and space.

    Key sizing considerations:

    • Flow rate: The required flow rate, together with the allowable velocity and pressure drop, determines the pipe size.
    • Velocity: Velocity must be high enough to prevent settling but low enough to avoid erosion and noise.
    • Pressure drop: Pressure drop must be within acceptable limits for the system.
    • Future capacity: Consider whether future flow increases are likely.

    Typical velocity guidelines:

    Fluid Recommended Velocity
    Water (pump discharge) 2–4 m/s
    Water (suction) 0.5–1.5 m/s
    Steam (saturated) 20–40 m/s
    Compressed air 10–20 m/s
    Viscous fluids 0.5–2 m/s

    These are general guidelines. Specific limits depend on the fluid, material, and application.

    Piping Layout

    Layout determines how piping is routed through the plant. Good layout minimizes length, avoids conflicts, and allows access for maintenance.

    Key layout considerations:

    • Route directly: Shorter routes reduce pressure drop and material cost.
    • Avoid unnecessary bends: Every bend adds pressure drop and cost.
    • Allow for expansion: Piping expands and contracts with temperature changes. Loops, offsets, and expansion joints accommodate this movement.
    • Provide access: Valves, instruments, and flanges must be accessible for operation and maintenance.
    • Avoid interference: Piping must not interfere with equipment access, walkways, or other systems.
    • Slope for drainage: Piping that carries liquids should slope to drain points.
    • Consider pipe racks: Grouping pipes in racks saves space and simplifies support.

    Expansion joints. Expansion joints (bellows, slip, or articulated) accommodate thermal movement where loops are not practical. However, they require careful design and maintenance because they are a common source of leaks. They must also be properly anchored and guided so that pressure thrust does not overload the joint or the connected equipment.

    Pipe Supports

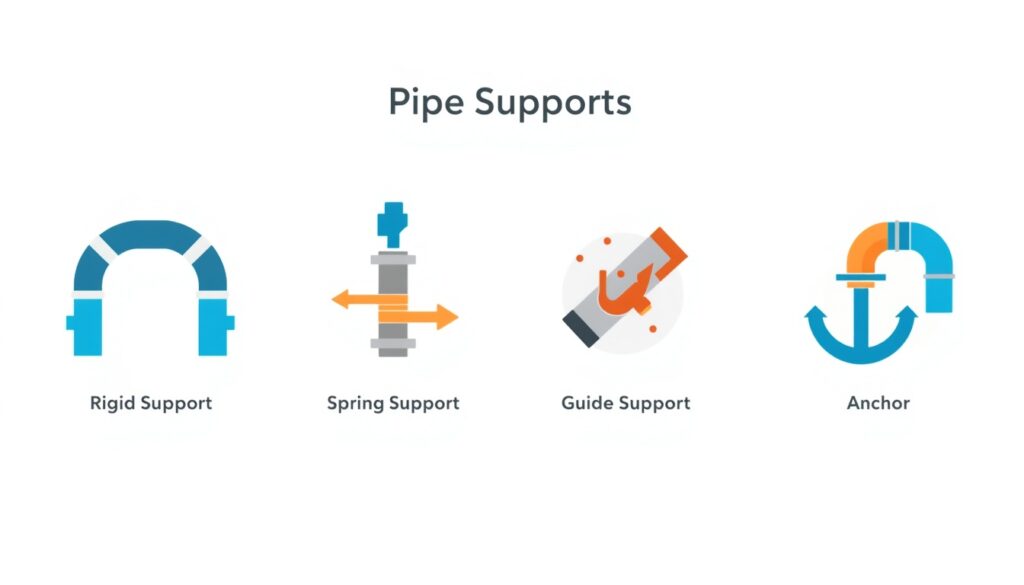
    Types of pipe supports for industrial piping systems

    Pipe supports carry the weight of piping and control movement due to thermal expansion, vibration, and other forces.

    Types of supports:

    • Rigid supports: Carry the weight of the pipe and restrict vertical movement, typically allowing horizontal sliding.
    • Spring supports: Allow vertical movement while supporting weight.
    • Guide supports: Allow axial movement while preventing lateral movement.
    • Anchors: Prevent all movement at a specific point.
    • Snubbers: Allow slow movement but resist rapid movement (e.g., during earthquakes).

    Support spacing depends on pipe size, material, and contents. Supports must be designed to handle the weight of the pipe, insulation, contents, and any valves or fittings.

    Valves and Fittings

    Valves control flow and allow isolation. Fittings connect pipes and change direction.

    Common valve types:

    Valve Type Function Typical Use
    Gate valve On/off isolation Fully open or closed service
    Globe valve Throttling Flow regulation
    Ball valve On/off isolation Quick operation
    Butterfly valve On/off or throttling Large diameter, low pressure
    Check valve Prevent backflow Pump discharge, critical lines
    Control valve Modulate flow Process control
    Relief valve Protect against overpressure Pressure vessels, piping systems

    Common fitting types:

    • Elbows: Change direction.
    • Tees: Branch flow.
    • Reducers: Change pipe size.
    • Flanges: Connect pipes and equipment for disassembly.

    Insulation and Heat Tracing

    Insulation reduces heat loss or gain and protects personnel from hot or cold surfaces.

    Insulation considerations:

    • Thermal performance: Insulation thickness depends on temperature and desired performance.
    • Personnel protection: Surfaces above 60°C or below 0°C typically require insulation or guarding.
    • Corrosion under insulation (CUI): Insulation can trap moisture and cause corrosion. Proper design and maintenance are essential.
    • Heat tracing: Electric or steam tracing maintains temperature in pipes that would otherwise cool below required levels.

    Pipe Identification and Labeling

    In complex plants, pipes must be identifiable for operation and maintenance. Pipes should be labeled with their contents and flow direction. Color coding and labeling systems help operators and maintenance staff identify lines quickly.

    Pressure Relief and Safety

    Piping systems must be protected against overpressure. Relief valves, rupture discs, and venting systems prevent catastrophic failure.

    Key considerations:

    • Relief valve sizing: Must be sized to handle the maximum relief case.
    • Discharge location: Relief discharge must be routed to a safe location.
    • Testing: Relief valves must be tested periodically.
    • Documentation: Relief valve sizing, testing, and maintenance must be documented.

    Water Hammer

    Water hammer occurs when fluid flow is suddenly stopped or changed, causing pressure surges that can damage piping and supports. Common causes include fast-closing valves and pump trips. Proper design includes slow-closing valves, air chambers, and surge suppressors.

    Testing and Commissioning

    Piping systems must be tested before operation to verify integrity and safety.

    Common tests:

    • Hydrostatic test: Fills the system with water and pressurizes to test strength and leak tightness.
    • Pneumatic test: Uses air or inert gas instead of water (used when water is not suitable). Because compressed gas stores much more energy than water, pneumatic tests require additional safety precautions.
    • Flushing: Removes debris and contaminants from the system.
    • Cleaning: Removes scale, rust, and other deposits.
    • Leak test: Verifies that joints and connections do not leak.

    Testing must be documented and witnessed where required.

    Key Design Considerations

    1. Codes and Standards

    Piping systems must comply with applicable codes and standards, such as ASME B31.1 (power piping), ASME B31.3 (process piping), or local equivalents.

    2. Material Compatibility

    Materials must be compatible with the fluid, temperature, and environment. Incompatible materials cause corrosion, contamination, or failure.

    3. Flexibility and Stress Analysis

    Piping must accommodate thermal expansion and other movements without excessive stress. Stress analysis may be required for critical lines. It is typically performed using specialized software such as CAESAR II or AutoPIPE. These tools model the piping system, apply thermal and mechanical loads, and calculate stresses at critical points.

    4. Support and Restraint

    Supports must carry weight and control movement. Restraints must prevent excessive movement without over-stressing the pipe.

    5. Accessibility

    Valves, instruments, and flanges must be accessible for operation and maintenance. Piping should not block access to equipment.

    6. Future Expansion

    Piping systems should be designed with spare capacity for future additions. This includes spare nozzles, spare pipe racks, and spare valves.

    Common Mistakes in Piping Design

    Even experienced designers make mistakes. Common ones include:

    • Undersizing pipes: Causing excessive pressure drop and poor performance.
    • Ignoring thermal expansion: Leading to stress, deformation, or failure.
    • Inadequate support spacing: Causing sagging, vibration, or failure.
    • Poor access to valves and instruments: Making maintenance difficult.
    • Incompatible materials: Causing corrosion or contamination.
    • Missing relief protection: Creating a safety hazard.
    • Ignoring water hammer: Allowing pressure surges to damage piping and supports.
    • Insufficient documentation: Making maintenance and troubleshooting difficult.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Piping Design

    Japanese engineering firms are known for their disciplined approach to piping design. Common characteristics include:

    • Thorough stress analysis: Critical lines are analyzed carefully for thermal and mechanical stress.
    • Conservative material selection: Materials are selected with adequate margin for corrosion and temperature.
    • Detailed support design: Supports are designed for all expected loads and movements.
    • Comprehensive documentation: Piping drawings, isometrics, and test records are carefully maintained.
    • Long-term reliability focus: Designs prioritize reliability and maintainability over lowest initial cost.

    For plant owners, this often means a piping system that performs reliably for decades, with fewer leaks and less maintenance.

    How to Evaluate Piping Design

    When reviewing piping design, ask:

    Question Why It Matters
    Are pipes sized for actual flow and pressure drop? Ensures proper performance
    Are materials compatible with the fluid and environment? Prevents corrosion and failure
    Is thermal expansion accommodated? Prevents stress and deformation
    Are supports designed for all loads? Prevents sagging and vibration
    Are valves and instruments accessible? Enables operation and maintenance
    Has water hammer been assessed and controlled? Prevents pressure-surge damage
    Is relief protection provided? Prevents overpressure failure
    Does the design comply with applicable codes? Ensures safety and legal operation

    A design that addresses these questions is likely to perform well over the plant’s life.

    Conclusion

    Piping systems are essential to plant reliability, safety, and efficiency. For small to medium-scale industrial plants, piping design deserves careful attention from the earliest stages of design. By focusing on material selection, sizing, layout, support, stress analysis, surge protection, and testing, owners and designers can ensure reliable flow and safe operation for decades.

    Key Takeaways

    • Piping systems transport, contain, isolate, control, and protect
    • Material selection depends on fluid, temperature, pressure, and environment
    • Pipe sizing balances pressure drop, velocity, and cost
    • Layout should minimize length, avoid bends, and allow for expansion
    • Supports carry weight and control movement
    • Testing verifies integrity before operation
    • Japanese EPC firms emphasize thorough stress analysis and detailed support design
  • Instrumentation and Control Systems for Industrial Plants: Key Considerations

    Instrumentation and Control Systems for Industrial Plants: Key Considerations

    Instrumentation and control systems are the eyes, ears, and hands of an industrial plant. They measure process variables, transmit data to control systems, and adjust equipment to maintain safe and efficient operation. Without reliable instrumentation and control, a plant cannot operate consistently, safely, or efficiently.

    For small to medium-scale industrial plants, instrumentation and control design is especially critical because there is less redundancy and fewer resources to manage complexity. The right design ensures reliable measurement, accurate control, and safe operation.

    This article covers the key considerations in instrumentation and control system design for industrial plants, from sensor selection to control system architecture.

    The Role of Instrumentation and Control

    Instrumentation and control systems perform several essential functions:

    • Measurement: Sensors measure temperature, pressure, flow, level, and other process variables.
    • Transmission: Signals are transmitted from field instruments to control systems.
    • Control: Control systems adjust valves, motors, and other actuators to maintain desired conditions.
    • Monitoring: Operators monitor process conditions through displays and alarms.
    • Safety: Safety instrumented systems (SIS) protect the plant during abnormal conditions.
    • Data logging: Historical data supports troubleshooting, optimization, and compliance.

    Without reliable instrumentation and control, operators cannot know what is happening in the process, and equipment cannot respond to changing conditions.

    Key Instrumentation Types

    Different process variables require different types of instruments.

    Variable Common Instrument Types
    Temperature Thermocouples, RTDs, thermistors
    Pressure Pressure gauges, transmitters, switches
    Flow Orifice plates, vortex meters, Coriolis meters, ultrasonic meters
    Level Float switches, radar, ultrasonic, differential pressure
    Analytical pH, conductivity, oxygen, gas analyzers
    Position Limit switches, encoders, proximity sensors

    Each instrument type has advantages and limitations. Selection depends on accuracy requirements, process conditions, and cost.

    Instrument Selection Considerations

    Choosing the right instrument is critical for reliable measurement.

    1. Accuracy and Range
    Instruments must be accurate enough for the application and cover the expected range of process conditions. Over-specifying accuracy adds cost; under-specifying leads to poor control.

    2. Process Conditions
    Temperature, pressure, corrosion, vibration, and humidity all affect instrument performance. Instruments must be rated for the conditions they will experience.

    3. Response Time
    Some processes require fast-responding instruments; others do not. Response time affects control loop performance.

    4. Installation, Calibration, and Maintenance
    Instruments must be accessible for calibration and maintenance. Installation must comply with manufacturer requirements and applicable standards. Instruments must be calibrated periodically to maintain accuracy. Calibration intervals depend on the instrument type, process conditions, and criticality of the measurement.

    5. Signal Type
    Instruments can transmit analog signals (4–20 mA), hybrid signals such as HART, or fully digital fieldbus communications. The choice affects wiring, control system compatibility, and diagnostic capability. Fieldbus and digital communications protocols (such as HART, Profibus, or Foundation Fieldbus) allow instruments to transmit diagnostic data in addition to process measurements. This enables predictive maintenance and faster troubleshooting.

    6. Certification
    In hazardous areas, instruments must be certified for the applicable area classification (e.g., ATEX, IECEx, or NEC/CEC).

    Control System Types

    The control system receives signals from instruments and sends commands to actuators.

    Type Characteristics Typical Use
    Relay logic Simple, hardwired Small plants, simple processes
    PLC Programmable, flexible, widely supported Most industrial plants
    DCS Distributed, integrated, scalable Large, complex plants
    SCADA Supervisory layer for data acquisition, monitoring, and remote access across PLCs or RTUs Plants requiring remote or centralized monitoring

    For small to medium-scale plants, PLC-based control is common. It offers flexibility, is well-supported by vendors, and can be expanded as the plant grows.

    Control Loop Design

    A control loop consists of a sensor, a controller, and a final control element (such as a valve or motor). The controller compares the measured value to a setpoint and adjusts the final control element to reduce the difference.

    Key control loop considerations:

    • Loop tuning: Controllers must be tuned for stable, responsive control.
    • Loop interaction: Multiple control loops can interact, requiring careful design.
    • Redundancy: Critical loops may require redundant sensors or controllers.
    • Fail-safe positions: Valves and actuators should fail to a safe position on loss of signal or power.

    Safety Instrumented Systems (SIS)

    Safety instrumented systems are independent of the basic process control system and are designed to bring the plant to a safe state during abnormal conditions.

    Key SIS considerations:

    • Safety integrity level (SIL): Determines the required reliability of the SIS.
    • Independence: SIS must be independent of the basic control system.
    • Testing: SIS components must be tested periodically to verify functionality.
    • Documentation: SIS design, testing, and maintenance must be documented.

    Whether a formal SIL-rated SIS is required depends on a hazard and risk assessment, not on plant size alone. For small plants, a full SIS may not be required, but safety interlocks and shutdown systems are still essential.

    Human-Machine Interface (HMI)

    The HMI is how operators interact with the control system. A well-designed HMI improves situational awareness and reduces operator error.

    Key HMI considerations:

    • Clarity: Displays should be clear and uncluttered.
    • Consistency: Similar information should be presented in similar ways.
    • Alarm management: Alarms should be prioritized and actionable.
    • Trending: Historical trends help operators understand process behavior.
    • Accessibility: Displays should be readable from normal operating positions.

    Alarm rationalization is the process of reviewing and prioritizing alarms to ensure they are actionable and meaningful. Too many alarms can overwhelm operators and lead to critical alarms being missed.

    Integration with Other Plant Systems

    Control systems often integrate with other plant systems, including electrical systems, safety systems, and business networks. Integration requires careful planning to avoid conflicts and security risks.

    Cybersecurity for Control Systems

    Control systems are increasingly connected to networks, creating cybersecurity risks. A cyberattack on a control system could disrupt operations or cause safety incidents.

    Key cybersecurity considerations:

    • Network segmentation: Control networks should be separated from business networks.
    • Access control: Only authorized personnel should access control systems.
    • Monitoring: Network traffic and system logs should be monitored for unusual activity.
    • Updates: Control system software and firmware should be kept up to date.
    • Training: Personnel should be trained on cybersecurity awareness.

    Key Design Considerations

    1. Reliability
    Instruments and control systems must be reliable. Critical measurements may require redundant instruments or controllers.

    2. Maintainability
    Instruments must be accessible for calibration, testing, and replacement. Documentation must be clear and complete.

    3. Scalability
    Control systems should be designed with spare capacity for future expansion. This includes spare I/O, spare network capacity, and spare panel space.

    4. Standardization
    Standardizing on common instrument types and control system platforms reduces training, spare parts, and maintenance complexity.

    5. Environmental Conditions
    Instruments and control equipment must be rated for the environmental conditions they will experience, including temperature, humidity, vibration, and corrosion.

    6. Regulatory Compliance
    Instrumentation and control systems must comply with applicable codes and standards, including those for hazardous areas, safety systems, and environmental monitoring.

    Common Mistakes in Instrumentation and Control Design

    Even experienced designers make mistakes. Common ones include:

    • Underspecifying instruments: Leading to poor accuracy or premature failure.
    • Ignoring process conditions: Instruments that cannot handle actual temperature, pressure, or corrosion.
    • Inadequate redundancy: Critical measurements without backup.
    • Poor HMI design: Confusing displays that increase operator error.
    • Neglecting cybersecurity: Control systems exposed to network threats.
    • Insufficient documentation: Making maintenance and troubleshooting difficult.
    • No spare capacity: Requiring costly upgrades for future expansion.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Instrumentation and Control

    Japanese engineering firms are known for their disciplined approach to instrumentation and control design. Common characteristics include:

    • Thorough specification: Instruments are specified carefully, with attention to accuracy, range, and process conditions.
    • Conservative design margins: Redundancy and spare capacity are provided where justified.
    • Detailed documentation: Loop diagrams, instrument schedules, and test records are carefully maintained.
    • Comprehensive testing: Control loops and safety systems are tested thoroughly before startup.
    • Long-term reliability focus: Designs prioritize reliability and maintainability over lowest initial cost.

    For plant owners, this often means an instrumentation and control system with a long service life and fewer unplanned outages.

    How to Evaluate Instrumentation and Control Design

    When reviewing instrumentation and control design, ask:

    Question Why It Matters
    Are instruments specified for actual process conditions? Ensures reliable measurement
    Is redundancy provided for critical measurements? Ensures continued operation during faults
    Is the control system scalable? Avoids costly upgrades later
    Is the HMI designed for operator effectiveness? Reduces operator error
    Is cybersecurity addressed? Protects against network threats
    Is documentation complete? Supports maintenance and troubleshooting
    Does the design comply with applicable codes? Ensures safety and legal operation

    A design that addresses these questions is likely to perform well over the plant’s life.

    Conclusion

    Instrumentation and control systems are essential to plant reliability, safety, and efficiency. For small to medium-scale industrial plants, instrumentation and control design deserves careful attention from the earliest stages of design. By focusing on instrument selection, control system architecture, safety systems, and cybersecurity, owners and designers can ensure reliable measurement, accurate control, and safe operation for many years.

    Key Takeaways

    • Instrumentation and control systems measure, transmit, control, monitor, and protect
    • Instrument selection depends on accuracy, process conditions, and response time
    • Control system types include relay logic, PLC, DCS, and SCADA
    • Safety instrumented systems (SIS) protect the plant during abnormal conditions
    • HMI design and alarm management affect operator effectiveness
    • Cybersecurity is an increasing concern for control systems
    • Japanese EPC firms emphasize thorough specification and comprehensive testing
  • Electrical Systems for Industrial Plants: Key Design Considerations

    Electrical Systems for Industrial Plants: Key Design Considerations

    Electrical systems are the nervous system of an industrial plant. They power motors, control instruments, provide lighting, and ensure safety systems function when needed. Unlike mechanical systems, which can sometimes be bypassed or operated manually, electrical systems must operate correctly every time. A failure can shut down the entire plant—or worse, create a safety hazard.

    For small to medium-scale industrial plants, electrical system design is especially critical because there is less redundancy and fewer resources to manage complexity. The right design ensures reliable power, safe operation, and room for future expansion.

    This article covers the key considerations in electrical system design for industrial plants, from power supply to distribution, protection, and control.

    The Main Electrical Systems in an Industrial Plant

    Main electrical systems in an industrial plant diagram

    An industrial plant’s electrical system can be divided into several subsystems, each with its own function.

    System Purpose
    Power supply Receives power from the grid or on-site generation
    Power distribution Delivers power to equipment throughout the plant
    Motor control Starts, stops, and protects motors
    Instrumentation and control Monitors and controls process variables
    Lighting Provides illumination for operation, maintenance, and safety
    Emergency power Provides backup power for critical systems
    Grounding and lightning protection Protects people and equipment from electrical hazards

    Each subsystem must be designed to work with the others. A weakness in any one can compromise the entire plant.

    Power Supply

    The first decision in electrical system design is how the plant will receive power.

    Grid supply: Most industrial plants receive power from the local utility grid. The supply voltage depends on the utility and the plant’s size. Small plants may receive power at low voltage (e.g., 400 V or 480 V), while larger plants receive power at medium voltage (e.g., 6.6 kV, 11 kV, or 33 kV) and step it down on site.

    On-site generation: Some plants generate their own power using gas turbines, diesel generators, or renewable sources. This provides independence from the grid but adds complexity and cost.

    Combined supply: Many plants use both grid supply and on-site generation. This provides redundancy and allows the plant to operate during grid outages.

    Key considerations for power supply:

    • Reliability: How often does the grid fail, and how long do outages last?
    • Power quality: Voltage sags, harmonics, and frequency variations can affect equipment.
    • Cost: Tariff structures, demand charges, and time-of-use rates affect operating cost.
    • Future expansion: Will the plant need more power later?

    Power Distribution

    Once power enters the plant, it must be distributed to equipment throughout the site.

    Distribution voltages: Plants typically use multiple voltage levels:

    • Medium voltage (e.g., 6.6 kV, 11 kV, 33 kV): For distribution across the site and to large motors.
    • Low voltage (e.g., 400 V, 480 V): For small motors, lighting, and control systems.
    • Extra-low voltage (e.g., 24 V DC): For instrumentation and control.

    Transformers step voltage down between levels.

    Distribution configurations:

    Configuration Characteristics Typical Use
    Radial Simple, single path from source to load Small plants, non-critical loads
    Ring Power feeds from two directions Medium plants, improved reliability
    Network Multiple sources and paths Large plants, high reliability

    For small to medium-scale plants, radial distribution is often sufficient. Ring distribution may be justified for critical loads.

    Key considerations for power distribution:

    • Voltage drop: Long cable runs cause voltage drop, which affects motor performance.
    • Cable sizing: Cables must be sized for current, voltage drop, and short-circuit withstand.
    • Routing: Cables should be routed away from hot surfaces, moisture, and mechanical damage.
    • Segregation: Power and instrument cables should be segregated to avoid interference.

    Power factor correction: Many utilities charge penalties for low power factor. Power factor correction capacitors or synchronous condensers may be required to maintain power factor above a specified threshold.

    Harmonics and filtering: Non-linear loads such as VFDs and rectifiers generate harmonics that can distort voltage and affect sensitive equipment. Harmonic filters or active compensators may be required.

    Motor Control

    Comparison of motor starting methods for industrial plants

    Motors are the largest electrical loads in most industrial plants. They drive pumps, fans, compressors, and conveyors.

    Motor starting: Large motors draw high starting current, which can cause voltage dips. Starting methods include:

    • Direct-on-line (DOL): Simple but high starting current.
    • Star-delta: Reduces starting current but adds complexity.
    • Soft starter: Gradually increases voltage to reduce starting current.
    • Variable frequency drive (VFD): Controls motor speed and torque, with low starting current.

    Motor protection: Motors must be protected against:

    • Overload: Excessive current due to mechanical or electrical faults.
    • Short circuit: Faults that cause very high current.
    • Phase loss: Loss of one phase in a three-phase supply.
    • Earth fault: Current leaking to ground.

    Protection devices include overload relays, circuit breakers, and earth fault relays.

    Key considerations for motor control:

    • Starting method: Depends on motor size, load characteristics, and grid strength.
    • Protection coordination: Protection devices must coordinate to isolate faults without unnecessary trips.
    • Control philosophy: Local vs. remote control, manual vs. automatic operation.

    Instrumentation and Control

    Instrumentation and control systems monitor process variables and adjust equipment to maintain desired conditions.

    Control system types:

    Type Characteristics Typical Use
    Relay logic Simple, hardwired Small plants, simple processes
    PLC Programmable, flexible Most industrial plants
    DCS Distributed, integrated Large, complex plants
    SCADA Supervisory control and data acquisition Plants requiring remote monitoring

    For small to medium-scale plants, PLC-based control is common. It offers flexibility and is well-supported by vendors.

    Key considerations for instrumentation and control:

    • Signal types: Analog (4–20 mA), digital, and fieldbus communications.
    • Redundancy: Critical control loops may require redundant sensors or controllers.
    • Cybersecurity: Control systems are increasingly connected to networks, creating security risks.
    • Human-machine interface (HMI): Operators need clear, intuitive displays.

    Lighting

    Lighting is often overlooked but essential for safe operation and maintenance.

    Lighting types:

    • General lighting: Illuminates work areas.
    • Task lighting: Provides focused light for specific tasks.
    • Emergency lighting: Provides illumination during power failures.
    • Outdoor lighting: Illuminates access roads, storage areas, and perimeters.

    Key considerations for lighting:

    • Illumination levels: Depends on the task and area.
    • Energy efficiency: LED lighting reduces power consumption.
    • Emergency lighting: Must be powered by backup supply.
    • Maintenance access: Light fixtures must be accessible for replacement.

    Emergency Power

    Emergency power systems provide backup power for critical loads during grid outages.

    Emergency power sources:

    • Diesel generators: Common, reliable, but require fuel storage and maintenance.
    • Battery systems: Provide instant power for short outages.
    • Uninterruptible power supplies (UPS): Provide clean, continuous power for sensitive equipment.

    Critical loads requiring emergency power:

    • Safety systems (fire detection, emergency shutdown)
    • Control systems
    • Emergency lighting
    • Critical instrumentation
    • Communication systems

    Key considerations for emergency power:

    • Load list: Which loads require backup power?
    • Duration: How long must backup power last?
    • Startup time: How quickly must backup power come online?
    • Testing: Emergency systems must be tested regularly.

    Grounding and Lightning Protection

    Grounding and lightning protection protect people and equipment from electrical hazards.

    Grounding: Grounding provides a low-resistance path for fault current, allowing protection devices to operate quickly. It also stabilizes voltage and reduces electrical noise.

    Lightning protection: Lightning protection systems intercept lightning strikes and conduct them safely to ground. They include air terminals, down conductors, and grounding electrodes.

    Key considerations:

    • Grounding system design: Must be designed for the site’s soil conditions.
    • Bonding: All metallic structures and equipment must be bonded to the grounding system.
    • Testing: Grounding systems must be tested periodically.

    Arc flash safety: Arc flash studies identify areas where high-energy electrical faults could occur. Appropriate labeling, PPE requirements, and work procedures must be in place.

    Key Design Considerations

    1. Load Analysis
    The first step in electrical design is a load analysis. This determines the total connected load, demand load, and future load.

    2. Redundancy
    Critical systems may require redundant power supplies, transformers, or feeders. The level of redundancy depends on the consequences of failure.

    3. Protection Coordination
    Protection devices must coordinate so that the device closest to a fault operates first, minimizing disruption.

    4. Cable Routing and Segregation
    Power and instrument cables should be routed separately to avoid interference. Cables should be protected from heat, moisture, and mechanical damage.

    5. Safety
    Electrical systems must comply with applicable codes and standards (e.g., IEC, NEC, local regulations). Safety features include grounding, isolation, and lockout/tagout provisions.

    6. Future Expansion
    Electrical systems should be designed with spare capacity for future loads. This includes spare breakers, spare cable trays, and spare transformer capacity.

    7. Electrical System Studies
    Electrical system studies include load flow analysis, short circuit analysis, protection coordination, and arc flash analysis. These studies should be completed during design and updated as the system changes.

    Common Mistakes in Electrical System Design

    Even experienced designers make mistakes. Common ones include:

    • Undersizing equipment: Leading to overloads and failures.
    • Ignoring voltage drop: Causing poor motor performance.
    • Poor protection coordination: Leading to unnecessary trips or failure to isolate faults.
    • Inadequate grounding: Creating safety hazards and equipment damage.
    • No spare capacity: Requiring costly upgrades for future expansion.
    • Insufficient segregation: Causing electrical noise and interference.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Electrical System Design

    Japanese engineering firms are known for their disciplined approach to electrical system design. Common characteristics include:

    • Thorough load analysis: Loads are analyzed carefully, with margin for future growth.
    • Conservative design margins: Equipment is sized with adequate margin for worst-case conditions.
    • Detailed protection coordination: Protection settings are carefully studied and coordinated.
    • Comprehensive documentation: Drawings, schedules, and test records are carefully maintained.
    • Long-term reliability focus: Designs prioritize reliability and maintainability over lowest initial cost.

    For plant owners, this often means an electrical system that performs reliably for decades, with fewer unplanned outages.

    How to Evaluate Electrical System Design

    When reviewing electrical system design, ask:

    Question Why It Matters
    What is the total connected load and demand load? Determines equipment sizing
    What is the power supply configuration? Affects reliability and cost
    Is redundancy provided for critical loads? Ensures continued operation during faults
    How is protection coordinated? Minimizes disruption from faults
    How are cables routed and segregated? Avoids interference and damage
    Is there spare capacity for future expansion? Avoids costly upgrades later
    Does the design comply with applicable codes? Ensures safety and legal operation

    A design that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Electrical systems are critical to plant reliability, safety, and efficiency
    • Power supply can be from the grid, on-site generation, or both
    • Distribution configurations include radial, ring, and network
    • Motor starting methods include DOL, star-delta, soft starter, and VFD
    • Emergency power is required for safety, control, and critical instrumentation
    • Japanese EPC firms emphasize thorough load analysis and protection coordination

    Conclusion

    Electrical systems are critical to plant reliability, safety, and efficiency. For small to medium-scale industrial plants, electrical design deserves careful attention from the earliest stages of design. By focusing on load analysis, redundancy, protection, safety, and future expansion, owners and designers can ensure reliable power and safe operation for decades.

  • Water Treatment for Industrial Plants: Key Considerations

    Water Treatment for Industrial Plants: Key Considerations

    Water is essential to almost every industrial plant. It is used for cooling, steam generation, process operations, and equipment cleaning. But water is rarely pure. It contains dissolved minerals, suspended solids, dissolved gases, and microorganisms that can cause corrosion, scaling, fouling, and biological growth.

    Water treatment is the process of removing or controlling these impurities so that water can be used safely and reliably in plant systems. For small to medium-scale industrial plants, water treatment is especially critical because there is less redundancy and less margin for error. A poorly treated cooling system can lead to tube failures, reduced output, and costly downtime.

    This article covers the fundamentals of water treatment for industrial plants, the key treatment processes, and the considerations that plant owners should be aware of.

    Why Water Treatment Matters

    Water quality affects plant reliability, efficiency, and cost. Poor water quality can lead to:

    • Corrosion: Dissolved oxygen, low pH, and dissolved solids attack metal surfaces.
    • Scaling: Dissolved minerals precipitate and form deposits on heat transfer surfaces.
    • Fouling: Suspended solids and biological growth block flow and reduce heat transfer.
    • Foaming and carryover: Impurities in boiler water cause foaming, leading to carryover into steam and turbine deposits.
    • Microbiological growth: Bacteria, algae, and fungi form biofilms that reduce heat transfer and promote corrosion.

    These problems reduce plant efficiency, increase maintenance cost, and shorten equipment life. In severe cases, they cause forced outages.

    The Main Water Systems in an Industrial Plant

    Main water systems in an industrial plant diagram

    Main water systems in an industrial plant diagram

    Different plant systems have different water quality requirements.

    System Purpose Key Water Quality Concerns
    Cooling water Reject heat from condensers and auxiliary equipment Scaling, corrosion, biological growth
    Boiler feedwater Produce steam in boilers Scale, corrosion, carryover
    Demineralized water Feed high-pressure boilers and process systems Dissolved solids, silica, conductivity
    Process water Used in chemical or manufacturing processes Varies by process
    Potable water For human consumption and sanitation Microbial, chemical, and aesthetic standards

    Each system requires a different level of treatment. Cooling water typically needs less treatment than boiler feedwater, which must be nearly pure. Process water treatment depends on the specific process. Some processes require demineralized water, while others can tolerate lower quality.

    Key Water Quality Parameters

    Water treatment is designed to control specific parameters. These include:

    • Hardness: Calcium and magnesium ions that cause scaling.
    • Alkalinity: Bicarbonate and carbonate ions that affect pH and scaling potential.
    • pH: Acidity or alkalinity of the water.
    • Conductivity: Measure of dissolved solids.
    • Silica: Forms hard deposits on boiler and turbine surfaces.
    • Dissolved oxygen: Causes corrosion in boilers and cooling systems.
    • Iron and copper: Corrosion products that deposit on surfaces.
    • Chlorides: Cause pitting corrosion in stainless steels.
    • Suspended solids: Cause fouling and deposits.
    • Microorganisms: Cause biofilms and microbiologically influenced corrosion.

    Cooling Water Treatment

    Cooling water treatment challenges including scaling, corrosion, and biological growth

    Cooling water treatment challenges including scaling, corrosion, and biological growth

    Cooling water treatment focuses on three main problems: scaling, corrosion, and biological growth. Treatment requirements also depend heavily on the type of cooling system used.

    Scaling control:

    Scale forms when dissolved minerals precipitate on heat transfer surfaces. The most common scale is calcium carbonate, but calcium sulfate, silica, and other deposits also occur.

    Control methods include:

    • Chemical inhibitors: Phosphonates, polymers, and other chemicals that prevent crystal formation.
    • pH control: Adjusting pH to keep minerals soluble.
    • Blowdown: Removing a portion of recirculating water to control dissolved solids concentration.
    • Softening: Removing hardness ions before they enter the system.

    Corrosion control:

    Corrosion in cooling systems is caused by dissolved oxygen, low pH, chlorides, and microbiological activity.

    Control methods include:

    • Corrosion inhibitors: Chemicals that form protective films on metal surfaces.
    • pH control: Maintaining pH in a range that minimizes corrosion.
    • Material selection: Using corrosion-resistant materials where needed.
    • Cathodic protection: For critical components.

    Biological control:

    Bacteria, algae, and fungi grow in cooling systems, especially in warm water with nutrients.

    Control methods include:

    • Biocides: Oxidizing (chlorine, bromine) or non-oxidizing chemicals that kill microorganisms.
    • Dispersants: Chemicals that break up biofilms.
    • Physical cleaning: Periodic flushing or mechanical cleaning.

    Once-through cooling systems:

    Once-through cooling systems require less chemical treatment than closed-loop systems because water is not recirculated. However, intake screening, chlorination, and corrosion control may still be required.

    Air-cooled systems:

    Plants using air-cooled cooling systems eliminate cooling water treatment, but boiler water treatment and demineralized water production may still be required.

    Boiler Water Treatment

    Boiler water treatment is more demanding than cooling water treatment because boilers operate at high temperature and pressure.

    External treatment:

    External treatment removes impurities before water enters the boiler. Common processes include:

    • Clarification: Removing suspended solids.
    • Filtration: Removing fine particles.
    • Softening: Removing hardness ions.
    • Demineralization: Removing all dissolved solids using ion exchange.
    • Reverse osmosis: Removing dissolved solids using membrane filtration.

    Internal treatment:

    Internal treatment controls residual impurities inside the boiler. Common chemicals include:

    • Oxygen scavengers: Remove dissolved oxygen.
    • pH adjusters: Maintain alkaline pH to minimize corrosion.
    • Scale inhibitors: Prevent precipitation on boiler surfaces.
    • Anti-foaming agents: Prevent foaming and carryover.

    Blowdown:

    Blowdown removes a portion of boiler water to control dissolved solids concentration. Continuous blowdown is preferred for larger boilers; intermittent blowdown is used for smaller ones.

    Demineralized Water Production

    High-pressure boilers and some process systems require demineralized water, which is water with almost all dissolved solids removed.

    Common demineralization processes include:

    • Ion exchange: Uses resins to exchange dissolved ions for hydrogen and hydroxide ions.
    • Reverse osmosis: Uses pressure to force water through a semi-permeable membrane, leaving dissolved solids behind.
    • Electrodeionization (EDI): Combines ion exchange and membrane processes for continuous demineralization.

    Demineralized water is essential for high-pressure boilers because dissolved solids can deposit on turbine blades, causing imbalance and efficiency loss.

    Key Design Considerations

    1. Water Source and Quality — The first step in water treatment design is understanding the water source. Surface water, groundwater, seawater, and municipal water all have different characteristics and require different treatment.
    2. Treatment Goals — Treatment goals depend on the end use. Cooling water, boiler feedwater, and demineralized water each have different quality requirements.
    3. Chemical Storage and Handling — Water treatment chemicals must be stored and handled safely. This requires appropriate containment, ventilation, and personal protective equipment. Personnel handling water treatment chemicals must be trained in safe handling, emergency response, and proper use of personal protective equipment.
    4. Waste Streams — Water treatment produces waste streams, including blowdown, filter backwash, and regeneration waste. These must be managed in compliance with environmental regulations.
    5. Monitoring and Control — Water quality must be monitored continuously. Key parameters include pH, conductivity, hardness, silica, and dissolved oxygen. Automated control systems help maintain treatment within specified limits.
    6. Redundancy — Critical water treatment components (pumps, resin beds, membrane units) may require redundancy to ensure continuous operation.

    Common Mistakes in Water Treatment

    Even experienced designers make mistakes. Common ones include:

    • Undersizing treatment systems: Leading to inadequate water quality and equipment damage.
    • Ignoring water source variability: Water quality changes seasonally and over time.
    • Insufficient chemical storage: Running out of treatment chemicals causes system upsets.
    • Poor waste management: Leading to environmental violations.
    • Inadequate monitoring: Failing to detect water quality excursions before damage occurs.
    • Skipping redundancy: A single point of failure can shut down the plant.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Water Treatment

    Japanese engineering firms are known for their disciplined approach to water treatment design. Common characteristics include:

    • Thorough water source assessment: Water quality is analyzed over time to capture variability.
    • Conservative design margins: Treatment systems are sized with adequate margin for worst-case water quality.
    • Detailed chemical management: Chemical selection, storage, and handling are carefully planned.
    • Comprehensive monitoring: Water quality is tracked continuously with clear alarm and response procedures.
    • Long-term performance focus: Treatment system performance is monitored and optimized over the plant’s life.

    For plant owners, this often means a water treatment system that performs reliably for decades, even under challenging water conditions.

    How to Evaluate Water Treatment Design

    When reviewing water treatment design, ask:

    Question Why It Matters
    What is the water source and quality? Determines treatment requirements
    What are the treatment goals for each system? Ensures water quality meets end-use requirements
    How is water quality monitored? Detects excursions before damage occurs
    How are chemicals stored and handled? Ensures safety and regulatory compliance
    How are waste streams managed? Ensures environmental compliance
    Is redundancy provided for critical components? Ensures continuous operation
    What is the life-cycle cost? Captures total cost, not just capital

    A water treatment system that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Water treatment controls corrosion, scaling, fouling, and biological growth
    • Different plant systems have different water quality requirements
    • Cooling water treatment focuses on scaling, corrosion, and biological control
    • Boiler water treatment is more demanding and requires external and internal treatment
    • Demineralized water is essential for high-pressure boilers
    • Japanese EPC firms emphasize thorough water source assessment and conservative design margins

    Conclusion

    Water treatment is a critical but often overlooked aspect of industrial plant design. It affects reliability, efficiency, maintenance cost, and environmental compliance. For small to medium-scale industrial plants, where margins are tight, water treatment deserves careful attention from the earliest stages of design.

    By understanding water quality requirements, selecting appropriate treatment processes, and planning for monitoring, redundancy, and waste management, owners and designers can ensure reliable water quality and long-term plant performance.

  • Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling is one of the most overlooked yet consequential decisions in industrial plant design. Every thermal plant—whether it burns coal, gas, biomass, or waste heat—must reject heat to the environment. How that heat is rejected affects efficiency, water consumption, environmental impact, capital cost, and site selection.

    For small to medium-scale industrial plants, cooling system selection is especially critical because there is less margin for error and fewer resources to manage complex systems. The wrong choice can limit plant output, increase operating cost, or create regulatory problems.

    This article covers the main cooling system options, compares them side by side, and helps you decide which one fits your project.

    Why Cooling Matters

    Thermal plants convert heat into electricity, but not all heat can be converted. A significant portion must be rejected to the environment. This is a fundamental thermodynamic limit—no plant can convert all its heat input into useful work.

    The cooling system’s job is to reject this waste heat efficiently and reliably. The main functions are:

    • Condensing steam: In steam cycles, cooling condenses the exhaust steam from the turbine back into water so it can be reused.
    • Cooling auxiliary equipment: Lubricating oil, generators, and other equipment require cooling.
    • Maintaining vacuum: Efficient condensing requires low pressure, which depends on effective cooling.

    If the cooling system underperforms, the turbine back pressure rises, reducing output and efficiency. In severe cases, the plant must reduce load or shut down.

    The Main Cooling System Options

    Comparison of once-through, closed-loop, and air-cooled cooling system types

    Comparison of once-through, closed-loop, and air-cooled cooling system types

    There are three main types of cooling systems for industrial plants:

    1. Once-through cooling
    2. Closed-loop (recirculating) cooling with cooling towers
    3. Air-cooled (dry) cooling

    Each has distinct characteristics, advantages, and drawbacks.

    Once-Through Cooling

    In a once-through system, water is drawn from a nearby source (river, lake, sea), passed through the condenser, and returned to the source at a higher temperature.

    Characteristics:

    • High efficiency: Once-through cooling provides the best cooling performance because water temperature is typically low.
    • Low capital cost: Fewer components, simpler system.
    • High water consumption: Large volumes of water are drawn and returned.
    • Environmental impact: Thermal discharge can affect aquatic ecosystems.
    • Site constraint: Requires a large, reliable water source.

    When it makes sense:

    • Sites with access to abundant cooling water (coastal or large river locations)
    • Regions with lenient thermal discharge regulations
    • Plants where efficiency is the top priority

    Once-through cooling is increasingly restricted in many jurisdictions due to environmental concerns. In the United States, for example, the Clean Water Act Section 316(b) requires that cooling water intake structures minimize environmental impact.

    Closed-Loop Cooling with Cooling Towers

    In a closed-loop system, cooling water is recirculated between the condenser and a cooling tower. The cooling tower rejects heat to the atmosphere, primarily through evaporation.

    Characteristics:

    • Moderate efficiency: Performance depends on ambient wet-bulb temperature. Efficiency is lower than once-through but higher than air-cooled.
    • Moderate capital cost: Cooling towers and circulating water systems add cost.
    • Lower water consumption: Water is lost primarily through evaporation and blowdown, but consumption is much lower than once-through.
    • Visible plume: Cooling towers produce a visible plume of water vapor, which can be a concern in some locations.
    • Chemical treatment: Recirculated water requires treatment to control corrosion, scaling, and biological growth. Closed-loop systems require continuous water treatment to manage these effects; treatment programs typically include corrosion inhibitors, scale inhibitors, and biocides.

    When it makes sense:

    • Sites with limited water availability
    • Regions with strict thermal discharge regulations
    • Plants where a balance between efficiency and water use is needed

    Closed-loop cooling is the most common choice for new industrial plants in many regions. It offers a reasonable compromise between efficiency, water use, and environmental impact.

    Air-Cooled (Dry) Cooling

    In an air-cooled system, heat is rejected directly to the atmosphere using air-cooled condensers or fin-fan coolers. No cooling water is used.

    Characteristics:

    • Lower efficiency: Performance depends on ambient dry-bulb temperature, which is typically higher than wet-bulb temperature. This reduces plant efficiency compared to wet cooling.
    • Higher capital cost: Air-cooled condensers are large and expensive.
    • Zero water consumption: No cooling water is required for heat rejection.
    • Large footprint: Air-cooled systems require significant space.
    • Higher auxiliary power: Fans consume more power than cooling tower fans.

    When it makes sense:

    • Sites with no reliable water source
    • Regions with strict water use restrictions
    • Plants where water availability is uncertain or expensive

    Air-cooled cooling is common in arid regions and in plants where water is scarce or expensive. It eliminates water consumption but at the cost of efficiency and capital cost.

    Side-by-Side Comparison

    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

    Factor Once-Through Closed-Loop (Wet) Air-Cooled (Dry)
    Cooling efficiency Highest Moderate Lowest
    Capital cost Lowest Moderate Highest
    Water consumption Highest Moderate None
    Footprint Small Moderate Large
    Auxiliary power Lowest Moderate Highest
    Environmental impact Thermal discharge Water consumption, plume Land use, noise
    Site requirement Large water source Moderate water source No water source
    Typical use Coastal, large rivers Most inland plants Arid regions

    Hybrid Cooling Systems

    Some plants use hybrid cooling, which combines wet and dry cooling. In a hybrid system, cooling towers operate during cooler periods, while air-cooled condensers take over during peak heat or when water is scarce.

    Advantages:

    • Reduces water consumption compared to pure wet cooling
    • Improves efficiency compared to pure dry cooling
    • Provides flexibility to respond to water availability and ambient conditions

    Disadvantages:

    • Higher capital cost than either pure wet or pure dry
    • More complex operation and maintenance

    Hybrid cooling is often used in regions with seasonal water constraints or where a balance between efficiency and water use is required.

    Key Design Considerations

    1. Ambient Conditions

    Wet-bulb temperature drives wet cooling performance. Dry-bulb temperature drives air-cooled performance. Both vary by location and season. Design must account for the worst-case conditions the plant will face.

    2. Water Availability and Quality

    Water quantity, quality, and cost all affect cooling system selection. Poor water quality may require treatment, which adds cost and complexity.

    3. Environmental Regulations

    Thermal discharge limits, water intake rules, and plume restrictions can all constrain cooling system options. These must be identified early in design.

    4. Plant Size and Load Profile

    Small plants may have different constraints than large ones. A plant that operates only during peak hours may not justify the cost of a complex cooling system.

    5. Parasitic Power

    Cooling system auxiliaries (pumps, fans) consume power, reducing net plant output. This must be accounted for in performance calculations.

    6. Corrosion and Materials

    Cooling water chemistry affects material selection. Once-through systems using seawater require corrosion-resistant materials. Closed-loop systems require water treatment to control scaling and corrosion.

    7. Availability and Redundancy

    For critical plants, consider whether redundancy in cooling system components (pumps, fans, cells) is justified. A single cooling tower cell failure can limit plant output.

    8. Noise Regulations

    Noise from cooling towers and air-cooled condensers can be a constraint in populated areas. Local noise regulations may limit fan speed or require acoustic treatment.

    9. Control and Optimization

    Modern cooling systems use variable frequency drives and advanced controls to match cooling output to plant load and ambient conditions. This reduces auxiliary power consumption at part load.

    Common Mistakes in Cooling System Selection

    Even experienced designers make mistakes. Common ones include:

    • Underestimating water consumption: Especially for wet cooling in water-scarce regions
    • Ignoring ambient extremes: Designing for average conditions rather than worst-case
    • Overlooking regulations: Discovering too late that thermal discharge or intake rules prohibit the chosen system
    • Undersizing cooling towers: Leading to higher back pressure and reduced output
    • Neglecting auxiliary power: Forgetting that fans and pumps reduce net output
    • Poor water treatment: Leading to scaling, corrosion, and reduced performance

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Cooling System Selection

    Japanese engineering firms are known for their disciplined approach to cooling system design. Common characteristics include:

    • Thorough site assessment: Water availability, ambient conditions, and regulations are studied carefully before selection.
    • Conservative design margins: Cooling systems are sized with adequate margin for worst-case conditions.
    • Life-cycle cost focus: Capital cost is evaluated alongside operating cost, water cost, and environmental compliance.
    • Detailed water treatment design: Water chemistry is managed carefully to ensure long-term reliability.
    • Long-term performance monitoring: Cooling system performance is tracked over the plant’s life.

    For plant owners, this often means a cooling system that performs reliably for decades, even under challenging conditions.

    How to Evaluate Cooling System Options

    When reviewing cooling system options, ask:

    Question Why It Matters
    What is the ambient design condition? Determines cooling performance and system size
    Is water available, and at what cost? Affects selection and operating cost
    What are the environmental regulations? Constrains system options
    What is the auxiliary power consumption? Reduces net plant output
    What is the life-cycle cost? Captures total cost, not just capital
    How reliable is the system? Affects plant availability
    How complex is operation and maintenance? Affects staffing and long-term cost

    A cooling system that satisfies all these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Cooling system selection affects efficiency, water use, cost, and environmental impact
    • Once-through: highest efficiency, highest water use
    • Closed-loop: moderate efficiency, moderate water use
    • Air-cooled: lowest efficiency, zero water use
    • Hybrid systems balance wet and dry cooling
    • Japanese EPC firms emphasize thorough site assessment and conservative design margins

    Conclusion

    Cooling system selection is a strategic decision that affects efficiency, water consumption, environmental impact, and cost. Once-through, closed-loop, and air-cooled systems each have distinct advantages and drawbacks. For small to medium-scale industrial plants, the right choice depends on site conditions, water availability, regulations, and financial objectives.

    By evaluating these factors carefully and considering life-cycle cost, owners and designers can select a cooling system that performs reliably and economically for decades.

  • HRSG Design and Operation: Key Considerations for Combined Cycle Plants

    HRSG Design and Operation: Key Considerations for Combined Cycle Plants

    The heat recovery steam generator (HRSG) is the component that makes combined cycle power generation possible. Without it, the hot exhaust gas from the gas turbine would be wasted, and the plant would operate as a simple cycle with much lower efficiency.

    For plant owners and engineers working with combined cycle plants, understanding HRSG design and operation is essential. The HRSG determines how much additional electricity the plant can produce, how quickly it can respond to load changes, and how reliably it operates over its life.

    This article covers the fundamentals of HRSG design, the key configuration options, operational considerations, and common issues that plant owners should be aware of.

    What Is an HRSG?

    An HRSG is a heat exchanger that recovers heat from the gas turbine exhaust and uses it to produce steam. That steam then drives a steam turbine to generate additional electricity.

    The basic flow is:

    • Gas turbine exhaust enters the HRSG
    • Heat is transferred to water and steam in tubes
    • Steam is produced at one or more pressure levels
    • Steam drives the steam turbine
    • Exhaust gas exits the HRSG at a much lower temperature

    The HRSG is essentially a boiler that has no burner of its own. All its heat comes from the gas turbine exhaust.

    Why the HRSG Matters

    The HRSG is the key to combined cycle efficiency. In a simple cycle plant, exhaust gas leaves the gas turbine at 500–600°C and is released to the atmosphere. In a combined cycle plant, that same exhaust gas passes through the HRSG, where its heat is used to generate steam.

    The result is that the plant produces significantly more electricity from the same fuel. This is why combined cycle plants achieve 50–60% efficiency, while simple cycle plants achieve only 30–40%.

    The HRSG also affects:

    • Plant output: More steam production means more electricity from the steam turbine.
    • Plant flexibility: HRSG design influences how quickly the plant can start and change load.
    • Plant reliability: HRSG failures can shut down the entire combined cycle plant.
    • Maintenance cost: HRSG components are subject to corrosion, fouling, and thermal fatigue.

    HRSG Configurations

    HRSG pressure level configurations comparison

    HRSGs come in several configurations, each suited to different applications.

    Horizontal vs. Vertical

    Configuration Characteristics Typical Use
    Horizontal Exhaust gas flows horizontally through the HRSG Large combined cycle plants
    Vertical Exhaust gas flows vertically upward Smaller plants, limited footprint

    Horizontal HRSGs are more common in large plants because they are easier to maintain and can accommodate larger tube bundles. Vertical HRSGs are more compact and are sometimes used in smaller installations.

    Number of Pressure Levels

    HRSGs can produce steam at one, two, or three pressure levels.

    Configuration Characteristics Efficiency Impact
    Single pressure Simplest design, one steam drum Lower efficiency, lower cost
    Dual pressure Two steam drums, two pressure levels Moderate efficiency, moderate cost
    Triple pressure Three steam drums, three pressure levels Highest efficiency, highest cost

    Triple pressure HRSGs extract more heat from the exhaust gas and produce more steam, improving overall plant efficiency. However, they are more complex and more expensive.

    For small to medium-scale plants, dual pressure is often a practical compromise between efficiency and cost. Triple pressure adds cost and complexity that may not be justified at smaller scales, while single pressure leaves efficiency on the table.

    Duct Firing

    Some HRSGs include supplementary firing (duct firing) to increase steam production. This increases plant output but reduces efficiency because it adds fuel without recovering additional waste heat. Duct firing also increases NOx emissions, which is a relevant consideration for plants in regulated jurisdictions.

    Duct firing is useful for meeting peak demand but is not typically used for baseload operation.

    Bypass Stacks

    Some HRSGs include a bypass stack that allows the gas turbine to operate independently when the steam cycle is unavailable, which adds flexibility during startup and when the steam side is out of service.

    Key Design Considerations

    1. Pinch Point and Approach Temperature

    The pinch point is the temperature difference between the exhaust gas leaving the evaporator and the saturated steam temperature. The approach temperature is the difference between the saturated steam temperature and the feedwater temperature entering the evaporator.

    Smaller pinch and approach temperatures mean more heat is recovered, improving efficiency. However, they also require larger heat transfer surfaces, increasing cost and footprint.

    Typical values:

    • Pinch point: 8–15°C
    • Approach temperature: 5–10°C

    2. Gas Side Pressure Drop

    The HRSG adds pressure drop to the exhaust gas path. Higher pressure drop reduces gas turbine output. Designers aim to minimize pressure drop while still achieving the required heat transfer.

    3. Tube Material Selection

    HRSG tubes are exposed to high temperatures and corrosive gases. Material selection depends on:

    • Exhaust gas temperature
    • Fuel composition (especially sulfur content)
    • Steam pressure and temperature
    • Expected operating hours

    Common materials include carbon steel for lower-temperature sections and alloy steels for higher-temperature sections.

    4. Drum Design and Sizing

    The steam drum separates steam from water and provides a buffer for load changes. Drum size affects the HRSG’s ability to handle rapid load changes and startup.

    5. Thermal Cycling

    HRSGs in cycling plants experience frequent thermal cycling, which causes fatigue in tubes, headers, and drums. Design must account for the expected number of cycles over the plant’s life.

    Operational Considerations

    Startup and Shutdown

    HRSG startup must be carefully controlled to avoid thermal stress. Key parameters include:

    • Drum heat-up rate
    • Tube metal temperature gradients
    • Steam temperature matching between HRSG and steam turbine

    Rapid startups increase thermal stress and can shorten component life.

    Water Chemistry

    Water quality is critical for HRSG reliability. Poor water chemistry leads to:

    • Scale formation on tubes
    • Corrosion of tube surfaces
    • Carryover of impurities into the steam turbine

    Water chemistry must be monitored continuously and controlled within strict limits.

    Fouling and Corrosion

    HRSG tubes can foul with deposits from exhaust gas, especially if the fuel contains sulfur or other impurities. Fouling reduces heat transfer and increases pressure drop, reducing plant efficiency.

    Corrosion can occur on the gas side (from acidic gases) or the water side (from poor water chemistry). Both must be managed through design, operation, and maintenance.

    Load Changes

    HRSGs respond to load changes more slowly than gas turbines. When the gas turbine load changes, the HRSG takes time to reach a new steady state. This affects the plant’s ability to respond to grid demand.

    Common HRSG Problems

    Even well-designed HRSGs can experience problems. Common issues include:

    • Tube failures: Caused by corrosion, fatigue, or overheating
    • Drum level instability: Caused by rapid load changes or poor control
    • Steam temperature excursions: Caused by changes in gas turbine load or exhaust temperature
    • Fouling and plugging: Caused by deposits from exhaust gas
    • Corrosion: Caused by acidic gases or poor water chemistry

    These problems can lead to reduced output, increased maintenance, and in severe cases, plant shutdown.

    How Japanese EPC Firms Approach HRSG Design

    Japanese engineering firms are known for their disciplined approach to HRSG design and operation. Common characteristics include:

    • Conservative design margins: Adequate pinch and approach temperatures, generous tube surface area
    • Careful material selection: Materials matched to fuel and operating conditions
    • Detailed thermal analysis: Startup and shutdown procedures designed to minimize thermal stress
    • Strict water chemistry control: Comprehensive monitoring and treatment programs
    • Long-term performance monitoring: Heat transfer and pressure drop tracked over the plant’s life

    For plant owners, this often means an HRSG that performs reliably for decades, even under cycling operation.

    How to Evaluate HRSG Design

    When reviewing an HRSG design, ask:

    Question Why It Matters
    What pinch and approach temperatures are specified? Determines efficiency and surface area
    How many pressure levels? Affects efficiency and complexity
    What materials are used for tubes? Determines resistance to corrosion and fatigue
    How is thermal cycling addressed? Affects component life in cycling plants
    What water chemistry limits apply? Determines reliability and maintenance needs
    How is fouling managed? Affects long-term performance
    What is the expected pressure drop? Affects gas turbine output

    A design that addresses these questions is likely to perform well over the plant’s life.

    Conclusion

    The HRSG is the heart of a combined cycle plant. It determines how much additional electricity the plant can produce and how efficiently it uses fuel. Understanding HRSG design and operation helps plant owners evaluate proposals, plan maintenance, and optimize performance.

    For small to medium-scale combined cycle plants, the HRSG is often the most technically complex component. Careful attention to design, materials, water chemistry, and operational procedures is essential for reliable, efficient operation over the plant’s life.

    Key Takeaways

    • The HRSG recovers gas turbine exhaust heat to produce steam, which is what lifts combined cycle efficiency well above simple cycle.
    • Configuration (horizontal or vertical, number of pressure levels) affects efficiency, cost, and complexity.
    • Pinch point and approach temperature are key design parameters, trading heat recovery against surface area and cost.
    • Water chemistry control and thermal cycling management are critical for long-term reliability.