Every plant faces the same dilemma with spare parts. Stock too much, and capital sits on shelves, inventory costs rise, and parts may degrade before they are used. Stock too little, and a single missing part can idle the plant for weeks while waiting for delivery.
Spare parts management is the discipline of finding the right balance: having the parts you need, when you need them, without tying up more capital than necessary. For small to medium-scale industrial plants, this balance is especially critical because there is less redundancy and fewer resources to absorb the consequences of either extreme.
This article covers the key strategies for effective spare parts management, from categorization and criticality analysis to inventory optimization, inventory accuracy, procurement of spares for new equipment, and obsolescence management.
Why Spare Parts Management Matters
Spare parts management directly affects plant performance.
| Factor | Impact of Good Spare Parts Management | Impact of Poor Spare Parts Management |
|---|---|---|
| Availability | Parts available when needed | Extended downtime waiting for parts |
| Maintenance cost | Controlled, predictable | Emergency purchases at premium prices |
| Capital tied up | Optimized inventory | Excess inventory or stockouts |
| Equipment life | Parts replaced on schedule | Delayed maintenance shortens equipment life |
| Production | Minimal disruption | Lost production during extended outages |
| Safety | Safety-critical parts replaced promptly | Pressure to run degraded equipment or improvise repairs |
For plant owners, spare parts management is where reliability and cost control meet. Getting it right means the plant can respond quickly to failures without carrying excessive inventory.
The Spare Parts Challenge
Spare parts management involves balancing competing objectives:
- Availability: Parts must be available when needed.
- Cost: Inventory ties up capital and incurs carrying costs.
- Space: Storage space is limited, especially in small plants.
- Obsolescence: Parts may become outdated or unavailable over time.
- Deterioration: Some parts degrade or reach shelf-life limits during storage.
The goal is neither to minimize inventory nor to maximize availability. It is to find the balance that minimizes total cost, including the cost of downtime, while maintaining acceptable reliability.
Categories of Spare Parts
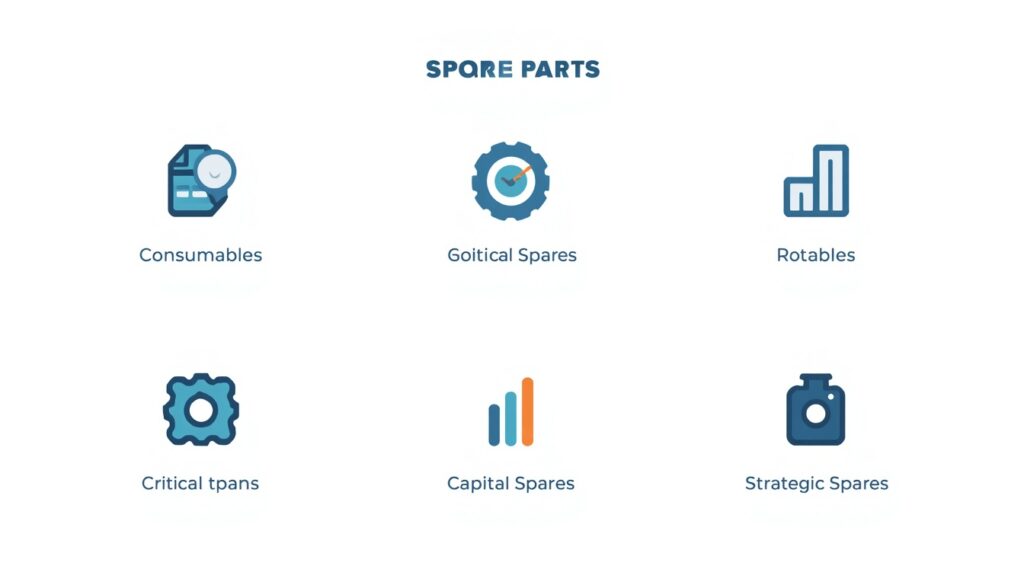
Not all spare parts are the same. Different categories require different management strategies.
| Category | Description | Typical Examples | Strategy |
|---|---|---|---|
| Consumables | Used regularly, low cost | Filters, lubricants, gaskets, belts | Reorder on usage, keep modest stock |
| Critical spares | Essential for operation, may have long lead times | Pump internals, control valves, instrument components | Stock based on lead time and criticality |
| Insurance spares | Expensive items with low failure probability but severe consequences | Turbine rotors, large motors, transformers | Justify by comparing holding cost with expected downtime cost |
| Rotables | Components swapped out and repaired | Motors, pumps, gearboxes | Maintain pool, track repair status |
| Capital spares | Very high-cost items, rarely needed, often capitalized | Major equipment, spare generators | Justify with detailed risk analysis |
| Strategic spares | Parts at risk of obsolescence | Proprietary parts, discontinued items | Purchase before unavailability |
The boundary between insurance and capital spares varies by organization. Insurance spares are defined by their risk profile (low probability, high consequence), while capital spares are defined by their cost and accounting treatment. Many items, such as a main transformer, are both.
Each category requires a different approach. Treating all parts the same leads to either excess inventory or stockouts.
Justifying Insurance Spares
Insurance spares are justified by comparing the cost of holding the part against the expected cost of downtime if the part is not available. The expected cost is the probability of failure over the planning period, multiplied by the cost of the resulting outage. The outage cost depends on how long the plant would be down, which is driven largely by the lead time to obtain a replacement, multiplied by the cost of lost production per day. If the expected cost exceeds the annual holding cost, the spare is justified.
A simple illustration: a large motor has a 2% chance of failing in any given year, a replacement lead time of 26 weeks (182 days), and lost margin of $20,000 per day. The expected annual downtime cost is 0.02 × 182 × $20,000 = $72,800. If the annual holding cost of the spare (capital cost, storage, insurance, and preservation) is less than this figure, the spare is justified. If it is much higher, alternatives such as a shared pool, supplier-held stock, or a faster repair contract may be more economical.
Note that expected-value logic can understate the case for rare but catastrophic events. Where the consequence threatens the viability of the business or safety, owners often stock the spare regardless of the calculated result.
Criticality Analysis
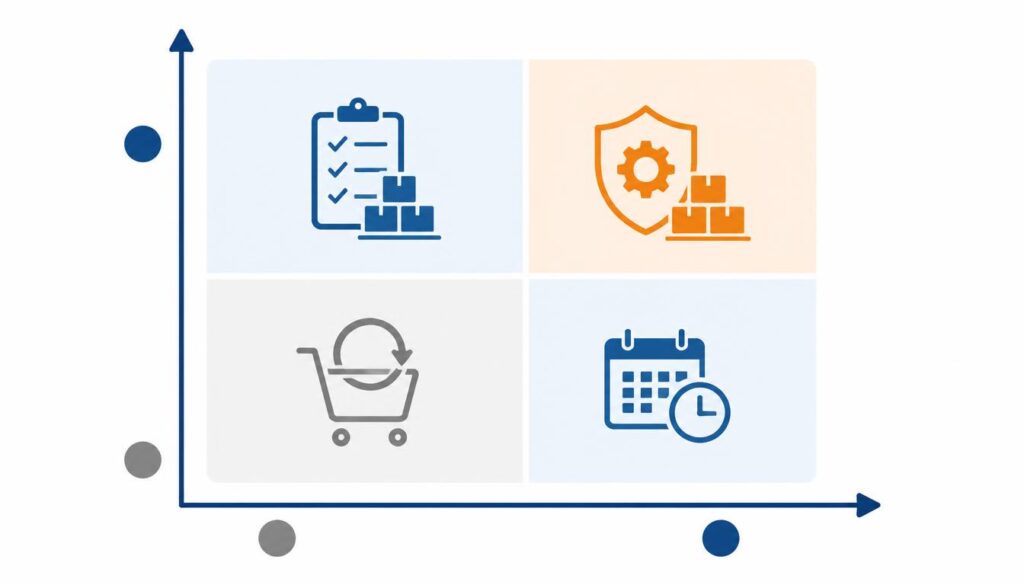
Criticality analysis determines which spare parts deserve the most attention. It considers:
- Equipment criticality: How important is the equipment to plant operation, safety, and environmental compliance?
- Failure likelihood: How likely is the part to fail?
- Lead time: How long does it take to obtain the part?
- Cost: What is the cost of the part versus the cost of downtime?
- Availability: Is the part readily available or scarce?
- Redundancy: Is there a standby unit that could carry the load?
A simple criticality matrix:
| Low Lead Time | High Lead Time | |
|---|---|---|
| High Equipment Criticality | Stock minimum; reliable reorder | Stock based on risk analysis |
| Low Equipment Criticality | Reorder on demand | Evaluate cost versus risk |
Criticality analysis helps direct limited inventory budget to the parts that matter most. It works best when the equipment criticality ranking is shared with the maintenance strategy, so that the same assets that receive the most preventive attention also receive the most spares attention.
Determining Stock Levels
Stock levels depend on several factors.
Key inputs:
- Lead time: How long does it take to obtain the part?
- Consumption rate: How often is the part used?
- Criticality: What happens if the part is not available?
- Cost: What is the cost of holding versus not holding?
- Reliability: How likely is the part to fail?
Stock level approaches:
| Approach | Description | When to Use |
|---|---|---|
| Min-max | Reorder when stock falls to the minimum; order up to the maximum | Simple, widely used |
| Reorder point | Order when stock reaches expected demand during lead time plus safety stock | When demand is predictable |
| Economic order quantity (EOQ) | Order size that minimizes the sum of ordering and holding costs, √(2 × annual demand × cost per order ÷ annual holding cost per unit) | When demand is stable and continuous |
| Criticality-based | Stock based on criticality and consequence, not just usage | For critical and insurance spares |
Statistical methods work well for consumables with steady demand. They work poorly for critical spares, which are used rarely and irregularly. For these items, the decision should rest on criticality, lead time, and failure consequence rather than historical consumption. Zero consumption does not mean a part is unnecessary.
For small plants, a min-max or criticality-based approach is often the most practical.
Lead Time Considerations
Lead time is often the single most important factor in spare parts management.
Lead time components:
- Requisition and approval: Time to raise and approve a purchase order.
- Manufacturing: Time for the supplier to manufacture or assemble.
- Shipping: Time for transport.
- Customs and clearance: Time for import procedures (for international suppliers).
- Receiving and inspection: Time to receive and verify the part.
For long-lead items, the lead time may exceed the time the plant can afford to be down. These items justify stocking, even at high cost.
Lead time strategies:
- Stock items with lead times longer than acceptable downtime.
- Identify alternate suppliers for critical parts.
- Consider local stock or consignment arrangements.
- Pre-approve purchasing authority for emergency orders to shorten the requisition step.
- Monitor lead times regularly; they change over time, and quoted lead times are often optimistic.
Inventory Optimization
Inventory optimization balances availability and cost.
Key concepts:
- Carrying cost: The cost of holding inventory (capital, space, insurance, taxes, deterioration). Annual carrying costs are commonly estimated at 15% to 30% of inventory value.
- Ordering cost: The cost of placing and processing orders.
- Stockout cost: The cost of not having a part when needed (downtime, emergency purchases, expediting).
- Service level: The probability of having a part when needed.
Optimization approaches:
- ABC analysis: Classify parts by annual consumption value (unit cost multiplied by annual usage). A items are the small share of parts that account for most of the value and receive close management; C items are the large share of parts that account for little value and receive simple management.
- VED analysis: Classify parts by criticality (Vital, Essential, Desirable).
- FSN analysis: Classify parts by movement (Fast, Slow, Non-moving).
- Combined analysis: Use ABC and VED together to prioritize. A vital C item, such as a low-cost relay whose failure stops the plant, deserves more attention than its value suggests.
For small plants, a combined ABC-VED analysis is often the most practical approach.
Inventory Accuracy
Inventory records are only useful if they are accurate. Inventory accuracy is essential: a system that says a part is in stock when it is not is worse than having no system, because the shortfall is discovered during a breakdown.
Regular cycle counting, which means counting a portion of the inventory on a rotating basis, helps maintain accuracy without the disruption of full physical inventories. A common approach is to count A and vital items more frequently (for example, quarterly) and C items less often (for example, annually).
Good practices for accuracy include:
- Controlled access to the storeroom, with all issues and returns recorded.
- Unique part numbers and clear bin locations.
- Investigating discrepancies to find root causes rather than simply adjusting the record.
- Tracking accuracy as a performance measure.
Storage and Preservation
Spare parts must be stored correctly to remain usable when needed.
Storage considerations:
- Environment: Temperature, humidity, and contamination control.
- Packaging: Original packaging or equivalent protection.
- Handling: Proper equipment and procedures for heavy or delicate parts.
- Identification: Clear labeling and inventory records.
- Access: Parts should be accessible without excessive handling.
- Shelf life: Date-coded items (elastomers, adhesives, lubricants, batteries) should be issued first-in, first-out and checked before use.
Preservation requirements:
- Rotating equipment: Periodic turning or lubrication, following the manufacturer’s instructions.
- Elastomers: Protection from heat, light, and ozone.
- Electronics: Protection from moisture and static.
- Chemicals: Proper containment and segregation.
- Batteries: Periodic charging or replacement.
Parts that degrade in storage create false confidence. A spare that fails on installation is worse than a known gap, because the team believed the risk was covered. Periodic inspection or testing of critical spares closes this gap.
Spare Parts for New Equipment
When specifying new equipment, include spare parts requirements in the procurement contract. Vendors can often provide recommended spares lists, and including them in the original order is usually cheaper than purchasing them later.
Recommended spares lists are typically divided into:
- Commissioning spares: Parts likely to be needed during installation, startup, and commissioning.
- Initial or operating spares: Parts recommended for the first period of operation, often one to two years.
- Capital or insurance spares: Long-lead or high-value items held against major failure.
Vendor lists should be treated as a starting point, not a final answer. Review them against the plant’s own criticality analysis, existing inventory, and operating conditions. Vendors may over-recommend, while a plant with standardized equipment may already hold suitable parts.
Additional contract provisions worth considering:
- Guaranteed availability of spares for a defined period (for example, 10 to 15 years).
- Advance notice of discontinuation, with a last-time buy option.
- Price protection or agreed price lists for spares.
- Delivery of spare parts documentation and part numbers with the equipment.
- Standardization of equipment types where possible, to reduce the variety of spares required.
Cannibalization
In some plants, parts are removed from one piece of equipment to keep another running. Cannibalization, which is removing parts from one asset to keep another running, is sometimes necessary in an emergency, but it should be tracked. A cannibalized asset becomes a future risk if it is not restored.
Good practice includes:
- Requiring formal approval for cannibalization.
- Recording the removal in the CMMS against the donor asset.
- Raising a replacement order immediately, so that the donor is restored.
- Tracking the number of open cannibalizations as an indicator of spares shortfall.
Frequent cannibalization usually signals that stock levels or the procurement process need attention.
Obsolescence Management
Parts become obsolete when manufacturers discontinue them or when technology changes. Obsolescence is a growing problem as equipment lifecycles lengthen, particularly for electronics and control systems.
Obsolescence risks:
- Discontinued parts: No longer manufactured or supported.
- Technology changes: Old technology replaced by new.
- Supplier changes: Supplier exits the business or changes product lines.
- Regulatory changes: Parts no longer compliant with regulations.
Obsolescence strategies:
- Identify at-risk parts: Which parts are likely to become obsolete? Ask vendors for lifecycle status of control systems and instruments.
- Last-time buy: Purchase sufficient stock before discontinuation, taking care to estimate lifetime demand and storage conditions.
- Alternate sources: Identify substitute parts or suppliers.
- Redesign: Modify equipment to use available parts.
- Reverse engineering: Manufacture equivalents when needed, subject to quality, safety, and intellectual property considerations.
- Refurbished or reclaimed parts: Consider certified refurbished items where new parts are unavailable.
For small plants, obsolescence is often overlooked until a part becomes unavailable. Proactive identification and last-time buys can prevent future problems.
Spare Parts and CMMS
A computerized maintenance management system (CMMS) is essential for effective spare parts management.
CMMS functions for spare parts:
- Inventory tracking: Current stock levels, locations, and values.
- Reorder management: Automatic reorder when stock falls below minimum.
- Usage history: Which parts are used, how often, and on which equipment.
- Bill of materials: Linking parts to the equipment that uses them, to support criticality analysis and identify shared spares.
- Work order integration: Reserving and issuing parts against planned work.
- Supplier management: Supplier details, lead times, and pricing.
- Cost tracking: Parts cost per equipment, per area, per period.
- Reporting: Stock status, usage trends, obsolescence risk.
Without a CMMS, spare parts management relies on memory and manual records, which leads to errors and inefficiencies.
Supplier Management
Suppliers are partners in spare parts management.
Key considerations:
- Reliability: Does the supplier deliver on time and to specification?
- Lead time: How long does the supplier take to deliver?
- Pricing: Is the pricing competitive and transparent?
- Technical support: Does the supplier provide technical assistance?
- Stocking arrangements: Does the supplier hold stock on your behalf?
- Consignment: Can parts be held on consignment (paid only when used)?
- Authenticity: Are parts genuine and traceable, particularly for pressure-retaining and safety-critical items?
Supplier strategies:
- Develop relationships with key suppliers.
- Identify alternate suppliers for critical parts.
- Negotiate stocking or consignment arrangements.
- Explore pooling or sharing arrangements with neighboring plants for expensive, rarely used items.
- Monitor supplier performance.
For small plants, a few reliable suppliers with strong support are often better than many suppliers with weaker relationships.
Measuring Performance
What is measured tends to improve. Useful spare parts performance indicators include:
| Indicator | What It Shows |
|---|---|
| Stock availability (service level) | How often a needed part is in stock |
| Inventory turnover | Annual usage value divided by average inventory value |
| Inventory accuracy | Match between records and physical counts |
| Stockouts causing downtime | Direct cost of gaps |
| Emergency purchases | Frequency and premium paid |
| Obsolete or dead stock | Capital tied up in unused items |
| Open cannibalizations | Hidden shortfalls |
Low turnover is not automatically bad for critical and insurance spares, which are held for rare events. Judge those on criticality, and judge consumables on turnover.
Common Mistakes in Spare Parts Management
Even experienced teams make mistakes. Common ones include:
- Stocking everything: Tying up capital in parts that may never be used.
- Stocking nothing: Risking extended downtime for lack of a critical part.
- Ignoring lead time: Discovering too late that a part takes months to obtain.
- No criticality analysis: Treating all parts the same.
- Poor storage: Parts degrade in storage and are unusable when needed.
- Inaccurate records: Trusting stock counts that do not match the shelf.
- Untracked cannibalization: Leaving donor equipment unrestored.
- Ignoring spares at purchase: Missing the chance to buy spares cheaply with new equipment.
- No obsolescence planning: Discovering a part is discontinued when it fails.
- No CMMS: Relying on memory and manual records.
- No supplier relationships: Struggling to obtain parts quickly when needed.
These mistakes are costly to correct after a failure. They are much cheaper to avoid through good planning.
How Japanese EPC Firms Approach Spare Parts Management
Japanese engineering firms are often noted for their disciplined approach to spare parts management. Common characteristics include:
- Thorough criticality analysis: Parts are categorized by criticality and risk.
- Detailed planning: Stock levels, lead times, and obsolescence are planned in advance, often as part of the project handover.
- Strong supplier relationships: Long-term relationships with reliable suppliers.
- Comprehensive documentation: Inventory records, usage history, and supplier data are carefully maintained.
- Proactive obsolescence management: At-risk parts are identified and addressed early.
- Long-term focus: Spare parts management is treated as a long-term commitment, not a short-term cost.
For plant owners, this often means higher availability, lower emergency costs, and fewer unpleasant surprises.
How to Evaluate Spare Parts Management
When reviewing spare parts management, ask:
| Question | Why It Matters |
|---|---|
| Are parts categorized by criticality? | Focuses attention on the parts that matter |
| Are stock levels based on lead time and criticality? | Balances availability and cost |
| Are insurance spares justified by risk analysis? | Avoids both over- and under-investment |
| Are inventory records accurate and cycle counted? | Ensures the system can be trusted |
| Is storage adequate for preservation? | Ensures parts are usable when needed |
| Were spares specified with new equipment? | Captures lower prices and avoids later gaps |
| Is cannibalization tracked and reversed? | Prevents hidden risk |
| Is obsolescence managed proactively? | Prevents future unavailability |
| Is a CMMS in place? | Enables effective tracking and management |
| Are supplier relationships strong? | Ensures parts can be obtained quickly |
| Is inventory reviewed regularly? | Keeps stock levels aligned with needs |
A plant that addresses these questions is likely to have effective spare parts management.
Conclusion
Spare parts management is a critical but often overlooked aspect of plant reliability and cost control. For small to medium-scale industrial plants, the right balance between availability and cost is essential.
By categorizing parts, analyzing criticality, optimizing stock levels, keeping records accurate, specifying spares with new equipment, managing obsolescence, and building supplier relationships, owners and maintenance teams can ensure that parts are available when needed, without tying up excessive capital.
Key Takeaways
- Spare parts management balances availability and cost
- Categories include consumables, critical spares, insurance spares, rotables, capital spares, and strategic spares
- Insurance spares are justified by comparing holding cost with the expected cost of downtime
- Criticality analysis directs attention to the parts that matter most
- Lead time is often the single most important factor
- Accurate inventory records, maintained through cycle counting, make the whole system trustworthy
- Specify spares in the procurement contract for new equipment; it is usually cheaper than buying later
- Track cannibalization, because a cannibalized asset is a future risk
- Obsolescence management prevents future unavailability
- A CMMS is essential for effective tracking and management
- Japanese EPC firms emphasize thorough criticality analysis and proactive obsolescence management