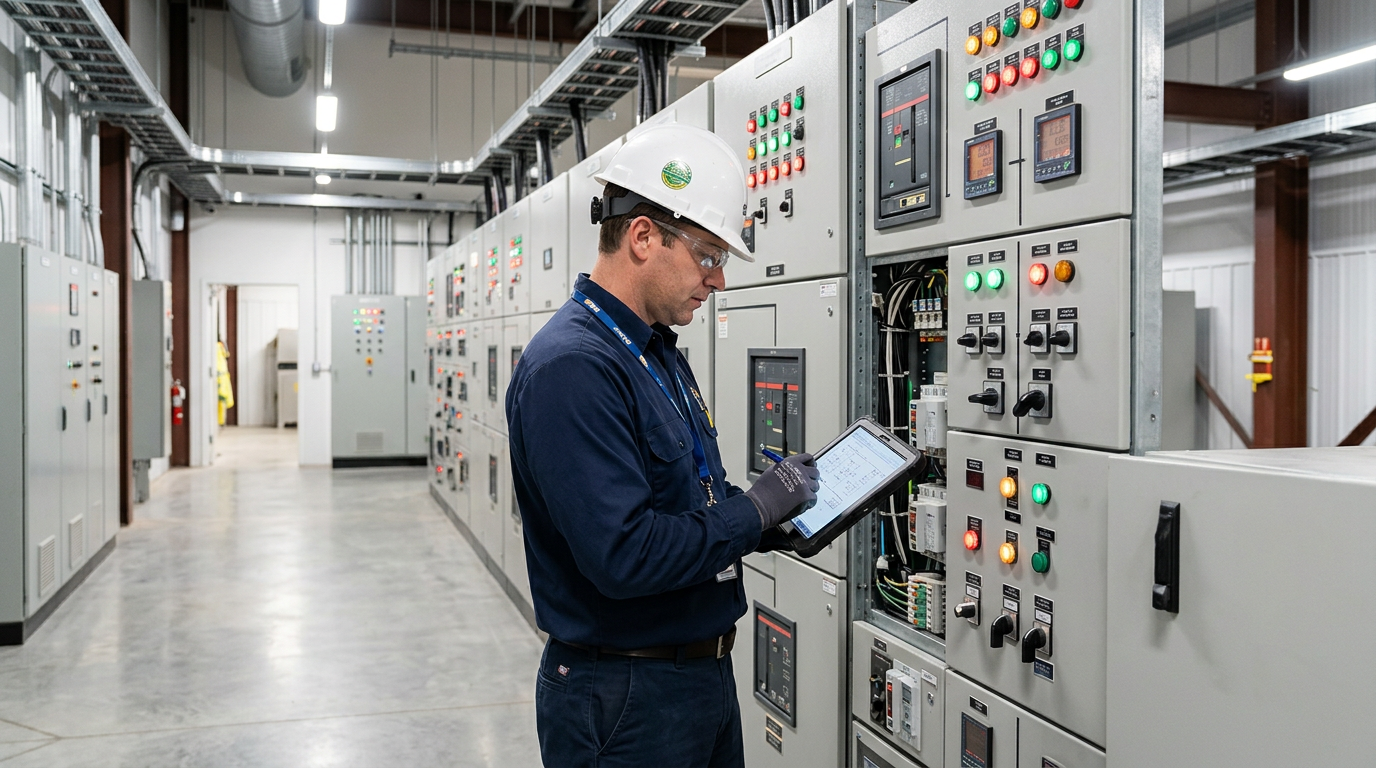
Tag: Industrial Plant

  • Electrical Systems for Industrial Plants: Key Design Considerations

    Electrical Systems for Industrial Plants: Key Design Considerations

    Electrical systems are the nervous system of an industrial plant. They power motors, control instruments, provide lighting, and ensure safety systems function when needed. Unlike mechanical systems, which can sometimes be bypassed or operated manually, electrical systems must operate correctly every time. A failure can shut down the entire plant—or worse, create a safety hazard.

    For small to medium-scale industrial plants, electrical system design is especially critical because there is less redundancy and fewer resources to manage complexity. The right design ensures reliable power, safe operation, and room for future expansion.

    This article covers the key considerations in electrical system design for industrial plants, from power supply to distribution, protection, and control.

    The Main Electrical Systems in an Industrial Plant
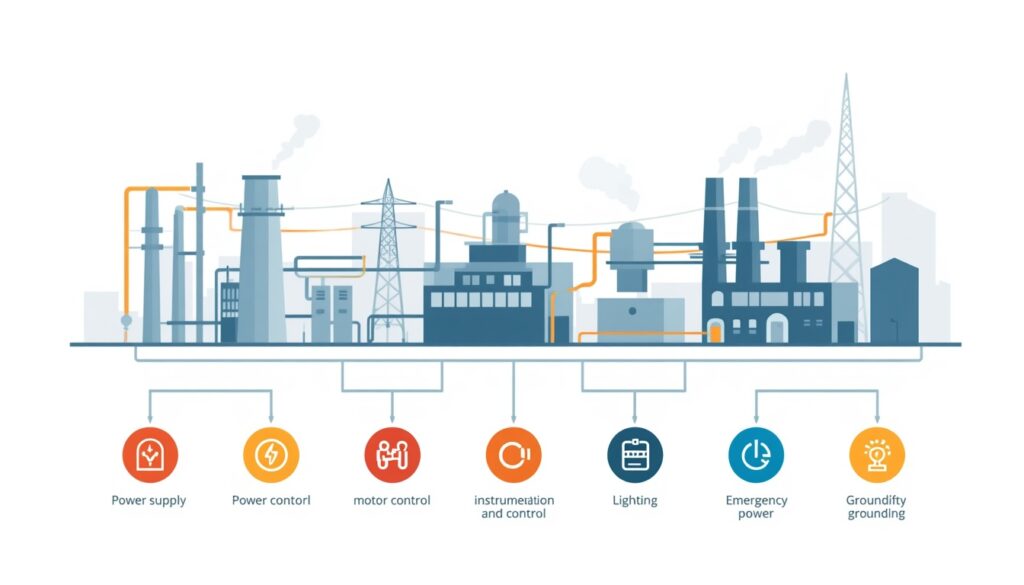
    Main electrical systems in an industrial plant diagram

    An industrial plant’s electrical system can be divided into several subsystems, each with its own function.

    System Purpose
    Power supply Receives power from the grid or on-site generation
    Power distribution Delivers power to equipment throughout the plant
    Motor control Starts, stops, and protects motors
    Instrumentation and control Monitors and controls process variables
    Lighting Provides illumination for operation, maintenance, and safety
    Emergency power Provides backup power for critical systems
    Grounding and lightning protection Protects people and equipment from electrical hazards

    Each subsystem must be designed to work with the others. A weakness in any one can compromise the entire plant.

    Power Supply

    The first decision in electrical system design is how the plant will receive power.

    Grid supply: Most industrial plants receive power from the local utility grid. The supply voltage depends on the utility and the plant’s size. Small plants may receive power at low voltage (e.g., 400 V or 480 V), while larger plants receive power at medium voltage (e.g., 6.6 kV, 11 kV, or 33 kV) and step it down on site.

    On-site generation: Some plants generate their own power using gas turbines, diesel generators, or renewable sources. This provides independence from the grid but adds complexity and cost.

    Combined supply: Many plants use both grid supply and on-site generation. This provides redundancy and allows the plant to operate during grid outages.

    Key considerations for power supply:

    • Reliability: How often does the grid fail, and how long do outages last?
    • Power quality: Voltage sags, harmonics, and frequency variations can affect equipment.
    • Cost: Tariff structures, demand charges, and time-of-use rates affect operating cost.
    • Future expansion: Will the plant need more power later?

    Power Distribution

    Once power enters the plant, it must be distributed to equipment throughout the site.

    Distribution voltages: Plants typically use multiple voltage levels:

    • Medium voltage (e.g., 6.6 kV, 11 kV, 33 kV): For distribution across the site and to large motors.
    • Low voltage (e.g., 400 V, 480 V): For small motors, lighting, and control systems.
    • Extra-low voltage (e.g., 24 V DC): For instrumentation and control.

    Transformers step voltage down between levels.

    Distribution configurations:

    Configuration Characteristics Typical Use
    Radial Simple, single path from source to load Small plants, non-critical loads
    Ring Power feeds from two directions Medium plants, improved reliability
    Network Multiple sources and paths Large plants, high reliability

    For small to medium-scale plants, radial distribution is often sufficient. Ring distribution may be justified for critical loads.

    Key considerations for power distribution:

    • Voltage drop: Long cable runs cause voltage drop, which affects motor performance.
    • Cable sizing: Cables must be sized for current, voltage drop, and short-circuit withstand.
    • Routing: Cables should be routed away from hot surfaces, moisture, and mechanical damage.
    • Segregation: Power and instrument cables should be segregated to avoid interference.

    Power factor correction: Many utilities charge penalties for low power factor. Power factor correction capacitors or synchronous condensers may be required to maintain power factor above a specified threshold.

    Harmonics and filtering: Non-linear loads such as VFDs and rectifiers generate harmonics that can distort voltage and affect sensitive equipment. Harmonic filters or active compensators may be required.

    Motor Control
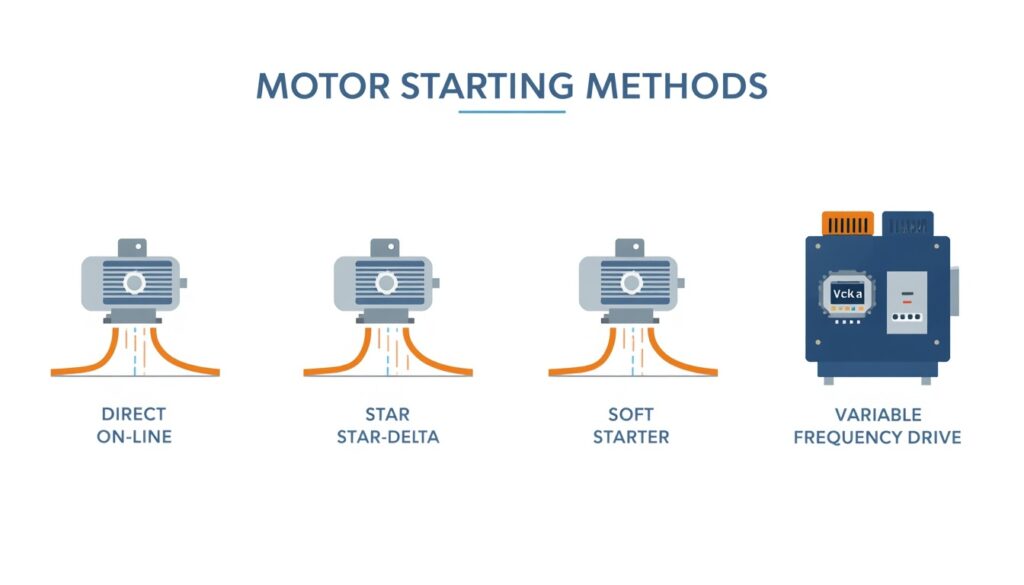
    Comparison of motor starting methods for industrial plants

    Motors are the largest electrical loads in most industrial plants. They drive pumps, fans, compressors, and conveyors.

    Motor starting: Large motors draw high starting current, which can cause voltage dips. Starting methods include:

    • Direct-on-line (DOL): Simple but high starting current.
    • Star-delta: Reduces starting current but adds complexity.
    • Soft starter: Gradually increases voltage to reduce starting current.
    • Variable frequency drive (VFD): Controls motor speed and torque, with low starting current.

    Motor protection: Motors must be protected against:

    • Overload: Excessive current due to mechanical or electrical faults.
    • Short circuit: Faults that cause very high current.
    • Phase loss: Loss of one phase in a three-phase supply.
    • Earth fault: Current leaking to ground.

    Protection devices include overload relays, circuit breakers, and earth fault relays.

    Key considerations for motor control:

    • Starting method: Depends on motor size, load characteristics, and grid strength.
    • Protection coordination: Protection devices must coordinate to isolate faults without unnecessary trips.
    • Control philosophy: Local vs. remote control, manual vs. automatic operation.

    Instrumentation and Control

    Instrumentation and control systems monitor process variables and adjust equipment to maintain desired conditions.

    Control system types:

    Type Characteristics Typical Use
    Relay logic Simple, hardwired Small plants, simple processes
    PLC Programmable, flexible Most industrial plants
    DCS Distributed, integrated Large, complex plants
    SCADA Supervisory control and data acquisition Plants requiring remote monitoring

    For small to medium-scale plants, PLC-based control is common. It offers flexibility and is well-supported by vendors.

    Key considerations for instrumentation and control:

    • Signal types: Analog (4–20 mA), digital, and fieldbus communications.
    • Redundancy: Critical control loops may require redundant sensors or controllers.
    • Cybersecurity: Control systems are increasingly connected to networks, creating security risks.
    • Human-machine interface (HMI): Operators need clear, intuitive displays.

    Lighting

    Lighting is often overlooked but essential for safe operation and maintenance.

    Lighting types:

    • General lighting: Illuminates work areas.
    • Task lighting: Provides focused light for specific tasks.
    • Emergency lighting: Provides illumination during power failures.
    • Outdoor lighting: Illuminates access roads, storage areas, and perimeters.

    Key considerations for lighting:

    • Illumination levels: Depends on the task and area.
    • Energy efficiency: LED lighting reduces power consumption.
    • Emergency lighting: Must be powered by backup supply.
    • Maintenance access: Light fixtures must be accessible for replacement.

    Emergency Power

    Emergency power systems provide backup power for critical loads during grid outages.

    Emergency power sources:

    • Diesel generators: Common, reliable, but require fuel storage and maintenance.
    • Battery systems: Provide instant power for short outages.
    • Uninterruptible power supplies (UPS): Provide clean, continuous power for sensitive equipment.

    Critical loads requiring emergency power:

    • Safety systems (fire detection, emergency shutdown)
    • Control systems
    • Emergency lighting
    • Critical instrumentation
    • Communication systems

    Key considerations for emergency power:

    • Load list: Which loads require backup power?
    • Duration: How long must backup power last?
    • Startup time: How quickly must backup power come online?
    • Testing: Emergency systems must be tested regularly.

    Grounding and Lightning Protection

    Grounding and lightning protection protect people and equipment from electrical hazards.

    Grounding: Grounding provides a low-resistance path for fault current, allowing protection devices to operate quickly. It also stabilizes voltage and reduces electrical noise.

    Lightning protection: Lightning protection systems intercept lightning strikes and conduct them safely to ground. They include air terminals, down conductors, and grounding electrodes.

    Key considerations:

    • Grounding system design: Must be designed for the site’s soil conditions.
    • Bonding: All metallic structures and equipment must be bonded to the grounding system.
    • Testing: Grounding systems must be tested periodically.

    Arc flash safety: Arc flash studies identify areas where high-energy electrical faults could occur. Appropriate labeling, PPE requirements, and work procedures must be in place.

    Key Design Considerations

    1. Load Analysis
    The first step in electrical design is a load analysis. This determines the total connected load, demand load, and future load.

    2. Redundancy
    Critical systems may require redundant power supplies, transformers, or feeders. The level of redundancy depends on the consequences of failure.

    3. Protection Coordination
    Protection devices must coordinate so that the device closest to a fault operates first, minimizing disruption.

    4. Cable Routing and Segregation
    Power and instrument cables should be routed separately to avoid interference. Cables should be protected from heat, moisture, and mechanical damage.

    5. Safety
    Electrical systems must comply with applicable codes and standards (e.g., IEC, NEC, local regulations). Safety features include grounding, isolation, and lockout/tagout provisions.

    6. Future Expansion
    Electrical systems should be designed with spare capacity for future loads. This includes spare breakers, spare cable trays, and spare transformer capacity.

    7. Electrical System Studies
    Electrical system studies include load flow analysis, short circuit analysis, protection coordination, and arc flash analysis. These studies should be completed during design and updated as the system changes.

    Common Mistakes in Electrical System Design

    Even experienced designers make mistakes. Common ones include:

    • Undersizing equipment: Leading to overloads and failures.
    • Ignoring voltage drop: Causing poor motor performance.
    • Poor protection coordination: Leading to unnecessary trips or failure to isolate faults.
    • Inadequate grounding: Creating safety hazards and equipment damage.
    • No spare capacity: Requiring costly upgrades for future expansion.
    • Insufficient segregation: Causing electrical noise and interference.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Electrical System Design

    Japanese engineering firms are known for their disciplined approach to electrical system design. Common characteristics include:

    • Thorough load analysis: Loads are analyzed carefully, with margin for future growth.
    • Conservative design margins: Equipment is sized with adequate margin for worst-case conditions.
    • Detailed protection coordination: Protection settings are carefully studied and coordinated.
    • Comprehensive documentation: Drawings, schedules, and test records are carefully maintained.
    • Long-term reliability focus: Designs prioritize reliability and maintainability over lowest initial cost.

    For plant owners, this often means an electrical system that performs reliably for decades, with fewer unplanned outages.

    How to Evaluate Electrical System Design

    When reviewing electrical system design, ask:

    Question Why It Matters
    What is the total connected load and demand load? Determines equipment sizing
    What is the power supply configuration? Affects reliability and cost
    Is redundancy provided for critical loads? Ensures continued operation during faults
    How is protection coordinated? Minimizes disruption from faults
    How are cables routed and segregated? Avoids interference and damage
    Is there spare capacity for future expansion? Avoids costly upgrades later
    Does the design comply with applicable codes? Ensures safety and legal operation

    A design that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Electrical systems are critical to plant reliability, safety, and efficiency
    • Power supply can be from the grid, on-site generation, or both
    • Distribution configurations include radial, ring, and network
    • Motor starting methods include DOL, star-delta, soft starter, and VFD
    • Emergency power is required for safety, control, and critical instrumentation
    • Japanese EPC firms emphasize thorough load analysis and protection coordination

    Conclusion

    Electrical systems are critical to plant reliability, safety, and efficiency. For small to medium-scale industrial plants, electrical design deserves careful attention from the earliest stages of design. By focusing on load analysis, redundancy, protection, safety, and future expansion, owners and designers can ensure reliable power and safe operation for decades.
  • Water Treatment for Industrial Plants: Key Considerations

    Water Treatment for Industrial Plants: Key Considerations

    Water is essential to almost every industrial plant. It is used for cooling, steam generation, process operations, and equipment cleaning. But water is rarely pure. It contains dissolved minerals, suspended solids, dissolved gases, and microorganisms that can cause corrosion, scaling, fouling, and biological growth.

    Water treatment is the process of removing or controlling these impurities so that water can be used safely and reliably in plant systems. For small to medium-scale industrial plants, water treatment is especially critical because there is less redundancy and less margin for error. A poorly treated cooling system can lead to tube failures, reduced output, and costly downtime.

    This article covers the fundamentals of water treatment for industrial plants, the key treatment processes, and the considerations that plant owners should be aware of.

    Why Water Treatment Matters

    Water quality affects plant reliability, efficiency, and cost. Poor water quality can lead to:

    • Corrosion: Dissolved oxygen, low pH, and dissolved solids attack metal surfaces.
    • Scaling: Dissolved minerals precipitate and form deposits on heat transfer surfaces.
    • Fouling: Suspended solids and biological growth block flow and reduce heat transfer.
    • Foaming and carryover: Impurities in boiler water cause foaming, leading to carryover into steam and turbine deposits.
    • Microbiological growth: Bacteria, algae, and fungi form biofilms that reduce heat transfer and promote corrosion.

    These problems reduce plant efficiency, increase maintenance cost, and shorten equipment life. In severe cases, they cause forced outages.

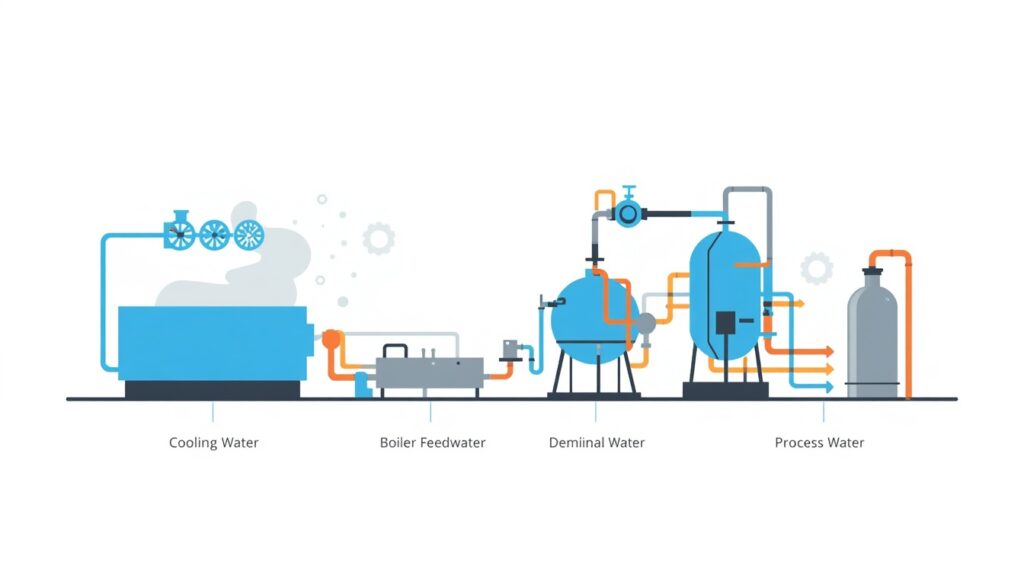
    The Main Water Systems in an Industrial Plant

    Main water systems in an industrial plant diagram

    Main water systems in an industrial plant diagram

    Different plant systems have different water quality requirements.

    System Purpose Key Water Quality Concerns
    Cooling water Reject heat from condensers and auxiliary equipment Scaling, corrosion, biological growth
    Boiler feedwater Produce steam in boilers Scale, corrosion, carryover
    Demineralized water Feed high-pressure boilers and process systems Dissolved solids, silica, conductivity
    Process water Used in chemical or manufacturing processes Varies by process
    Potable water For human consumption and sanitation Microbial, chemical, and aesthetic standards

    Each system requires a different level of treatment. Cooling water typically needs less treatment than boiler feedwater, which must be nearly pure. Process water treatment depends on the specific process. Some processes require demineralized water, while others can tolerate lower quality.

    Key Water Quality Parameters

    Water treatment is designed to control specific parameters. These include:

    • Hardness: Calcium and magnesium ions that cause scaling.
    • Alkalinity: Bicarbonate and carbonate ions that affect pH and scaling potential.
    • pH: Acidity or alkalinity of the water.
    • Conductivity: Measure of dissolved solids.
    • Silica: Forms hard deposits on boiler and turbine surfaces.
    • Dissolved oxygen: Causes corrosion in boilers and cooling systems.
    • Iron and copper: Corrosion products that deposit on surfaces.
    • Chlorides: Cause pitting corrosion in stainless steels.
    • Suspended solids: Cause fouling and deposits.
    • Microorganisms: Cause biofilms and microbiologically influenced corrosion.

    Cooling Water Treatment

    Cooling water treatment challenges including scaling, corrosion, and biological growth

    Cooling water treatment challenges including scaling, corrosion, and biological growth

    Cooling water treatment focuses on three main problems: scaling, corrosion, and biological growth. Treatment requirements also depend heavily on the type of cooling system used.

    Scaling control:

    Scale forms when dissolved minerals precipitate on heat transfer surfaces. The most common scale is calcium carbonate, but calcium sulfate, silica, and other deposits also occur.

    Control methods include:

    • Chemical inhibitors: Phosphonates, polymers, and other chemicals that prevent crystal formation.
    • pH control: Adjusting pH to keep minerals soluble.
    • Blowdown: Removing a portion of recirculating water to control dissolved solids concentration.
    • Softening: Removing hardness ions before they enter the system.

    Corrosion control:

    Corrosion in cooling systems is caused by dissolved oxygen, low pH, chlorides, and microbiological activity.

    Control methods include:

    • Corrosion inhibitors: Chemicals that form protective films on metal surfaces.
    • pH control: Maintaining pH in a range that minimizes corrosion.
    • Material selection: Using corrosion-resistant materials where needed.
    • Cathodic protection: For critical components.

    Biological control:

    Bacteria, algae, and fungi grow in cooling systems, especially in warm water with nutrients.

    Control methods include:

    • Biocides: Oxidizing (chlorine, bromine) or non-oxidizing chemicals that kill microorganisms.
    • Dispersants: Chemicals that break up biofilms.
    • Physical cleaning: Periodic flushing or mechanical cleaning.

    Once-through cooling systems:

    Once-through cooling systems require less chemical treatment than closed-loop systems because water is not recirculated. However, intake screening, chlorination, and corrosion control may still be required.

    Air-cooled systems:

    Plants using air-cooled cooling systems eliminate cooling water treatment, but boiler water treatment and demineralized water production may still be required.

    Boiler Water Treatment

    Boiler water treatment is more demanding than cooling water treatment because boilers operate at high temperature and pressure.

    External treatment:

    External treatment removes impurities before water enters the boiler. Common processes include:

    • Clarification: Removing suspended solids.
    • Filtration: Removing fine particles.
    • Softening: Removing hardness ions.
    • Demineralization: Removing all dissolved solids using ion exchange.
    • Reverse osmosis: Removing dissolved solids using membrane filtration.

    Internal treatment:

    Internal treatment controls residual impurities inside the boiler. Common chemicals include:

    • Oxygen scavengers: Remove dissolved oxygen.
    • pH adjusters: Maintain alkaline pH to minimize corrosion.
    • Scale inhibitors: Prevent precipitation on boiler surfaces.
    • Anti-foaming agents: Prevent foaming and carryover.

    Blowdown:

    Blowdown removes a portion of boiler water to control dissolved solids concentration. Continuous blowdown is preferred for larger boilers; intermittent blowdown is used for smaller ones.

    Demineralized Water Production

    High-pressure boilers and some process systems require demineralized water, which is water with almost all dissolved solids removed.

    Common demineralization processes include:

    • Ion exchange: Uses resins to exchange dissolved ions for hydrogen and hydroxide ions.
    • Reverse osmosis: Uses pressure to force water through a semi-permeable membrane, leaving dissolved solids behind.
    • Electrodeionization (EDI): Combines ion exchange and membrane processes for continuous demineralization.

    Demineralized water is essential for high-pressure boilers because dissolved solids can deposit on turbine blades, causing imbalance and efficiency loss.

    Key Design Considerations

    1. Water Source and Quality — The first step in water treatment design is understanding the water source. Surface water, groundwater, seawater, and municipal water all have different characteristics and require different treatment.
    2. Treatment Goals — Treatment goals depend on the end use. Cooling water, boiler feedwater, and demineralized water each have different quality requirements.
    3. Chemical Storage and Handling — Water treatment chemicals must be stored and handled safely. This requires appropriate containment, ventilation, and personal protective equipment. Personnel handling water treatment chemicals must be trained in safe handling, emergency response, and proper use of personal protective equipment.
    4. Waste Streams — Water treatment produces waste streams, including blowdown, filter backwash, and regeneration waste. These must be managed in compliance with environmental regulations.
    5. Monitoring and Control — Water quality must be monitored continuously. Key parameters include pH, conductivity, hardness, silica, and dissolved oxygen. Automated control systems help maintain treatment within specified limits.
    6. Redundancy — Critical water treatment components (pumps, resin beds, membrane units) may require redundancy to ensure continuous operation.

    Common Mistakes in Water Treatment

    Even experienced designers make mistakes. Common ones include:

    • Undersizing treatment systems: Leading to inadequate water quality and equipment damage.
    • Ignoring water source variability: Water quality changes seasonally and over time.
    • Insufficient chemical storage: Running out of treatment chemicals causes system upsets.
    • Poor waste management: Leading to environmental violations.
    • Inadequate monitoring: Failing to detect water quality excursions before damage occurs.
    • Skipping redundancy: A single point of failure can shut down the plant.

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Water Treatment

    Japanese engineering firms are known for their disciplined approach to water treatment design. Common characteristics include:

    • Thorough water source assessment: Water quality is analyzed over time to capture variability.
    • Conservative design margins: Treatment systems are sized with adequate margin for worst-case water quality.
    • Detailed chemical management: Chemical selection, storage, and handling are carefully planned.
    • Comprehensive monitoring: Water quality is tracked continuously with clear alarm and response procedures.
    • Long-term performance focus: Treatment system performance is monitored and optimized over the plant’s life.

    For plant owners, this often means a water treatment system that performs reliably for decades, even under challenging water conditions.

    How to Evaluate Water Treatment Design

    When reviewing water treatment design, ask:

    Question Why It Matters
    What is the water source and quality? Determines treatment requirements
    What are the treatment goals for each system? Ensures water quality meets end-use requirements
    How is water quality monitored? Detects excursions before damage occurs
    How are chemicals stored and handled? Ensures safety and regulatory compliance
    How are waste streams managed? Ensures environmental compliance
    Is redundancy provided for critical components? Ensures continuous operation
    What is the life-cycle cost? Captures total cost, not just capital

    A water treatment system that addresses these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Water treatment controls corrosion, scaling, fouling, and biological growth
    • Different plant systems have different water quality requirements
    • Cooling water treatment focuses on scaling, corrosion, and biological control
    • Boiler water treatment is more demanding and requires external and internal treatment
    • Demineralized water is essential for high-pressure boilers
    • Japanese EPC firms emphasize thorough water source assessment and conservative design margins

    Conclusion

    Water treatment is a critical but often overlooked aspect of industrial plant design. It affects reliability, efficiency, maintenance cost, and environmental compliance. For small to medium-scale industrial plants, where margins are tight, water treatment deserves careful attention from the earliest stages of design.

    By understanding water quality requirements, selecting appropriate treatment processes, and planning for monitoring, redundancy, and waste management, owners and designers can ensure reliable water quality and long-term plant performance.

  • Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling is one of the most overlooked yet consequential decisions in industrial plant design. Every thermal plant—whether it burns coal, gas, biomass, or waste heat—must reject heat to the environment. How that heat is rejected affects efficiency, water consumption, environmental impact, capital cost, and site selection.

    For small to medium-scale industrial plants, cooling system selection is especially critical because there is less margin for error and fewer resources to manage complex systems. The wrong choice can limit plant output, increase operating cost, or create regulatory problems.

    This article covers the main cooling system options, compares them side by side, and helps you decide which one fits your project.

    Why Cooling Matters

    Thermal plants convert heat into electricity, but not all heat can be converted. A significant portion must be rejected to the environment. This is a fundamental thermodynamic limit—no plant can convert all its heat input into useful work.

    The cooling system’s job is to reject this waste heat efficiently and reliably. The main functions are:

    • Condensing steam: In steam cycles, cooling condenses the exhaust steam from the turbine back into water so it can be reused.
    • Cooling auxiliary equipment: Lubricating oil, generators, and other equipment require cooling.
    • Maintaining vacuum: Efficient condensing requires low pressure, which depends on effective cooling.

    If the cooling system underperforms, the turbine back pressure rises, reducing output and efficiency. In severe cases, the plant must reduce load or shut down.

    The Main Cooling System Options

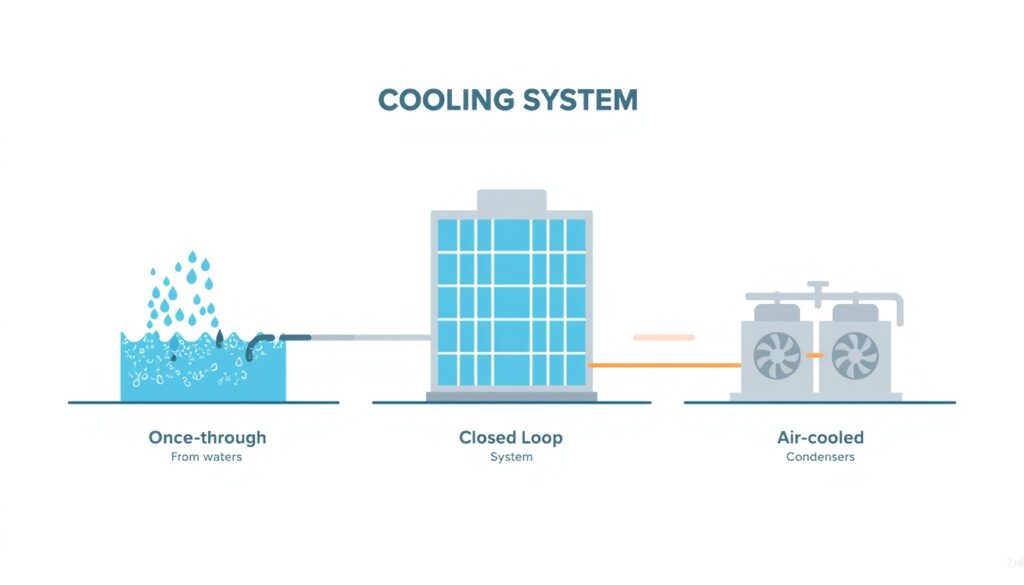
    Comparison of once-through, closed-loop, and air-cooled cooling system types

    Comparison of once-through, closed-loop, and air-cooled cooling system types

    There are three main types of cooling systems for industrial plants:

    1. Once-through cooling
    2. Closed-loop (recirculating) cooling with cooling towers
    3. Air-cooled (dry) cooling

    Each has distinct characteristics, advantages, and drawbacks.

    Once-Through Cooling

    In a once-through system, water is drawn from a nearby source (river, lake, sea), passed through the condenser, and returned to the source at a higher temperature.

    Characteristics:

    • High efficiency: Once-through cooling provides the best cooling performance because water temperature is typically low.
    • Low capital cost: Fewer components, simpler system.
    • High water consumption: Large volumes of water are drawn and returned.
    • Environmental impact: Thermal discharge can affect aquatic ecosystems.
    • Site constraint: Requires a large, reliable water source.

    When it makes sense:

    • Sites with access to abundant cooling water (coastal or large river locations)
    • Regions with lenient thermal discharge regulations
    • Plants where efficiency is the top priority

    Once-through cooling is increasingly restricted in many jurisdictions due to environmental concerns. In the United States, for example, the Clean Water Act Section 316(b) requires that cooling water intake structures minimize environmental impact.

    Closed-Loop Cooling with Cooling Towers

    In a closed-loop system, cooling water is recirculated between the condenser and a cooling tower. The cooling tower rejects heat to the atmosphere, primarily through evaporation.

    Characteristics:

    • Moderate efficiency: Performance depends on ambient wet-bulb temperature. Efficiency is lower than once-through but higher than air-cooled.
    • Moderate capital cost: Cooling towers and circulating water systems add cost.
    • Lower water consumption: Water is lost primarily through evaporation and blowdown, but consumption is much lower than once-through.
    • Visible plume: Cooling towers produce a visible plume of water vapor, which can be a concern in some locations.
    • Chemical treatment: Recirculated water requires treatment to control corrosion, scaling, and biological growth. Closed-loop systems require continuous water treatment to manage these effects; treatment programs typically include corrosion inhibitors, scale inhibitors, and biocides.

    When it makes sense:

    • Sites with limited water availability
    • Regions with strict thermal discharge regulations
    • Plants where a balance between efficiency and water use is needed

    Closed-loop cooling is the most common choice for new industrial plants in many regions. It offers a reasonable compromise between efficiency, water use, and environmental impact.

    Air-Cooled (Dry) Cooling

    In an air-cooled system, heat is rejected directly to the atmosphere using air-cooled condensers or fin-fan coolers. No cooling water is used.

    Characteristics:

    • Lower efficiency: Performance depends on ambient dry-bulb temperature, which is typically higher than wet-bulb temperature. This reduces plant efficiency compared to wet cooling.
    • Higher capital cost: Air-cooled condensers are large and expensive.
    • Zero water consumption: No cooling water is required for heat rejection.
    • Large footprint: Air-cooled systems require significant space.
    • Higher auxiliary power: Fans consume more power than cooling tower fans.

    When it makes sense:

    • Sites with no reliable water source
    • Regions with strict water use restrictions
    • Plants where water availability is uncertain or expensive

    Air-cooled cooling is common in arid regions and in plants where water is scarce or expensive. It eliminates water consumption but at the cost of efficiency and capital cost.

    Side-by-Side Comparison

    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

    Factor Once-Through Closed-Loop (Wet) Air-Cooled (Dry)
    Cooling efficiency Highest Moderate Lowest
    Capital cost Lowest Moderate Highest
    Water consumption Highest Moderate None
    Footprint Small Moderate Large
    Auxiliary power Lowest Moderate Highest
    Environmental impact Thermal discharge Water consumption, plume Land use, noise
    Site requirement Large water source Moderate water source No water source
    Typical use Coastal, large rivers Most inland plants Arid regions

    Hybrid Cooling Systems

    Some plants use hybrid cooling, which combines wet and dry cooling. In a hybrid system, cooling towers operate during cooler periods, while air-cooled condensers take over during peak heat or when water is scarce.

    Advantages:

    • Reduces water consumption compared to pure wet cooling
    • Improves efficiency compared to pure dry cooling
    • Provides flexibility to respond to water availability and ambient conditions

    Disadvantages:

    • Higher capital cost than either pure wet or pure dry
    • More complex operation and maintenance

    Hybrid cooling is often used in regions with seasonal water constraints or where a balance between efficiency and water use is required.

    Key Design Considerations

    1. Ambient Conditions

    Wet-bulb temperature drives wet cooling performance. Dry-bulb temperature drives air-cooled performance. Both vary by location and season. Design must account for the worst-case conditions the plant will face.

    2. Water Availability and Quality

    Water quantity, quality, and cost all affect cooling system selection. Poor water quality may require treatment, which adds cost and complexity.

    3. Environmental Regulations

    Thermal discharge limits, water intake rules, and plume restrictions can all constrain cooling system options. These must be identified early in design.

    4. Plant Size and Load Profile

    Small plants may have different constraints than large ones. A plant that operates only during peak hours may not justify the cost of a complex cooling system.

    5. Parasitic Power

    Cooling system auxiliaries (pumps, fans) consume power, reducing net plant output. This must be accounted for in performance calculations.

    6. Corrosion and Materials

    Cooling water chemistry affects material selection. Once-through systems using seawater require corrosion-resistant materials. Closed-loop systems require water treatment to control scaling and corrosion.

    7. Availability and Redundancy

    For critical plants, consider whether redundancy in cooling system components (pumps, fans, cells) is justified. A single cooling tower cell failure can limit plant output.

    8. Noise Regulations

    Noise from cooling towers and air-cooled condensers can be a constraint in populated areas. Local noise regulations may limit fan speed or require acoustic treatment.

    9. Control and Optimization

    Modern cooling systems use variable frequency drives and advanced controls to match cooling output to plant load and ambient conditions. This reduces auxiliary power consumption at part load.

    Common Mistakes in Cooling System Selection

    Even experienced designers make mistakes. Common ones include:

    • Underestimating water consumption: Especially for wet cooling in water-scarce regions
    • Ignoring ambient extremes: Designing for average conditions rather than worst-case
    • Overlooking regulations: Discovering too late that thermal discharge or intake rules prohibit the chosen system
    • Undersizing cooling towers: Leading to higher back pressure and reduced output
    • Neglecting auxiliary power: Forgetting that fans and pumps reduce net output
    • Poor water treatment: Leading to scaling, corrosion, and reduced performance

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Cooling System Selection

    Japanese engineering firms are known for their disciplined approach to cooling system design. Common characteristics include:

    • Thorough site assessment: Water availability, ambient conditions, and regulations are studied carefully before selection.
    • Conservative design margins: Cooling systems are sized with adequate margin for worst-case conditions.
    • Life-cycle cost focus: Capital cost is evaluated alongside operating cost, water cost, and environmental compliance.
    • Detailed water treatment design: Water chemistry is managed carefully to ensure long-term reliability.
    • Long-term performance monitoring: Cooling system performance is tracked over the plant’s life.

    For plant owners, this often means a cooling system that performs reliably for decades, even under challenging conditions.

    How to Evaluate Cooling System Options

    When reviewing cooling system options, ask:

    Question Why It Matters
    What is the ambient design condition? Determines cooling performance and system size
    Is water available, and at what cost? Affects selection and operating cost
    What are the environmental regulations? Constrains system options
    What is the auxiliary power consumption? Reduces net plant output
    What is the life-cycle cost? Captures total cost, not just capital
    How reliable is the system? Affects plant availability
    How complex is operation and maintenance? Affects staffing and long-term cost

    A cooling system that satisfies all these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Cooling system selection affects efficiency, water use, cost, and environmental impact
    • Once-through: highest efficiency, highest water use
    • Closed-loop: moderate efficiency, moderate water use
    • Air-cooled: lowest efficiency, zero water use
    • Hybrid systems balance wet and dry cooling
    • Japanese EPC firms emphasize thorough site assessment and conservative design margins

    Conclusion

    Cooling system selection is a strategic decision that affects efficiency, water consumption, environmental impact, and cost. Once-through, closed-loop, and air-cooled systems each have distinct advantages and drawbacks. For small to medium-scale industrial plants, the right choice depends on site conditions, water availability, regulations, and financial objectives.

    By evaluating these factors carefully and considering life-cycle cost, owners and designers can select a cooling system that performs reliably and economically for decades.

  • Understanding Heat Rate and Thermal Efficiency in Industrial Plants

    Understanding Heat Rate and Thermal Efficiency in Industrial Plants

    Heat rate is one of the most important performance metrics in thermal power generation. It measures how efficiently a plant converts fuel into electricity. For plant owners, heat rate directly affects operating cost, fuel consumption, and profitability.

    Despite its importance, heat rate is often misunderstood. It is sometimes confused with thermal efficiency, and its relationship to fuel cost is not always clear. This article explains what heat rate is, how it is calculated, what affects it, and why it matters for small to medium-scale industrial plants.

    What Is Heat Rate?

    Heat rate energy input and output illustration

    Heat rate is the amount of energy input required to produce one unit of energy output. In power generation, it is typically expressed in kJ/kWh (kilojoules per kilowatt-hour) or Btu/kWh (British thermal units per kilowatt-hour). To convert between them, 1 kJ/kWh ≈ 0.948 Btu/kWh (equivalently, 1 Btu/kWh ≈ 1.055 kJ/kWh). This article uses kJ/kWh throughout.

    A lower heat rate means better efficiency. A higher heat rate means more fuel is required to produce the same output.

    For example:

    • A plant with a heat rate of 10,000 kJ/kWh requires 10,000 kJ of fuel energy to produce 1 kWh of electricity.
    • A plant with a heat rate of 8,000 kJ/kWh requires only 8,000 kJ of fuel energy to produce the same 1 kWh.

    The second plant is more efficient and will have lower fuel costs for the same output.

    One caution on the fuel side: heat rate can be based on the fuel’s lower heating value (LHV) or higher heating value (HHV). HHV-based figures are higher (worse) than LHV-based figures for the same plant, by roughly 10% for natural gas and less for coal. Always confirm which basis is being used before comparing numbers.

    Heat Rate vs. Thermal Efficiency

    Heat rate and thermal efficiency are related but not identical. Thermal efficiency is the ratio of useful output to energy input, expressed as a percentage.

    The relationship is:

    Thermal Efficiency (%) = 3,600 / Heat Rate (kJ/kWh) × 100 (3,600 kJ = 1 kWh)

    The 3,600 is simply the number of kilojoules in one kilowatt-hour, that is, the energy content of one unit of electrical output. In Btu units, the equivalent constant is 3,412 Btu = 1 kWh.

    For example:

    • Heat rate of 10,000 kJ/kWh → efficiency = 36%
    • Heat rate of 8,000 kJ/kWh → efficiency = 45%
    • Heat rate of 12,000 kJ/kWh → efficiency = 30%

    In simple terms:

    • Lower heat rate = higher efficiency
    • Higher heat rate = lower efficiency

    Both metrics describe the same thing from different angles. Heat rate is preferred in some regions and industries; thermal efficiency is preferred in others.

    Why Heat Rate Matters

    Heat rate matters because fuel is the largest operating cost for most thermal plants. A small improvement in heat rate can translate into significant savings over the plant’s life.

    Consider a plant that consumes fuel at a cost of $5 per million kJ (equivalent to $5/GJ, or roughly $5.3/MMBtu). Fuel prices vary widely by region and over time, so the absolute numbers below are illustrative; substitute your own fuel contract price.

    Heat Rate (kJ/kWh) Fuel Cost per kWh Annual Fuel Cost (100 MW plant, full load, 8,760 h/year)
    12,000 $0.060 $52.6 million
    10,000 $0.050 $43.8 million
    8,000 $0.040 $35.0 million

    The difference between a heat rate of 12,000 and 8,000 is about $17.5 million per year for a 100 MW plant running continuously at full output. For smaller plants, the absolute numbers are lower, but the percentage impact is the same.

    This is why heat rate is often a key performance guarantee in EPC contracts. If the plant does not meet its guaranteed heat rate, the contractor may be liable for liquidated damages.

    For context, guarantee values depend on plant type, size, and the basis used (LHV or HHV, gross or net). For combined cycle plants, guarantees typically range from 6,000 to 7,500 kJ/kWh. For simple cycle plants, 9,000 to 12,000 kJ/kWh is common. Smaller plants tend toward the upper end of these ranges or above them.

    What Affects Heat Rate?

    Many factors influence a plant’s heat rate. Some are design-related, others are operational.

    Design factors:

    • Cycle configuration: Combined cycle plants have lower heat rates than simple cycle plants.
    • Equipment efficiency: Turbine, boiler, and generator efficiency all affect heat rate.
    • Steam conditions: Higher temperature and pressure improve efficiency.
    • Condenser performance: Better vacuum improves efficiency.
    • Auxiliary power consumption: Pumps, fans, and controls consume power, increasing net heat rate.

    Operational factors:

    • Load level: Plants are usually most efficient at or near full load.
    • Ambient conditions: Higher ambient temperature reduces output and increases heat rate.
    • Fuel quality: Lower heating value or impurities can reduce efficiency.
    • Equipment degradation: Fouling, wear, and leaks increase heat rate over time.
    • Operational practices: Startup, shutdown, and part-load operation affect average heat rate.

    For small plants, operational factors often have a larger impact because there is less design margin.

    Gross vs. Net Heat Rate

    Heat rate can be expressed as gross or net.

    • Gross heat rate: Based on total generator output, before subtracting auxiliary power consumption.
    • Net heat rate: Based on net output delivered to the grid, after subtracting auxiliary power.

    Net heat rate is always higher (worse) than gross heat rate because auxiliary equipment consumes power. For plant owners, net heat rate is the more relevant metric because it reflects the actual output available for sale.

    A common mistake is to compare gross heat rates from different plants without adjusting for auxiliary power. Always confirm which basis is being used.

    How Heat Rate Is Measured

    Heat rate is determined through performance testing, typically conducted after commissioning. The test measures:

    • Fuel input: Flow rate and heating value of fuel
    • Power output: Gross and net electrical output
    • Auxiliary power: Consumption of pumps, fans, and other equipment
    • Ambient conditions: Temperature, pressure, and humidity

    International standards such as ASME PTC 46 (overall plant performance) or ISO 2314 (gas turbines) provide procedures for conducting and reporting these tests. The results are used to verify contractual performance guarantees.

    Improving Heat Rate

    Heat rate can be improved through both design and operational measures.

    Design improvements:

    • Higher steam conditions: Supercritical or ultra-supercritical cycles (mainly practical for large utility-scale plants)
    • Combined cycle: Recovering waste heat from exhaust gases
    • Better condensers: Lower condenser pressure improves efficiency
    • Efficient auxiliaries: Variable frequency drives, high-efficiency motors
    • Advanced controls: Optimizing combustion and load allocation

    Operational improvements:

    • Operating at design point: Running at or near full load
    • Regular maintenance: Cleaning heat exchangers, repairing leaks, replacing worn components
    • Fuel management: Using consistent, high-quality fuel
    • Performance monitoring: Tracking heat rate trends to detect degradation
    • Operator training: Ensuring best practices for startup, shutdown, and load changes

    For existing plants, operational improvements often provide the fastest payback. For new plants, design improvements are built in from the start.

    Common Mistakes in Heat Rate Management

    Even experienced operators make mistakes. Common ones include:

    • Ignoring auxiliary power: Focusing on gross heat rate instead of net
    • Comparing at different conditions: Not correcting for ambient temperature or fuel quality
    • Neglecting degradation: Assuming heat rate stays constant over time
    • Operating at part load: Running at low load when full load is possible
    • Skipping performance tests: Not verifying heat rate after major overhauls
    • Poor fuel quality: Using inconsistent or low-quality fuel that increases heat rate

    These mistakes can lead to higher operating costs and missed performance targets.

    How Japanese EPC Firms Approach Heat Rate

    Japanese engineering firms are known for their focus on thermal efficiency. Common characteristics include:

    • Conservative design margins: Equipment is specified with enough margin to maintain performance over time.
    • Detailed performance testing: Heat rate tests are carefully planned and executed.
    • Long-term monitoring: Performance is tracked over the plant’s life, not just at commissioning.
    • Operational support: Japanese firms often provide ongoing support to help owners maintain efficiency.
    • Continuous improvement: Lessons from each project are applied to the next.

    For plant owners, this often means a plant that meets its heat rate guarantee and maintains performance over time.

    How to Evaluate Heat Rate Performance

    When reviewing heat rate performance, ask:

    Question Why It Matters
    Is the heat rate gross or net? Net heat rate reflects actual output for sale
    Is it based on LHV or HHV? The two bases differ by roughly 5–10%, depending on fuel
    What conditions apply? Heat rate varies with ambient temperature and fuel
    Has it been corrected to reference conditions? Allows comparison across different tests
    How has it changed over time? Detects degradation and maintenance needs
    How does it compare to the guarantee? Determines whether the contractor has met obligations
    What is the fuel cost impact? Translates heat rate into financial terms

    A plant that understands its heat rate performance can manage fuel costs, plan maintenance, and verify contractual compliance.

    Conclusion

    Heat rate is a fundamental measure of thermal plant efficiency. It directly affects fuel cost, operating profitability, and contractual performance. For small to medium-scale industrial plants, where margins are tight, understanding and managing heat rate is essential.

    By focusing on design efficiency, operational practices, and continuous monitoring, owners and operators can keep heat rate low and fuel costs under control.

    Key Takeaways

    • Heat rate measures fuel energy input per unit of electricity output.
    • Lower heat rate = higher efficiency.
    • Net heat rate reflects actual output for sale.
    • Heat rate is affected by design, operation, and ambient conditions.
    • Regular monitoring detects degradation and supports maintenance planning.
  • Equipment Selection Criteria for Small to Medium-Scale Industrial Plants

    Equipment Selection Criteria for Small to Medium-Scale Industrial Plants

    Equipment selection is one of the most consequential decisions in plant design. The equipment you choose determines capital cost, operating cost, reliability, maintenance requirements, and ultimately whether the plant meets its performance targets.

    For small to medium-scale industrial plants, equipment selection is especially critical. There is less redundancy, less margin for error, and less room to absorb the consequences of a poor choice. A pump that is oversized wastes energy for decades. A heat exchanger that is undersized limits output from day one.

    This article covers the key criteria that drive effective equipment selection for small to medium-scale plants. Whether you are specifying a boiler, a turbine, a pump, or a control system, these principles apply.

    Why Equipment Selection Matters More for Small Plants

    Large plants often have redundancy built into their designs. If one pump fails, a backup takes over. If one heat exchanger fouls, another compensates. Small plants rarely have this luxury.

    The consequences of poor equipment selection in a small plant include:

    • Higher capital cost: Oversized or over-specified equipment increases upfront investment.
    • Higher operating cost: Inefficient equipment consumes more fuel, power, or chemicals over its life.
    • Reduced reliability: Equipment that is marginal for the application fails more often.
    • Maintenance burden: Equipment that is difficult to service increases downtime and cost.
    • Limited flexibility: Equipment that cannot handle variations in load or feedstock restricts operations.

    For these reasons, equipment selection should be treated as a strategic decision, not a procurement formality.

    The Core Criteria for Equipment Selection

    Core criteria for industrial plant equipment selection

    A good equipment selection process evaluates each item against several criteria simultaneously:

    Criterion What It Means
    Technical suitability Does the equipment meet process requirements?
    Reliability How often does it fail, and how severe are failures?
    Efficiency How much energy, fuel, or consumable does it use?
    Capital cost What is the purchase price, including installation?
    Operating cost What are the ongoing costs of energy, maintenance, and spares?
    Maintainability How easy is it to inspect, repair, and replace?
    Lead time How long until delivery, and does it fit the schedule?
    Vendor support Does the supplier provide spares, service, and technical support?
    Compliance Does it meet codes, standards, and environmental requirements?

    These criteria sometimes conflict. A highly efficient piece of equipment may cost more upfront. A reliable vendor may have a longer lead time. Good selection balances these trade-offs.

    Technical Suitability

    The first question is always: does the equipment meet the process requirements?

    This includes:

    • Capacity: Can it handle the required flow, pressure, temperature, or load?
    • Range: Can it operate across the expected range of conditions?
    • Turndown: Can it operate stably and efficiently down to the minimum expected load?
    • Compatibility: Is it compatible with the process fluid, fuel, or environment?
    • Interfaces: Does it connect properly with upstream and downstream equipment?

    Manufacturers provide performance curves and datasheets that define these limits. These should be reviewed carefully, not assumed.

    A common mistake is selecting equipment that meets design conditions but performs poorly at off-design conditions. For small plants, which often operate across a wide range of loads, turndown and part-load efficiency are especially important.

    Equipment selection also directly affects whether the plant can meet its performance guarantees. If the plant must achieve a guaranteed heat rate or output, every major item must be capable of supporting it. A pump or heat exchanger that is marginal at design conditions may cause the entire plant to fall short. (See [title/link of article on performance guarantees].)

    Standardization vs. Customization

    For small plants, standard, off-the-shelf equipment is usually preferable to custom-designed units. Catalogue equipment typically costs less, is delivered faster, has a proven field record, and uses spare parts that are easier to source and interchange. Standardizing on the same models across the plant, such as a single pump family, also reduces the number of different spares to hold and simplifies operator training.

    Customization is justified when standard equipment cannot meet a process requirement or offers a clear performance advantage. Even then, its added cost, longer lead time, and heavier spares burden should be weighed explicitly rather than accepted by default.

    Reliability

    Reliability is the probability that equipment will perform its function without failure over a given period. For small plants, reliability is critical because there is often no redundancy.

    Key reliability considerations include:

    • Mean time between failures (MTBF): How often does the equipment fail?
    • Mean time to repair (MTTR): How long does it take to restore operation after a failure?
    • Failure mode: Does failure result in a safe shutdown or a hazardous condition?
    • Service history: How has this equipment performed in similar applications?

    Reliability data can come from manufacturer records, industry databases, or references from other plant owners. Do not rely solely on vendor claims.

    For critical equipment, consider whether redundancy is justified. A single spare pump may cost less than the production lost during a failure.

    Efficiency

    Efficiency determines how much energy or fuel the equipment consumes over its life. For equipment that runs continuously, efficiency often matters more than capital cost.

    Consider a pump, for example. Suppose it draws 100 kW and runs 8,000 hours per year at an electricity price of $0.10/kWh. Its annual energy cost is about $80,000. A pump that draws 5% less power saves about $4,000 per year, or roughly $40,000 over 10 years. If the more efficient pump carries a 20% price premium on a typical $20,000 unit, that premium is only $4,000, so it pays for itself in about one year. Even after discounting future savings (about $27,000 at an 8% discount rate), the energy savings far exceed the price difference.

    The same logic applies to boilers, turbines, compressors, and heat exchangers. The key is to evaluate life-cycle cost, not just purchase price.

    Capital Cost vs. Operating Cost

    Capital cost versus operating cost trade-off in equipment selection

    Equipment selection often involves a trade-off between capital cost and operating cost. A cheaper piece of equipment may consume more energy, require more maintenance, or fail more often.

    The tool for evaluating this trade-off is life-cycle cost analysis, also known as total cost of ownership (TCO) analysis. This sums:

    • Purchase price
    • Installation cost
    • Energy cost over the equipment’s life
    • Maintenance and spares cost
    • Downtime cost
    • Disposal or replacement cost

    For small plants, where margins are tight, life-cycle cost (TCO) is often the most important criterion. A slightly higher upfront investment in efficient, reliable equipment usually pays back many times over.

    Maintainability

    Maintainability considerations in industrial plant equipment selection

    Equipment must be maintainable. This means:

    • Access: Can it be reached for inspection and repair?
    • Disassembly: Can components be removed and replaced without major work?
    • Standardization: Are parts standard, or are they proprietary and slow to source?
    • Documentation: Are manuals, drawings, and procedures available?
    • Training: Can your team operate and maintain it, or is specialist support required?

    For small plants, maintainability is often overlooked. Equipment that is difficult to service leads to longer downtime, higher costs, and more reliance on external support.

    Lead Time and Schedule

    Lead time is the time between placing an order and receiving the equipment. For long-lead items such as turbines, generators, and large vessels, lead times can be 12 to 24 months or more.

    Lead time affects:

    • Project schedule: Long-lead items determine the critical path.
    • Procurement planning: Orders must be placed early enough to meet schedule.
    • Storage and preservation: Equipment delivered early must be stored and protected.
    • Vendor capacity: Popular vendors may be booked out for months.

    For small plants, lead time is often a constraint. Early identification of long-lead items allows procurement to start as soon as the design is firm.

    Vendor Support

    The equipment vendor is a partner for the life of the plant. Good vendor support includes:

    • Spare parts availability: Can parts be sourced quickly?
    • Technical support: Is help available when problems arise?
    • Warranty: What is covered, and for how long?
    • Service agreements: Are maintenance and overhaul services available?
    • Training: Does the vendor provide training for your team?

    A vendor with strong support may be worth a higher price. A vendor with poor support can leave you stranded when equipment fails.

    Spare Parts Strategy

    Availability from the vendor is only half the question. The other half is what to hold on site. For critical equipment, consider whether to stock spare parts on-site or rely on vendor delivery. Remote plants often justify carrying key spares, because a single missing part can idle the plant for weeks. A practical approach is to ask each vendor for a recommended spares list, then stock the items that are critical to operation, have long lead times, or are unlikely to be available locally. Weigh the carrying cost of these spares against the cost of downtime.

    Compliance and Standards

    Equipment must comply with applicable codes, standards, and regulations. These may include:

    • Pressure vessel codes: ASME, PED, or local equivalents
    • Electrical standards: IEC, NEC, or local equivalents
    • Environmental regulations: Emissions limits, noise limits, and discharge requirements
    • Safety standards: ATEX, NFPA, or local equivalents

    Compliance is not optional. Equipment that does not meet applicable standards cannot be legally operated, and may not be insurable.

    Common Equipment Selection Mistakes

    Even experienced designers make mistakes. Common ones include:

    • Selecting on price alone: Ignoring efficiency, reliability, and maintenance costs
    • Oversizing equipment: Adding unnecessary margin that increases cost and reduces efficiency
    • Undersizing equipment: Leaving no margin for actual operating conditions
    • Ignoring part-load performance: Optimizing for design point only
    • Overlooking lead time: Discovering too late that equipment cannot be delivered on schedule
    • Neglecting vendor support: Choosing a vendor with no local presence or spare parts
    • Skipping life-cycle cost analysis: Comparing only purchase prices

    These mistakes are costly to fix after equipment is installed. They are much cheaper to avoid during selection.

    How Japanese EPC Firms Approach Equipment Selection

    Japanese engineering firms are known for their disciplined approach to equipment selection. Common characteristics include:

    • Conservative sizing: Equipment is specified with adequate margin, but not excessive.
    • Emphasis on reliability: Proven equipment and vendors are preferred over untested alternatives.
    • Life-cycle cost focus: Purchase price is evaluated alongside operating and maintenance costs.
    • Long-term vendor relationships: Established vendors with strong support are favored.
    • Detailed documentation: Specifications, datasheets, and test records are carefully maintained.

    For plant owners, this often means equipment that performs reliably for decades, even if the initial price is higher than some alternatives.

    How to Evaluate Equipment Selection

    When reviewing equipment selections, ask:

    Question Why It Matters
    Does it meet process requirements? Ensures the plant can achieve its design output
    Can it support the performance guarantees? Prevents a marginal item from causing the plant to fall short
    Is it reliable? Reduces downtime and maintenance cost
    Is it efficient? Reduces operating cost over the plant’s life
    What is the life-cycle cost (TCO)? Captures total cost, not just purchase price
    Is it maintainable? Reduces downtime and reliance on external support
    Can it be delivered on schedule? Keeps the project on track
    Does the vendor provide good support, and are critical spares covered? Ensures spare parts and technical help are available
    Does it comply with standards? Ensures legal and safe operation

    A selection that satisfies all these questions is likely to perform well over the plant’s life.

    Conclusion

    Equipment selection is not just a procurement exercise. It is a strategic decision that affects cost, reliability, efficiency, and long-term performance. For small to medium-scale industrial plants, where margins are tight and redundancy is limited, equipment selection deserves careful attention from the earliest stages of design.

    By focusing on technical suitability, reliability, efficiency, life-cycle cost, maintainability, lead time, vendor support, and compliance, owners and designers can select equipment that performs reliably and economically for decades.

    Key Takeaways

    • Equipment selection affects cost, reliability, efficiency, and long-term performance.
    • Life-cycle cost (total cost of ownership), not just purchase price, should drive decisions.
    • Reliability and maintainability matter more in small plants with limited redundancy.
    • Standard, proven equipment and a sensible on-site spares strategy reduce cost, lead time, and downtime.
    • Lead time and vendor support are critical for schedule and long-term operation.
    • Japanese EPC firms favor conservative sizing, proven vendors, and detailed documentation.
  • Key Considerations in Small-Scale Industrial Plant Layout Design

    Key Considerations in Small-Scale Industrial Plant Layout Design

    Plant layout is one of the most consequential decisions in industrial plant design. It affects construction cost, operating efficiency, maintenance access, safety, and future expansion. For small-scale industrial plants, layout decisions are especially critical because there is less space to work with and less margin for error.

    This article covers the key considerations that drive effective layout design for small to medium-scale industrial plants. Whether you are planning a biomass facility, a small thermal plant, or a process plant, these principles apply.

    Plot Plan vs. Equipment Layout

    Two related but distinct documents define a plant’s layout:

    • Plot plan: The site-level arrangement of buildings, roads, major equipment, tanks, utilities, and boundaries.
    • Equipment layout: The detailed arrangement of equipment, piping, and access within a building, structure, or process area.

    For small plants, the plot plan often determines whether the project is feasible at all. Site boundaries, setbacks, access roads, and separation distances are fixed early, and they constrain everything that follows. This article addresses both levels, but the plot plan should be settled before detailed equipment layout begins.

    Why Layout Matters More for Small Plants

    Large plants often have enough space to accommodate imperfect layouts. Small plants do not. Every meter counts. A poorly planned layout in a small plant can lead to:

    • Higher construction cost: Extra piping, longer cable runs, and additional structural steel.
    • Inefficient operations: Longer travel distances for operators and maintenance staff.
    • Safety risks: Inadequate separation between hazardous areas.
    • Limited expansion: No room to add equipment or capacity later.
    • Maintenance difficulties: Equipment that cannot be accessed for service.

    For these reasons, layout should be treated as a strategic decision, not a drafting exercise.

    The Core Objectives of Plant Layout

    Core objectives of industrial plant layout design

    A good layout achieves several objectives simultaneously:

    Objective What It Means
    Minimize capital cost Reduce piping, cabling, and structural requirements
    Optimize operations Place equipment in logical process order
    Ensure safety Separate hazardous areas and provide clear escape routes
    Enable maintenance Provide access for inspection, repair, and replacement
    Allow expansion Reserve space for future equipment or capacity increase
    Facilitate construction Allow efficient sequencing of civil, mechanical, and electrical work

    These objectives sometimes conflict. For example, minimizing cost may push equipment closer together, but safety and maintenance requirements may demand more space. Good layout design balances these trade-offs.

    Key Considerations

    1. Process Flow

    Process flow diagram for industrial plant layout design

    The layout should follow the process flow as closely as possible. Raw material should enter at one end, and finished product or output should exit at the other. This minimizes piping runs, reduces pressure drops, and simplifies operation.

    For small plants, a linear or L-shaped layout often works best. Linear layouts minimize piping runs and simplify construction, while L-shaped layouts allow the plant to fit into constrained sites while preserving process flow. Both are simple, efficient, and easy to expand.

    2. Equipment Spacing

    Equipment must be spaced to allow:

    • Operation: Space for operators to monitor and adjust equipment.
    • Maintenance: Room to remove and replace components such as heat exchangers, pumps, and motors.
    • Safety: Adequate distance between hot surfaces, electrical equipment, and flammable materials.
    • Ventilation: Airflow to prevent heat buildup and gas accumulation.

    Manufacturers typically provide minimum clearance recommendations. These should be treated as minimums, not targets.

    3. Piping, Pipe Racks, and Cable Routing

    Piping and cabling are significant cost drivers. A layout that minimizes the length and complexity of these runs reduces both capital cost and pressure losses.

    Key principles:

    • Group equipment that shares piping or cabling connections.
    • Use common pipe racks and cable trays where possible.
    • Avoid unnecessary elevation changes in piping.
    • Route cables away from hot or hazardous areas.

    Pipe racks as the backbone of the layout. In many plants, the pipe rack is the organizing element around which everything else is arranged. Its location drives equipment spacing, since equipment is typically placed along both sides of the rack. It also drives construction sequence, because rack foundations and steel are often erected early so that piping and cable trays can be installed as equipment arrives. Deciding rack location and routing early, ideally alongside the plot plan, avoids expensive rework later. Leave spare capacity on the rack for future lines, and keep power and instrument cable trays segregated from process piping according to applicable standards.

    4. Access and Egress

    Safe access is essential. The layout must provide:

    • Primary access routes: For normal operations and maintenance.
    • Emergency egress routes: For evacuation during an incident.
    • Vehicle access: For deliveries, mobile equipment, and emergency response.
    • Pedestrian access: Separate from vehicle routes where possible.

    In small plants, access routes often do double duty. This requires careful planning to avoid conflicts.

    5. Safety, Hazard Separation, and Regulatory Compliance

    Safety should be a primary driver of layout, not an afterthought. Key considerations include:

    • Separation distances: Between hazardous and non-hazardous areas.
    • Fire zones: Segregation of equipment by fire risk.
    • Explosion protection: Location of electrical equipment relative to flammable areas.
    • Toxic gas dispersion: Placement of vents and stacks relative to occupied areas.
    • Emergency shutdown: Access to isolation valves and controls.

    Recognized codes and standards (such as NFPA, IEC, and API) provide guidance on separation distances. These must be respected.

    Regulatory compliance. Local regulations often dictate separation distances, fire zone requirements, and emergency access routes. These must be identified early, as they can constrain the layout significantly. A layout that is efficient on paper but fails a permit review can force a costly redesign.

    6. Maintenance and Replacement

    Equipment must be accessible for maintenance. The layout should allow:

    • Removal of major components: Heat exchanger tubes, turbine rotors, and pump internals.
    • Lifting access: Overhead clearance for cranes or mobile lifting equipment.
    • Workspace: Room for maintenance personnel and tools.
    • Spare parts storage: Nearby but not blocking access.

    For small plants, maintenance access is often compromised by tight layout. This should be addressed early in design, not discovered during operation.

    Operation vs. maintenance. Layout for operation and layout for maintenance sometimes conflict. A compact layout may be efficient for operations but difficult for maintenance. The trade-off should be evaluated explicitly.

    7. Future Expansion

    Even small plants sometimes need to expand. A good layout reserves space for:

    • Additional equipment: Parallel process lines, additional pumps, or extra capacity.
    • Utility upgrades: Larger transformers, additional cooling capacity.
    • Control system expansion: Space for additional panels or instruments.
    • Site infrastructure: Roads, parking, and storage.

    Expansion space should be identified during initial design, even if expansion is not certain.

    8. Construction Sequence

    Layout affects how the plant is built. A layout that allows efficient construction sequencing can reduce schedule and cost. Key considerations include:

    • Access for construction equipment: Cranes, trucks, and heavy lift equipment.
    • Laydown areas: Space for temporary storage of materials and equipment.
    • Sequencing: Ability to install equipment in a logical order without blocking access.
    • Temporary facilities: Site offices, warehouses, and worker facilities.

    For small plants, construction access is often constrained. Early planning helps avoid delays.

    9. 3D Modeling and Clash Detection

    Modern layout design uses 3D modeling to detect clashes between piping, structural, and electrical systems before construction begins. This reduces field changes and rework. In tight small-plant layouts, where piping, steel, cable trays, and maintenance envelopes compete for the same space, clash detection is especially valuable. The 3D model can also be used to check maintenance access and lifting paths, not just physical interferences.

    Common Layout Mistakes

    Even experienced designers make mistakes. Common ones include:

    • Insufficient maintenance access: Equipment installed too close to walls or other equipment.
    • Ignoring expansion: No space reserved for future needs.
    • Poor process flow: Equipment arranged inefficiently, increasing piping and operating cost.
    • Inadequate safety separation: Hazardous areas too close to occupied areas.
    • Overlooking construction access: Equipment that cannot be delivered or installed.
    • Forgetting utilities: Insufficient space for piping, cabling, and instrumentation.

    These mistakes are costly to fix after construction begins. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Layout

    Japanese engineering firms often take a disciplined approach to plant layout. Common characteristics include:

    • Thorough front-end planning: Layout is developed early and refined through multiple reviews.
    • Attention to detail: Clearances, access routes, and maintenance space are carefully considered.
    • Safety focus: Hazard separation and emergency access are prioritized.
    • Long-term perspective: Expansion space is reserved even when not immediately needed.
    • Constructability review: Layout is evaluated for ease of construction, not just operation.

    For plant owners, this often means a layout that is efficient, safe, and adaptable to future needs.

    How to Evaluate a Layout

    When reviewing a proposed layout, ask:

    Question Why It Matters
    Does it follow the process flow? Minimizes piping and operating cost
    Is there adequate maintenance access? Reduces downtime and maintenance cost
    Are safety separations respected? Protects people and assets
    Is there space for expansion? Avoids costly future modifications
    Can it be constructed efficiently? Reduces schedule and cost
    Are utilities properly routed? Avoids conflicts and inefficiencies
    Is it compliant with regulations? Ensures legal and safe operation

    A layout that satisfies all these questions is likely to perform well over the plant’s life.

    Conclusion

    Plant layout is not just a drawing exercise. It is a strategic decision that affects cost, safety, operations, and future flexibility. For small-scale industrial plants, where space is limited and margins are tight, layout deserves careful attention from the earliest stages of design.

    By focusing on process flow, equipment spacing, safety, maintenance access, and expansion, owners and designers can create layouts that are efficient, safe, and built to last.

    Key Takeaways

    • Plant layout affects cost, safety, operations, and future flexibility.
    • The plot plan often determines project feasibility, so settle it before detailed equipment layout.
    • Process flow should drive the overall arrangement.
    • Equipment spacing must allow operation, maintenance, and safety.
    • Access and egress must be planned for normal and emergency conditions.
    • Local regulations should be identified early, since they can constrain the layout significantly.
    • 3D modeling and clash detection reduce field changes and rework.
    • Japanese EPC firms emphasize front-end planning and constructability review.