Tag: Plant Owner Guide

  • Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling Systems for Industrial Plants: Options and Trade-Offs

    Cooling is one of the most overlooked yet consequential decisions in industrial plant design. Every thermal plant—whether it burns coal, gas, biomass, or waste heat—must reject heat to the environment. How that heat is rejected affects efficiency, water consumption, environmental impact, capital cost, and site selection.

    For small to medium-scale industrial plants, cooling system selection is especially critical because there is less margin for error and fewer resources to manage complex systems. The wrong choice can limit plant output, increase operating cost, or create regulatory problems.

    This article covers the main cooling system options, compares them side by side, and helps you decide which one fits your project.

    Why Cooling Matters

    Thermal plants convert heat into electricity, but not all heat can be converted. A significant portion must be rejected to the environment. This is a fundamental thermodynamic limit—no plant can convert all its heat input into useful work.

    The cooling system’s job is to reject this waste heat efficiently and reliably. The main functions are:

    • Condensing steam: In steam cycles, cooling condenses the exhaust steam from the turbine back into water so it can be reused.
    • Cooling auxiliary equipment: Lubricating oil, generators, and other equipment require cooling.
    • Maintaining vacuum: Efficient condensing requires low pressure, which depends on effective cooling.

    If the cooling system underperforms, the turbine back pressure rises, reducing output and efficiency. In severe cases, the plant must reduce load or shut down.

    The Main Cooling System Options
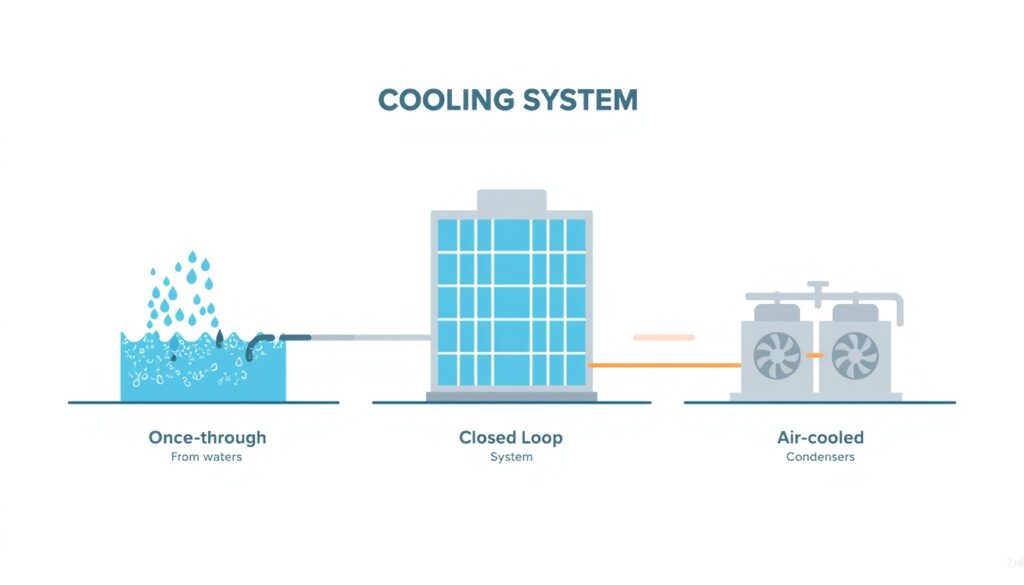
    Comparison of once-through, closed-loop, and air-cooled cooling system types

    Comparison of once-through, closed-loop, and air-cooled cooling system types

    There are three main types of cooling systems for industrial plants:

    1. Once-through cooling
    2. Closed-loop (recirculating) cooling with cooling towers
    3. Air-cooled (dry) cooling

    Each has distinct characteristics, advantages, and drawbacks.

    Once-Through Cooling

    In a once-through system, water is drawn from a nearby source (river, lake, sea), passed through the condenser, and returned to the source at a higher temperature.

    Characteristics:

    • High efficiency: Once-through cooling provides the best cooling performance because water temperature is typically low.
    • Low capital cost: Fewer components, simpler system.
    • High water consumption: Large volumes of water are drawn and returned.
    • Environmental impact: Thermal discharge can affect aquatic ecosystems.
    • Site constraint: Requires a large, reliable water source.

    When it makes sense:

    • Sites with access to abundant cooling water (coastal or large river locations)
    • Regions with lenient thermal discharge regulations
    • Plants where efficiency is the top priority

    Once-through cooling is increasingly restricted in many jurisdictions due to environmental concerns. In the United States, for example, the Clean Water Act Section 316(b) requires that cooling water intake structures minimize environmental impact.

    Closed-Loop Cooling with Cooling Towers

    In a closed-loop system, cooling water is recirculated between the condenser and a cooling tower. The cooling tower rejects heat to the atmosphere, primarily through evaporation.

    Characteristics:

    • Moderate efficiency: Performance depends on ambient wet-bulb temperature. Efficiency is lower than once-through but higher than air-cooled.
    • Moderate capital cost: Cooling towers and circulating water systems add cost.
    • Lower water consumption: Water is lost primarily through evaporation and blowdown, but consumption is much lower than once-through.
    • Visible plume: Cooling towers produce a visible plume of water vapor, which can be a concern in some locations.
    • Chemical treatment: Recirculated water requires treatment to control corrosion, scaling, and biological growth. Closed-loop systems require continuous water treatment to manage these effects; treatment programs typically include corrosion inhibitors, scale inhibitors, and biocides.

    When it makes sense:

    • Sites with limited water availability
    • Regions with strict thermal discharge regulations
    • Plants where a balance between efficiency and water use is needed

    Closed-loop cooling is the most common choice for new industrial plants in many regions. It offers a reasonable compromise between efficiency, water use, and environmental impact.

    Air-Cooled (Dry) Cooling

    In an air-cooled system, heat is rejected directly to the atmosphere using air-cooled condensers or fin-fan coolers. No cooling water is used.

    Characteristics:

    • Lower efficiency: Performance depends on ambient dry-bulb temperature, which is typically higher than wet-bulb temperature. This reduces plant efficiency compared to wet cooling.
    • Higher capital cost: Air-cooled condensers are large and expensive.
    • Zero water consumption: No cooling water is required for heat rejection.
    • Large footprint: Air-cooled systems require significant space.
    • Higher auxiliary power: Fans consume more power than cooling tower fans.

    When it makes sense:

    • Sites with no reliable water source
    • Regions with strict water use restrictions
    • Plants where water availability is uncertain or expensive

    Air-cooled cooling is common in arid regions and in plants where water is scarce or expensive. It eliminates water consumption but at the cost of efficiency and capital cost.

    Side-by-Side Comparison
    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

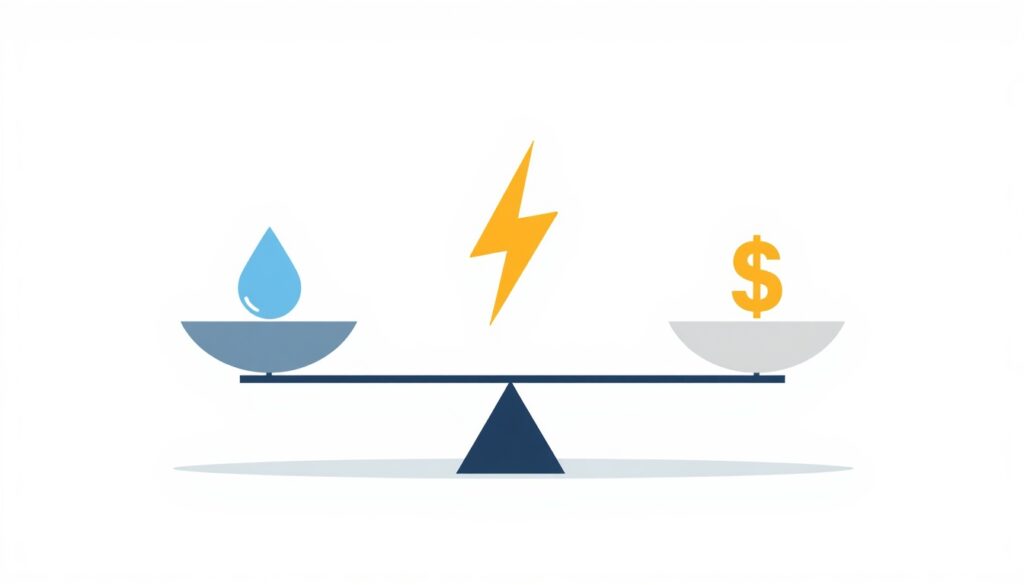
    Trade-offs between water consumption, efficiency, and capital cost in cooling systems

    Factor Once-Through Closed-Loop (Wet) Air-Cooled (Dry)
    Cooling efficiency Highest Moderate Lowest
    Capital cost Lowest Moderate Highest
    Water consumption Highest Moderate None
    Footprint Small Moderate Large
    Auxiliary power Lowest Moderate Highest
    Environmental impact Thermal discharge Water consumption, plume Land use, noise
    Site requirement Large water source Moderate water source No water source
    Typical use Coastal, large rivers Most inland plants Arid regions

    Hybrid Cooling Systems

    Some plants use hybrid cooling, which combines wet and dry cooling. In a hybrid system, cooling towers operate during cooler periods, while air-cooled condensers take over during peak heat or when water is scarce.

    Advantages:

    • Reduces water consumption compared to pure wet cooling
    • Improves efficiency compared to pure dry cooling
    • Provides flexibility to respond to water availability and ambient conditions

    Disadvantages:

    • Higher capital cost than either pure wet or pure dry
    • More complex operation and maintenance

    Hybrid cooling is often used in regions with seasonal water constraints or where a balance between efficiency and water use is required.

    Key Design Considerations

    1. Ambient Conditions

    Wet-bulb temperature drives wet cooling performance. Dry-bulb temperature drives air-cooled performance. Both vary by location and season. Design must account for the worst-case conditions the plant will face.

    2. Water Availability and Quality

    Water quantity, quality, and cost all affect cooling system selection. Poor water quality may require treatment, which adds cost and complexity.

    3. Environmental Regulations

    Thermal discharge limits, water intake rules, and plume restrictions can all constrain cooling system options. These must be identified early in design.

    4. Plant Size and Load Profile

    Small plants may have different constraints than large ones. A plant that operates only during peak hours may not justify the cost of a complex cooling system.

    5. Parasitic Power

    Cooling system auxiliaries (pumps, fans) consume power, reducing net plant output. This must be accounted for in performance calculations.

    6. Corrosion and Materials

    Cooling water chemistry affects material selection. Once-through systems using seawater require corrosion-resistant materials. Closed-loop systems require water treatment to control scaling and corrosion.

    7. Availability and Redundancy

    For critical plants, consider whether redundancy in cooling system components (pumps, fans, cells) is justified. A single cooling tower cell failure can limit plant output.

    8. Noise Regulations

    Noise from cooling towers and air-cooled condensers can be a constraint in populated areas. Local noise regulations may limit fan speed or require acoustic treatment.

    9. Control and Optimization

    Modern cooling systems use variable frequency drives and advanced controls to match cooling output to plant load and ambient conditions. This reduces auxiliary power consumption at part load.

    Common Mistakes in Cooling System Selection

    Even experienced designers make mistakes. Common ones include:

    • Underestimating water consumption: Especially for wet cooling in water-scarce regions
    • Ignoring ambient extremes: Designing for average conditions rather than worst-case
    • Overlooking regulations: Discovering too late that thermal discharge or intake rules prohibit the chosen system
    • Undersizing cooling towers: Leading to higher back pressure and reduced output
    • Neglecting auxiliary power: Forgetting that fans and pumps reduce net output
    • Poor water treatment: Leading to scaling, corrosion, and reduced performance

    These mistakes are costly to fix after construction. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Cooling System Selection

    Japanese engineering firms are known for their disciplined approach to cooling system design. Common characteristics include:

    • Thorough site assessment: Water availability, ambient conditions, and regulations are studied carefully before selection.
    • Conservative design margins: Cooling systems are sized with adequate margin for worst-case conditions.
    • Life-cycle cost focus: Capital cost is evaluated alongside operating cost, water cost, and environmental compliance.
    • Detailed water treatment design: Water chemistry is managed carefully to ensure long-term reliability.
    • Long-term performance monitoring: Cooling system performance is tracked over the plant’s life.

    For plant owners, this often means a cooling system that performs reliably for decades, even under challenging conditions.

    How to Evaluate Cooling System Options

    When reviewing cooling system options, ask:

    Question Why It Matters
    What is the ambient design condition? Determines cooling performance and system size
    Is water available, and at what cost? Affects selection and operating cost
    What are the environmental regulations? Constrains system options
    What is the auxiliary power consumption? Reduces net plant output
    What is the life-cycle cost? Captures total cost, not just capital
    How reliable is the system? Affects plant availability
    How complex is operation and maintenance? Affects staffing and long-term cost

    A cooling system that satisfies all these questions is likely to perform well over the plant’s life.

    Key Takeaways

    • Cooling system selection affects efficiency, water use, cost, and environmental impact
    • Once-through: highest efficiency, highest water use
    • Closed-loop: moderate efficiency, moderate water use
    • Air-cooled: lowest efficiency, zero water use
    • Hybrid systems balance wet and dry cooling
    • Japanese EPC firms emphasize thorough site assessment and conservative design margins

    Conclusion

    Cooling system selection is a strategic decision that affects efficiency, water consumption, environmental impact, and cost. Once-through, closed-loop, and air-cooled systems each have distinct advantages and drawbacks. For small to medium-scale industrial plants, the right choice depends on site conditions, water availability, regulations, and financial objectives.

    By evaluating these factors carefully and considering life-cycle cost, owners and designers can select a cooling system that performs reliably and economically for decades.
  • Equipment Selection Criteria for Small to Medium-Scale Industrial Plants

    Equipment Selection Criteria for Small to Medium-Scale Industrial Plants

    Equipment selection is one of the most consequential decisions in plant design. The equipment you choose determines capital cost, operating cost, reliability, maintenance requirements, and ultimately whether the plant meets its performance targets.

    For small to medium-scale industrial plants, equipment selection is especially critical. There is less redundancy, less margin for error, and less room to absorb the consequences of a poor choice. A pump that is oversized wastes energy for decades. A heat exchanger that is undersized limits output from day one.

    This article covers the key criteria that drive effective equipment selection for small to medium-scale plants. Whether you are specifying a boiler, a turbine, a pump, or a control system, these principles apply.

    Why Equipment Selection Matters More for Small Plants

    Large plants often have redundancy built into their designs. If one pump fails, a backup takes over. If one heat exchanger fouls, another compensates. Small plants rarely have this luxury.

    The consequences of poor equipment selection in a small plant include:

    • Higher capital cost: Oversized or over-specified equipment increases upfront investment.
    • Higher operating cost: Inefficient equipment consumes more fuel, power, or chemicals over its life.
    • Reduced reliability: Equipment that is marginal for the application fails more often.
    • Maintenance burden: Equipment that is difficult to service increases downtime and cost.
    • Limited flexibility: Equipment that cannot handle variations in load or feedstock restricts operations.

    For these reasons, equipment selection should be treated as a strategic decision, not a procurement formality.

    The Core Criteria for Equipment Selection

    Core criteria for industrial plant equipment selection

    A good equipment selection process evaluates each item against several criteria simultaneously:

    Criterion What It Means
    Technical suitability Does the equipment meet process requirements?
    Reliability How often does it fail, and how severe are failures?
    Efficiency How much energy, fuel, or consumable does it use?
    Capital cost What is the purchase price, including installation?
    Operating cost What are the ongoing costs of energy, maintenance, and spares?
    Maintainability How easy is it to inspect, repair, and replace?
    Lead time How long until delivery, and does it fit the schedule?
    Vendor support Does the supplier provide spares, service, and technical support?
    Compliance Does it meet codes, standards, and environmental requirements?

    These criteria sometimes conflict. A highly efficient piece of equipment may cost more upfront. A reliable vendor may have a longer lead time. Good selection balances these trade-offs.

    Technical Suitability

    The first question is always: does the equipment meet the process requirements?

    This includes:

    • Capacity: Can it handle the required flow, pressure, temperature, or load?
    • Range: Can it operate across the expected range of conditions?
    • Turndown: Can it operate stably and efficiently down to the minimum expected load?
    • Compatibility: Is it compatible with the process fluid, fuel, or environment?
    • Interfaces: Does it connect properly with upstream and downstream equipment?

    Manufacturers provide performance curves and datasheets that define these limits. These should be reviewed carefully, not assumed.

    A common mistake is selecting equipment that meets design conditions but performs poorly at off-design conditions. For small plants, which often operate across a wide range of loads, turndown and part-load efficiency are especially important.

    Equipment selection also directly affects whether the plant can meet its performance guarantees. If the plant must achieve a guaranteed heat rate or output, every major item must be capable of supporting it. A pump or heat exchanger that is marginal at design conditions may cause the entire plant to fall short. (See [title/link of article on performance guarantees].)

    Standardization vs. Customization

    For small plants, standard, off-the-shelf equipment is usually preferable to custom-designed units. Catalogue equipment typically costs less, is delivered faster, has a proven field record, and uses spare parts that are easier to source and interchange. Standardizing on the same models across the plant, such as a single pump family, also reduces the number of different spares to hold and simplifies operator training.

    Customization is justified when standard equipment cannot meet a process requirement or offers a clear performance advantage. Even then, its added cost, longer lead time, and heavier spares burden should be weighed explicitly rather than accepted by default.

    Reliability

    Reliability is the probability that equipment will perform its function without failure over a given period. For small plants, reliability is critical because there is often no redundancy.

    Key reliability considerations include:

    • Mean time between failures (MTBF): How often does the equipment fail?
    • Mean time to repair (MTTR): How long does it take to restore operation after a failure?
    • Failure mode: Does failure result in a safe shutdown or a hazardous condition?
    • Service history: How has this equipment performed in similar applications?

    Reliability data can come from manufacturer records, industry databases, or references from other plant owners. Do not rely solely on vendor claims.

    For critical equipment, consider whether redundancy is justified. A single spare pump may cost less than the production lost during a failure.

    Efficiency

    Efficiency determines how much energy or fuel the equipment consumes over its life. For equipment that runs continuously, efficiency often matters more than capital cost.

    Consider a pump, for example. Suppose it draws 100 kW and runs 8,000 hours per year at an electricity price of $0.10/kWh. Its annual energy cost is about $80,000. A pump that draws 5% less power saves about $4,000 per year, or roughly $40,000 over 10 years. If the more efficient pump carries a 20% price premium on a typical $20,000 unit, that premium is only $4,000, so it pays for itself in about one year. Even after discounting future savings (about $27,000 at an 8% discount rate), the energy savings far exceed the price difference.

    The same logic applies to boilers, turbines, compressors, and heat exchangers. The key is to evaluate life-cycle cost, not just purchase price.

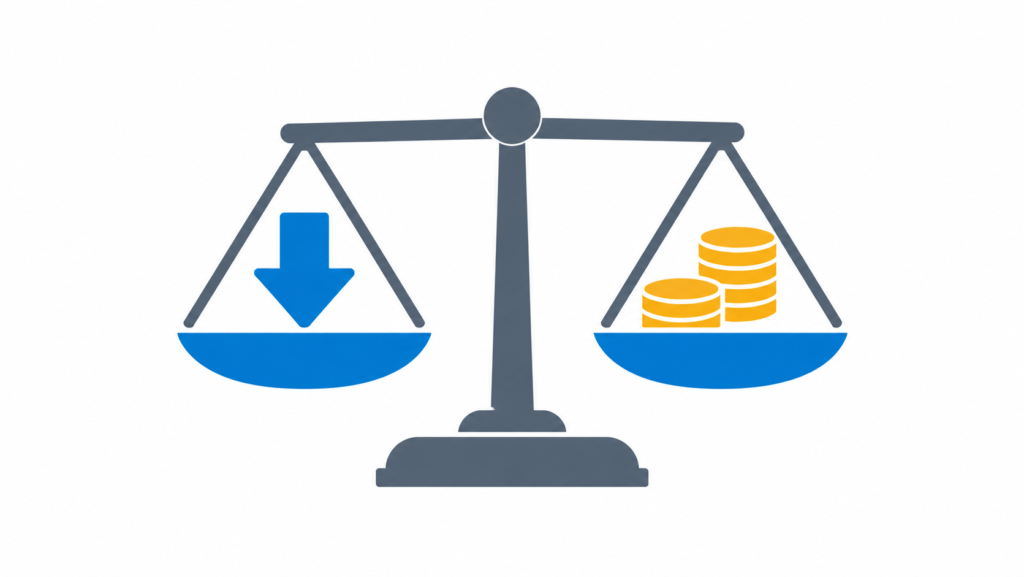
    Capital Cost vs. Operating Cost

    Capital cost versus operating cost trade-off in equipment selection

    Equipment selection often involves a trade-off between capital cost and operating cost. A cheaper piece of equipment may consume more energy, require more maintenance, or fail more often.

    The tool for evaluating this trade-off is life-cycle cost analysis, also known as total cost of ownership (TCO) analysis. This sums:

    • Purchase price
    • Installation cost
    • Energy cost over the equipment’s life
    • Maintenance and spares cost
    • Downtime cost
    • Disposal or replacement cost

    For small plants, where margins are tight, life-cycle cost (TCO) is often the most important criterion. A slightly higher upfront investment in efficient, reliable equipment usually pays back many times over.

    Maintainability

    Maintainability considerations in industrial plant equipment selection

    Equipment must be maintainable. This means:

    • Access: Can it be reached for inspection and repair?
    • Disassembly: Can components be removed and replaced without major work?
    • Standardization: Are parts standard, or are they proprietary and slow to source?
    • Documentation: Are manuals, drawings, and procedures available?
    • Training: Can your team operate and maintain it, or is specialist support required?

    For small plants, maintainability is often overlooked. Equipment that is difficult to service leads to longer downtime, higher costs, and more reliance on external support.

    Lead Time and Schedule

    Lead time is the time between placing an order and receiving the equipment. For long-lead items such as turbines, generators, and large vessels, lead times can be 12 to 24 months or more.

    Lead time affects:

    • Project schedule: Long-lead items determine the critical path.
    • Procurement planning: Orders must be placed early enough to meet schedule.
    • Storage and preservation: Equipment delivered early must be stored and protected.
    • Vendor capacity: Popular vendors may be booked out for months.

    For small plants, lead time is often a constraint. Early identification of long-lead items allows procurement to start as soon as the design is firm.

    Vendor Support

    The equipment vendor is a partner for the life of the plant. Good vendor support includes:

    • Spare parts availability: Can parts be sourced quickly?
    • Technical support: Is help available when problems arise?
    • Warranty: What is covered, and for how long?
    • Service agreements: Are maintenance and overhaul services available?
    • Training: Does the vendor provide training for your team?

    A vendor with strong support may be worth a higher price. A vendor with poor support can leave you stranded when equipment fails.

    Spare Parts Strategy

    Availability from the vendor is only half the question. The other half is what to hold on site. For critical equipment, consider whether to stock spare parts on-site or rely on vendor delivery. Remote plants often justify carrying key spares, because a single missing part can idle the plant for weeks. A practical approach is to ask each vendor for a recommended spares list, then stock the items that are critical to operation, have long lead times, or are unlikely to be available locally. Weigh the carrying cost of these spares against the cost of downtime.

    Compliance and Standards

    Equipment must comply with applicable codes, standards, and regulations. These may include:

    • Pressure vessel codes: ASME, PED, or local equivalents
    • Electrical standards: IEC, NEC, or local equivalents
    • Environmental regulations: Emissions limits, noise limits, and discharge requirements
    • Safety standards: ATEX, NFPA, or local equivalents

    Compliance is not optional. Equipment that does not meet applicable standards cannot be legally operated, and may not be insurable.

    Common Equipment Selection Mistakes

    Even experienced designers make mistakes. Common ones include:

    • Selecting on price alone: Ignoring efficiency, reliability, and maintenance costs
    • Oversizing equipment: Adding unnecessary margin that increases cost and reduces efficiency
    • Undersizing equipment: Leaving no margin for actual operating conditions
    • Ignoring part-load performance: Optimizing for design point only
    • Overlooking lead time: Discovering too late that equipment cannot be delivered on schedule
    • Neglecting vendor support: Choosing a vendor with no local presence or spare parts
    • Skipping life-cycle cost analysis: Comparing only purchase prices

    These mistakes are costly to fix after equipment is installed. They are much cheaper to avoid during selection.

    How Japanese EPC Firms Approach Equipment Selection

    Japanese engineering firms are known for their disciplined approach to equipment selection. Common characteristics include:

    • Conservative sizing: Equipment is specified with adequate margin, but not excessive.
    • Emphasis on reliability: Proven equipment and vendors are preferred over untested alternatives.
    • Life-cycle cost focus: Purchase price is evaluated alongside operating and maintenance costs.
    • Long-term vendor relationships: Established vendors with strong support are favored.
    • Detailed documentation: Specifications, datasheets, and test records are carefully maintained.

    For plant owners, this often means equipment that performs reliably for decades, even if the initial price is higher than some alternatives.

    How to Evaluate Equipment Selection

    When reviewing equipment selections, ask:

    Question Why It Matters
    Does it meet process requirements? Ensures the plant can achieve its design output
    Can it support the performance guarantees? Prevents a marginal item from causing the plant to fall short
    Is it reliable? Reduces downtime and maintenance cost
    Is it efficient? Reduces operating cost over the plant’s life
    What is the life-cycle cost (TCO)? Captures total cost, not just purchase price
    Is it maintainable? Reduces downtime and reliance on external support
    Can it be delivered on schedule? Keeps the project on track
    Does the vendor provide good support, and are critical spares covered? Ensures spare parts and technical help are available
    Does it comply with standards? Ensures legal and safe operation

    A selection that satisfies all these questions is likely to perform well over the plant’s life.

    Conclusion

    Equipment selection is not just a procurement exercise. It is a strategic decision that affects cost, reliability, efficiency, and long-term performance. For small to medium-scale industrial plants, where margins are tight and redundancy is limited, equipment selection deserves careful attention from the earliest stages of design.

    By focusing on technical suitability, reliability, efficiency, life-cycle cost, maintainability, lead time, vendor support, and compliance, owners and designers can select equipment that performs reliably and economically for decades.
    Key Takeaways

    • Equipment selection affects cost, reliability, efficiency, and long-term performance.
    • Life-cycle cost (total cost of ownership), not just purchase price, should drive decisions.
    • Reliability and maintainability matter more in small plants with limited redundancy.
    • Standard, proven equipment and a sensible on-site spares strategy reduce cost, lead time, and downtime.
    • Lead time and vendor support are critical for schedule and long-term operation.
    • Japanese EPC firms favor conservative sizing, proven vendors, and detailed documentation.
  • Key Considerations in Small-Scale Industrial Plant Layout Design

    Key Considerations in Small-Scale Industrial Plant Layout Design

    Plant layout is one of the most consequential decisions in industrial plant design. It affects construction cost, operating efficiency, maintenance access, safety, and future expansion. For small-scale industrial plants, layout decisions are especially critical because there is less space to work with and less margin for error.

    This article covers the key considerations that drive effective layout design for small to medium-scale industrial plants. Whether you are planning a biomass facility, a small thermal plant, or a process plant, these principles apply.

    Plot Plan vs. Equipment Layout

    Two related but distinct documents define a plant’s layout:

    • Plot plan: The site-level arrangement of buildings, roads, major equipment, tanks, utilities, and boundaries.
    • Equipment layout: The detailed arrangement of equipment, piping, and access within a building, structure, or process area.

    For small plants, the plot plan often determines whether the project is feasible at all. Site boundaries, setbacks, access roads, and separation distances are fixed early, and they constrain everything that follows. This article addresses both levels, but the plot plan should be settled before detailed equipment layout begins.

    Why Layout Matters More for Small Plants

    Large plants often have enough space to accommodate imperfect layouts. Small plants do not. Every meter counts. A poorly planned layout in a small plant can lead to:

    • Higher construction cost: Extra piping, longer cable runs, and additional structural steel.
    • Inefficient operations: Longer travel distances for operators and maintenance staff.
    • Safety risks: Inadequate separation between hazardous areas.
    • Limited expansion: No room to add equipment or capacity later.
    • Maintenance difficulties: Equipment that cannot be accessed for service.

    For these reasons, layout should be treated as a strategic decision, not a drafting exercise.

    The Core Objectives of Plant Layout

    Core objectives of industrial plant layout design

    A good layout achieves several objectives simultaneously:

    Objective What It Means
    Minimize capital cost Reduce piping, cabling, and structural requirements
    Optimize operations Place equipment in logical process order
    Ensure safety Separate hazardous areas and provide clear escape routes
    Enable maintenance Provide access for inspection, repair, and replacement
    Allow expansion Reserve space for future equipment or capacity increase
    Facilitate construction Allow efficient sequencing of civil, mechanical, and electrical work

    These objectives sometimes conflict. For example, minimizing cost may push equipment closer together, but safety and maintenance requirements may demand more space. Good layout design balances these trade-offs.

    Key Considerations

    1. Process Flow

    Process flow diagram for industrial plant layout design

    The layout should follow the process flow as closely as possible. Raw material should enter at one end, and finished product or output should exit at the other. This minimizes piping runs, reduces pressure drops, and simplifies operation.

    For small plants, a linear or L-shaped layout often works best. Linear layouts minimize piping runs and simplify construction, while L-shaped layouts allow the plant to fit into constrained sites while preserving process flow. Both are simple, efficient, and easy to expand.

    2. Equipment Spacing

    Equipment must be spaced to allow:

    • Operation: Space for operators to monitor and adjust equipment.
    • Maintenance: Room to remove and replace components such as heat exchangers, pumps, and motors.
    • Safety: Adequate distance between hot surfaces, electrical equipment, and flammable materials.
    • Ventilation: Airflow to prevent heat buildup and gas accumulation.

    Manufacturers typically provide minimum clearance recommendations. These should be treated as minimums, not targets.

    3. Piping, Pipe Racks, and Cable Routing

    Piping and cabling are significant cost drivers. A layout that minimizes the length and complexity of these runs reduces both capital cost and pressure losses.

    Key principles:

    • Group equipment that shares piping or cabling connections.
    • Use common pipe racks and cable trays where possible.
    • Avoid unnecessary elevation changes in piping.
    • Route cables away from hot or hazardous areas.

    Pipe racks as the backbone of the layout. In many plants, the pipe rack is the organizing element around which everything else is arranged. Its location drives equipment spacing, since equipment is typically placed along both sides of the rack. It also drives construction sequence, because rack foundations and steel are often erected early so that piping and cable trays can be installed as equipment arrives. Deciding rack location and routing early, ideally alongside the plot plan, avoids expensive rework later. Leave spare capacity on the rack for future lines, and keep power and instrument cable trays segregated from process piping according to applicable standards.

    4. Access and Egress

    Safe access is essential. The layout must provide:

    • Primary access routes: For normal operations and maintenance.
    • Emergency egress routes: For evacuation during an incident.
    • Vehicle access: For deliveries, mobile equipment, and emergency response.
    • Pedestrian access: Separate from vehicle routes where possible.

    In small plants, access routes often do double duty. This requires careful planning to avoid conflicts.

    5. Safety, Hazard Separation, and Regulatory Compliance

    Safety should be a primary driver of layout, not an afterthought. Key considerations include:

    • Separation distances: Between hazardous and non-hazardous areas.
    • Fire zones: Segregation of equipment by fire risk.
    • Explosion protection: Location of electrical equipment relative to flammable areas.
    • Toxic gas dispersion: Placement of vents and stacks relative to occupied areas.
    • Emergency shutdown: Access to isolation valves and controls.

    Recognized codes and standards (such as NFPA, IEC, and API) provide guidance on separation distances. These must be respected.

    Regulatory compliance. Local regulations often dictate separation distances, fire zone requirements, and emergency access routes. These must be identified early, as they can constrain the layout significantly. A layout that is efficient on paper but fails a permit review can force a costly redesign.

    6. Maintenance and Replacement

    Equipment must be accessible for maintenance. The layout should allow:

    • Removal of major components: Heat exchanger tubes, turbine rotors, and pump internals.
    • Lifting access: Overhead clearance for cranes or mobile lifting equipment.
    • Workspace: Room for maintenance personnel and tools.
    • Spare parts storage: Nearby but not blocking access.

    For small plants, maintenance access is often compromised by tight layout. This should be addressed early in design, not discovered during operation.

    Operation vs. maintenance. Layout for operation and layout for maintenance sometimes conflict. A compact layout may be efficient for operations but difficult for maintenance. The trade-off should be evaluated explicitly.

    7. Future Expansion

    Even small plants sometimes need to expand. A good layout reserves space for:

    • Additional equipment: Parallel process lines, additional pumps, or extra capacity.
    • Utility upgrades: Larger transformers, additional cooling capacity.
    • Control system expansion: Space for additional panels or instruments.
    • Site infrastructure: Roads, parking, and storage.

    Expansion space should be identified during initial design, even if expansion is not certain.

    8. Construction Sequence

    Layout affects how the plant is built. A layout that allows efficient construction sequencing can reduce schedule and cost. Key considerations include:

    • Access for construction equipment: Cranes, trucks, and heavy lift equipment.
    • Laydown areas: Space for temporary storage of materials and equipment.
    • Sequencing: Ability to install equipment in a logical order without blocking access.
    • Temporary facilities: Site offices, warehouses, and worker facilities.

    For small plants, construction access is often constrained. Early planning helps avoid delays.

    9. 3D Modeling and Clash Detection

    Modern layout design uses 3D modeling to detect clashes between piping, structural, and electrical systems before construction begins. This reduces field changes and rework. In tight small-plant layouts, where piping, steel, cable trays, and maintenance envelopes compete for the same space, clash detection is especially valuable. The 3D model can also be used to check maintenance access and lifting paths, not just physical interferences.

    Common Layout Mistakes

    Even experienced designers make mistakes. Common ones include:

    • Insufficient maintenance access: Equipment installed too close to walls or other equipment.
    • Ignoring expansion: No space reserved for future needs.
    • Poor process flow: Equipment arranged inefficiently, increasing piping and operating cost.
    • Inadequate safety separation: Hazardous areas too close to occupied areas.
    • Overlooking construction access: Equipment that cannot be delivered or installed.
    • Forgetting utilities: Insufficient space for piping, cabling, and instrumentation.

    These mistakes are costly to fix after construction begins. They are much cheaper to avoid during design.

    How Japanese EPC Firms Approach Layout

    Japanese engineering firms often take a disciplined approach to plant layout. Common characteristics include:

    • Thorough front-end planning: Layout is developed early and refined through multiple reviews.
    • Attention to detail: Clearances, access routes, and maintenance space are carefully considered.
    • Safety focus: Hazard separation and emergency access are prioritized.
    • Long-term perspective: Expansion space is reserved even when not immediately needed.
    • Constructability review: Layout is evaluated for ease of construction, not just operation.

    For plant owners, this often means a layout that is efficient, safe, and adaptable to future needs.

    How to Evaluate a Layout

    When reviewing a proposed layout, ask:

    Question Why It Matters
    Does it follow the process flow? Minimizes piping and operating cost
    Is there adequate maintenance access? Reduces downtime and maintenance cost
    Are safety separations respected? Protects people and assets
    Is there space for expansion? Avoids costly future modifications
    Can it be constructed efficiently? Reduces schedule and cost
    Are utilities properly routed? Avoids conflicts and inefficiencies
    Is it compliant with regulations? Ensures legal and safe operation

    A layout that satisfies all these questions is likely to perform well over the plant’s life.

    Conclusion

    Plant layout is not just a drawing exercise. It is a strategic decision that affects cost, safety, operations, and future flexibility. For small-scale industrial plants, where space is limited and margins are tight, layout deserves careful attention from the earliest stages of design.

    By focusing on process flow, equipment spacing, safety, maintenance access, and expansion, owners and designers can create layouts that are efficient, safe, and built to last.

    Key Takeaways

    • Plant layout affects cost, safety, operations, and future flexibility.
    • The plot plan often determines project feasibility, so settle it before detailed equipment layout.
    • Process flow should drive the overall arrangement.
    • Equipment spacing must allow operation, maintenance, and safety.
    • Access and egress must be planned for normal and emergency conditions.
    • Local regulations should be identified early, since they can constrain the layout significantly.
    • 3D modeling and clash detection reduce field changes and rework.
    • Japanese EPC firms emphasize front-end planning and constructability review.
  • The Three Stages of EPC Project Delivery: Engineering, Procurement, Construction

    The Three Stages of EPC Project Delivery: Engineering, Procurement, Construction

    An EPC contract is often described as a single, unified delivery method. But behind that single contract are three distinct stages, each with its own activities, risks, and deliverables. Understanding how these stages fit together helps plant owners know what to expect at each phase and where problems are most likely to arise.

    This article walks through the three stages of EPC project delivery, explains what happens in each, and highlights the key points where owners should pay close attention.

    Stage 1: Engineering

    Engineering stage of EPC project delivery showing design documents

    The engineering stage is where the plant is designed. Under the EPC contract, it begins after the contract is signed and continues until the design is complete enough to support procurement and construction. Engineering support typically continues through construction to handle field changes and prepare as-built documentation.

    A note on FEED: In many projects, a front-end engineering design (FEED) phase precedes the EPC contract. FEED defines the basic design, cost estimate, and schedule that form the basis for the EPC bid. A well-executed FEED reduces the risk of scope changes during detailed engineering.

    Engineering typically includes:

    • Basic design: Process flow diagrams, heat and mass balances, and overall plant layout.
    • Detailed design: Equipment specifications, piping and instrumentation diagrams (P&IDs), electrical drawings, and civil/structural drawings.
    • Engineering calculations: Equipment sizing, pipe sizing, structural analysis, and control system logic.
    • Technical documentation: Datasheets, equipment lists, and operating manuals.

    Why Engineering Matters Most

    The engineering stage has an outsized influence on the project’s success. Decisions made here determine:

    • Capital cost: Equipment selection and layout decisions set most of the project’s capital cost before a single item is purchased.
    • Operating cost: Efficiency, fuel consumption, and maintenance requirements are set during design.
    • Schedule: Delays in engineering cascade into procurement and construction.
    • Performance: Whether the plant meets its output and efficiency guarantees depends on design choices made at this stage.

    For plant owners, the engineering stage is where you have the most influence. Once construction begins, changes become expensive and slow.

    Key Owner Touchpoints in Engineering

    Owners should be actively involved in:

    Touchpoint Why It Matters
    Design reviews Catch errors before they become costly changes
    Equipment selection Ensure vendor choices match your reliability and maintenance preferences
    HAZOP studies Identify safety risks in the design before construction
    Interface definition Clarify what the owner supplies vs. what the contractor supplies
    Documentation review Ensure drawings and manuals meet your operational needs

    Owner-supplied equipment: Some projects include owner-supplied equipment, where the owner procures certain items directly. This can reduce cost but increases coordination complexity, since the contractor must integrate owner-supplied items into the overall design and schedule.

    Stage 2: Procurement

    Procurement stage of EPC project delivery showing supply chain

    Procurement is the process of sourcing and purchasing all equipment, materials, and services required for the plant. It overlaps with engineering and often extends into construction.

    Procurement activities include:

    • Vendor identification and qualification: Finding suppliers capable of meeting technical and delivery requirements.
    • Request for quotation (RFQ): Issuing specifications and soliciting bids.
    • Bid evaluation: Comparing technical compliance and commercial terms.
    • Purchase orders and contracts: Placing orders and managing supplier agreements.
    • Expediting: Monitoring supplier progress to ensure on-time delivery.
    • Inspection and testing: Verifying equipment meets specifications before shipment.
    • Logistics: Managing shipping, customs, and delivery to site.

    Why Procurement Is a Common Source of Delays

    Procurement is frequently the stage where projects fall behind. Common causes include:

    • Long lead times: Items like turbines, generators, and large vessels can take 12 to 24 months or more to manufacture.
    • Vendor capacity constraints: Popular vendors may be booked out for months.
    • Supply chain disruptions: Material shortages, shipping delays, and customs issues.
    • Quality issues: Equipment that fails inspection must be reworked or replaced.
    • Currency and price volatility: Commodity prices can shift between quotation and order.

    For owners, the lesson is simple: the earlier procurement starts, the better. Long-lead items should be identified during engineering and ordered as soon as the design is firm enough.

    Key Owner Touchpoints in Procurement

    Touchpoint Why It Matters
    Vendor list approval Ensure the contractor is not using unqualified suppliers
    Critical equipment review Verify specifications for major items
    Inspection witness points Attend or send a representative for key factory tests
    Delivery schedule review Confirm long-lead items are on track
    Change order review Approve any scope changes that affect cost or schedule

    Stage 3: Construction

    Construction stage of EPC project delivery at an industrial plant

    Construction is the physical execution of the project. It includes civil works, structural erection, equipment installation, piping, electrical and instrumentation, and commissioning.

    Construction activities include:

    • Site preparation: Earthworks, foundations, and access roads.
    • Civil and structural works: Buildings, structures, and support systems.
    • Mechanical erection: Installation of equipment, piping, and valves.
    • Electrical and instrumentation: Cable trays, wiring, control systems, and instruments.
    • Testing and commissioning: Pressure tests, loop checks, commissioning, and performance testing.
    • Handover: Documentation, training, and final acceptance.

    The importance of commissioning: Commissioning is where the plant is tested under actual operating conditions. This is when performance guarantees are verified through commissioning and performance testing, and when any deficiencies must be corrected before acceptance.

    What good handover looks like: Good handover includes complete as-built drawings, equipment manuals, operating procedures, maintenance schedules, and training for the owner’s team. Incomplete handover documentation is a common source of problems during the first years of operation.

    Why Construction Is the Most Visible Stage

    Construction is where the project becomes tangible. It is also where:

    • Safety risks are highest: Heavy lifting, working at height, and live electrical work.
    • Coordination is most complex: Multiple subcontractors must work in sequence.
    • Schedule pressure is most intense: Every delay compounds.
    • Quality issues surface: Installation errors, misalignment, and missing components.

    For owners, construction is a period of high activity and high risk. Regular site visits and progress meetings help catch problems early.

    Key Owner Touchpoints in Construction

    Touchpoint Why It Matters
    Site progress meetings Track actual vs. planned progress
    Safety audits Ensure contractor is maintaining safety standards
    Quality inspections Verify installation meets specifications
    Witness testing Observe pressure tests and loop checks
    Punch list review Ensure outstanding items are completed before handover
    Commissioning attendance Verify the plant operates as designed

    How the Three Stages Overlap

    While it is convenient to describe engineering, procurement, and construction as sequential stages, in practice they overlap significantly.

    Stage Typical Overlap
    Engineering → Procurement Procurement of long-lead items begins before detailed design is complete
    Procurement → Construction Early construction (civil works) starts while equipment is still being manufactured
    Engineering → Construction Design changes during construction are common but costly

    This overlap is one reason EPC delivery is complex. The contractor must manage multiple activities simultaneously while maintaining schedule and budget.

    Managing the interfaces: The overlap between stages is a common source of disputes. If engineering is not sufficiently advanced, procurement may order equipment that later needs modification. If procurement is delayed, construction may start before key equipment is available. Managing these interfaces is one of the contractor’s most important responsibilities.

    Why Japanese EPC Firms Excel at This

    Japanese EPC firms are known for managing the three stages with particular discipline. Key characteristics include:

    • Front-loaded engineering: More time spent on design before construction begins, reducing costly changes later.
    • Careful procurement planning: Long-lead items identified early and ordered promptly.
    • Strong site management: Detailed construction planning, safety focus, and quality control.
    • Integrated communication: Engineering, procurement, and construction teams work closely together.

    For plant owners, this often translates into a smoother project with fewer surprises, even if the initial schedule appears slower.

    What Owners Should Focus On

    Across all three stages, owners should prioritize:

    1. Clear scope definition before the contract is signed.
    2. Active participation in design reviews and key decisions.
    3. Regular progress monitoring during procurement and construction.
    4. Documentation of all changes, approvals, and decisions.
    5. Commissioning involvement to ensure the plant meets its guarantees.

    Conclusion

    The three stages of EPC project delivery (engineering, procurement, and construction) form the backbone of any plant project. Each stage has its own activities, risks, and owner touchpoints. Understanding how they fit together helps owners anticipate problems, ask the right questions, and keep the project on track.

    Whether you are building a small biomass plant or a medium-scale thermal facility, the principles are the same: good engineering drives good procurement, and good procurement enables good construction.

    Key Takeaways

    • EPC delivery has three stages: engineering, procurement, and construction.
    • Engineering has the greatest influence on cost, schedule, and performance.
    • Procurement is a common source of delays, especially for long-lead items.
    • Construction is the most visible stage and carries the highest safety and coordination risk.
    • The stages overlap significantly, and managing interfaces is critical.
    • Japanese EPC firms emphasize front-loaded engineering and careful procurement planning.
  • EPCM vs. EPC: Which Delivery Model Is Right for Your Plant?

    EPCM vs. EPC: Which Delivery Model Is Right for Your Plant?

    When planning an industrial plant, one of the earliest and most consequential decisions is how to structure the contract with your engineering partner. Two models dominate the conversation: EPC and EPCM. They sound similar and are often confused, but they represent fundamentally different approaches to project delivery.

    For owners of small to medium-scale plants, understanding the difference is critical. The wrong choice can leave you with more risk than you expected, or more administrative burden than you can handle.

    This article explains both models, compares them side by side, and helps you decide which one fits your project.

    What Is EPC?

    EPC stands for Engineering, Procurement, and Construction. In this model, a single contractor takes full responsibility for the project, from detailed design through to commissioning.

    The EPC contractor:

    • Performs all engineering and design work
    • Procures all equipment and materials
    • Manages and executes all construction activities
    • Delivers a completed, operational plant

    The owner signs one contract, pays one price (usually a lump sum), and receives a facility that is ready to operate. This is often called turnkey delivery.

    What Is EPCM?

    EPCM stands for Engineering, Procurement, and Construction Management. The key word is Management.

    In an EPCM arrangement, the contractor:

    • Performs engineering and design work
    • Manages procurement on behalf of the owner
    • Manages construction contractors on behalf of the owner
    • Does not carry out construction directly

    The owner holds the individual construction contracts. The EPCM contractor acts as the owner’s agent, coordinating and supervising the work but not taking financial responsibility for the construction itself.

    In EPCM delivery, the owner may also engage an independent owner’s engineer to review the EPCM contractor’s work. This adds another layer of oversight but requires additional coordination.

    The Fundamental Difference

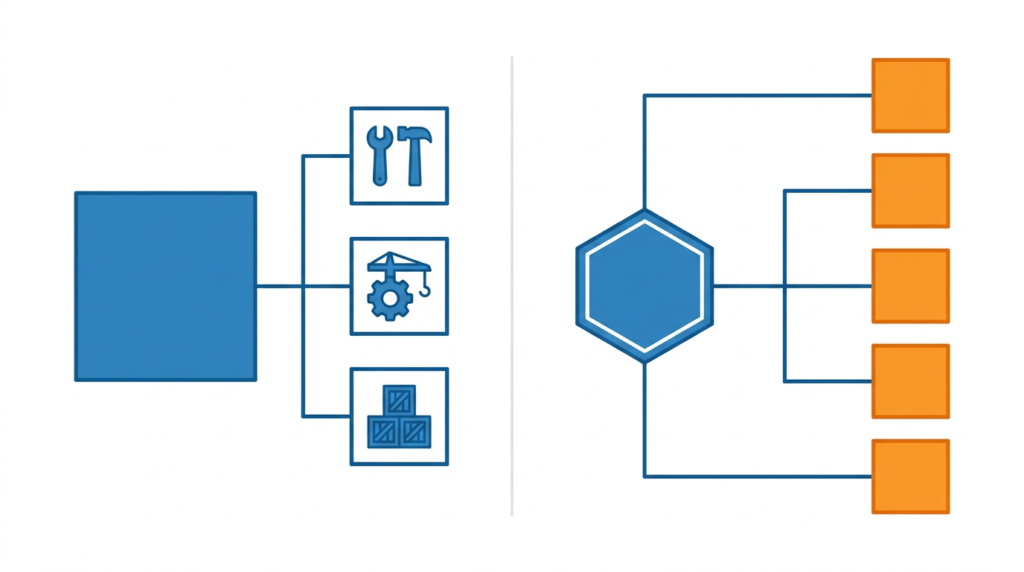
    EPC and EPCM contract structure comparison diagram

    The simplest way to understand the difference is this:

    EPC: The contractor builds the plant and hands you the keys.

    EPCM: The contractor manages the building of the plant while you hold the contracts.

    In EPC, the contractor carries the risk of cost overruns and schedule delays. In EPCM, the owner carries most of that risk, and the EPCM contractor is paid a fee for managing the process.

    EPC also provides greater schedule certainty, since the contractor is responsible for coordinating all activities. In EPCM, schedule risk sits largely with the owner, since the owner holds the individual contracts and the EPCM contractor’s role is to coordinate them.

    Side-by-Side Comparison

    Factor EPC EPCM
    Contract structure Single contract with one contractor Multiple contracts; owner holds construction contracts
    Risk bearer Contractor (for most construction risk) Owner
    Cost certainty High (lump-sum price) Lower (cost-plus or reimbursable)
    Schedule certainty Higher (one party coordinates all activities) Lower (owner holds the contracts)
    Owner involvement Lower High
    Owner staffing needs Limited Significant
    Flexibility for changes Low (changes are costly) Higher (owner can adjust scope)
    Contractor’s role Single point of responsibility Manager/agent
    Typical project size Small to large Medium to very large

    When EPC Makes Sense

    EPC is often the right choice when:

    • The owner lacks in-house engineering staff. Without a technical team to manage multiple contractors, EPC transfers that burden to the contractor.
    • Cost certainty is critical. Lenders and investors often prefer EPC because the lump-sum price reduces financial uncertainty. Lenders prefer EPC because the fixed price and single point of responsibility reduce the risk of cost overruns and delays that could affect debt service. Some lenders require EPC delivery as a condition of financing.
    • The project is well-defined. If the scope is clear and unlikely to change, EPC locks in price and schedule.
    • The plant is small to medium-scale. For smaller plants, the overhead of managing multiple contracts may not be justified.

    For most small to medium-scale industrial plants, EPC is the default choice for these reasons.

    When EPCM Makes Sense

    EPCM is often the right choice when:

    • The owner has strong in-house engineering capability. If you have the technical team to oversee design and construction, EPCM gives you more control.
    • The project is large and complex. Very large projects often use EPCM because few contractors are willing to absorb the risk of a lump-sum price at that scale.
    • Flexibility is important. If the scope is likely to evolve, EPCM allows changes without the heavy penalties typical of EPC contracts.
    • The owner wants to retain control over key decisions. EPCM keeps the owner in the driver’s seat for equipment selection, contractor selection, and design changes.

    The Risk Trade-Off

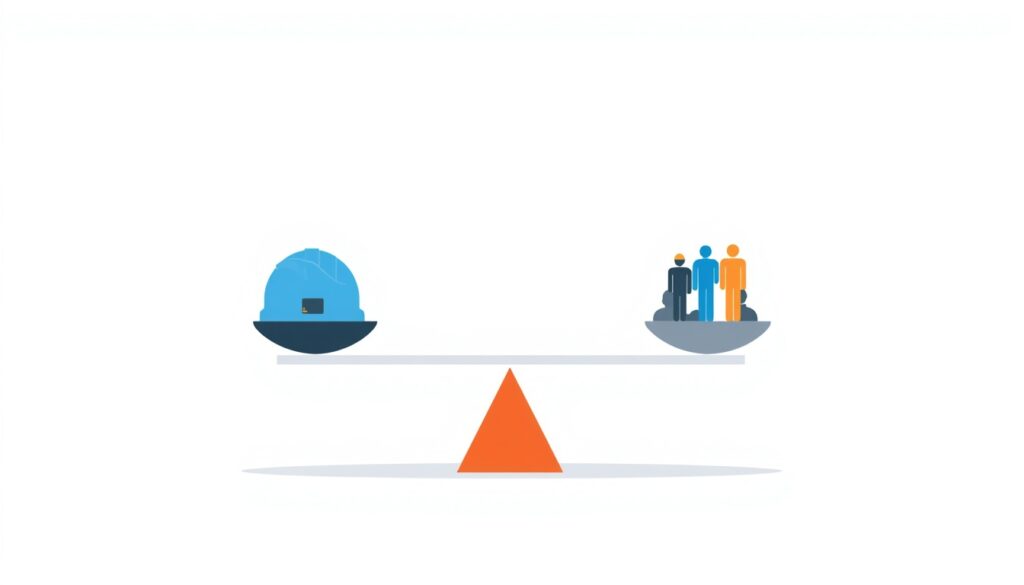
    Risk distribution comparison between EPC and EPCM models

    The core trade-off between EPC and EPCM is risk versus control.

    EPC EPCM
    Risk Contractor bears most risk Owner bears most risk
    Control Owner has less control Owner has more control
    Cost Higher price (includes a risk premium), but predictable Lower management fee, but total project cost is uncertain
    Effort Lower owner effort Higher owner effort

    There is no universally correct answer. The right choice depends on your team’s capabilities, your project’s complexity, and your appetite for risk.

    Hybrid and Variant Models

    The choice is not always strictly EPC or EPCM. In practice, some projects use hybrid models. For example, the main process plant may be delivered under EPC while balance-of-plant works are managed under EPCM. These hybrids can capture the benefits of both models, but they require careful interface management.

    Another variant is sometimes called “EPC-Lite” or “open book EPC.” Here, the contractor takes EPC-style responsibility for delivering the plant, but the owner has visibility into actual costs. This suits owners who want cost certainty but also transparency. Because these terms are not standardized, always confirm in the contract exactly what the contractor guarantees and how costs, savings, and overruns are shared.

    Common Mistakes Owners Make

    1. Choosing EPC without understanding the scope.
    If the scope is not clearly defined, an EPC contractor will either price in a large contingency or refuse to bid. Vague scopes lead to disputes later.

    2. Choosing EPCM without the staff to manage it.
    EPCM requires the owner to make decisions, review designs, and manage interfaces. If you do not have the team for this, EPCM can quickly become overwhelming.

    3. Assuming EPC eliminates all risk.
    EPC transfers most construction risk to the contractor, but the owner can still bear risks that the contract does not transfer, such as those tied to permits, owner-provided information, and, depending on the contract terms, site conditions. The owner also takes over operation and maintenance after handover.

    4. Assuming EPCM is always cheaper.
    EPCM fees may be lower, but the owner absorbs cost overruns. In a volatile market, EPCM can end up costing more than a fixed-price EPC.

    How Japanese EPC Firms Approach This

    Japanese engineering firms often favor EPC delivery for small to medium-scale plants. This reflects several common characteristics of Japanese project delivery:

    • Preference for clear responsibility: A single point of accountability aligns with a strong emphasis on clear roles and ownership of outcomes.
    • Long-term relationships: Japanese firms often work with trusted subcontractors, reducing the coordination burden that EPCM requires.
    • Conservative risk assessment: Japanese contractors tend to price EPC contracts carefully, avoiding the aggressive bidding that can lead to disputes.
    • Quality focus: EPC allows the contractor to control quality across design, procurement, and construction.

    For plant owners working with Japanese EPC firms, this often means a smoother project with fewer surprises, though the initial price may be higher than some competitors.

    How to Decide

    Ask yourself these questions:

    1. Do we have in-house engineering staff? If no, EPC is likely the better choice.
    2. Is cost or schedule certainty a priority? If yes, EPC provides more predictable pricing and timelines.
    3. Is the scope likely to change? If yes, EPCM offers more flexibility.
    4. Do we want to be deeply involved in decisions? If yes, EPCM gives you more control.
    5. What is our risk tolerance? If low, EPC shifts risk to the contractor.
    6. Would a hybrid or open-book approach fit? If you want a mix of certainty, transparency, and control, discuss these options with your contractor.

    For most small to medium-scale industrial plants, EPC is the practical choice. It simplifies management, provides cost and schedule certainty, and matches the scale of the project.

    Conclusion

    EPC and EPCM are both valid delivery models, but they serve different purposes. EPC transfers risk and responsibility to a single contractor, while EPCM keeps the owner in control at the cost of higher involvement and risk.

    Understanding the difference, and choosing the model that matches your team, your project, and your risk appetite, is one of the most important decisions you will make. Get it right, and the project starts on solid ground. Get it wrong, and you may find yourself managing a project you were not prepared to handle.

    Key Takeaways

    • EPC: single contractor, lump-sum price, contractor bears most risk
    • EPCM: owner holds contracts, EPCM contractor manages on the owner’s behalf
    • EPC offers cost and schedule certainty; EPCM offers flexibility and control
    • Choose EPC if you lack in-house engineering staff or need cost certainty
    • Choose EPCM if you have strong in-house capability or need flexibility
    • Japanese EPC firms often favor EPC for small to medium-scale plants
  • Understanding Performance Guarantees in EPC Contracts

    Understanding Performance Guarantees in EPC Contracts

    When a plant owner signs an EPC contract, a large part of the final payment is tied to one critical milestone: proving that the plant actually performs as promised. This is where performance guarantees come in. They are among the most important, and most negotiated, sections of any EPC agreement.

    For owners of small to medium-scale industrial plants, understanding how performance guarantees work is essential. A well-written guarantee protects your investment. A vague or weak one can leave you with a plant that never reaches its designed output.

    What Are Performance Guarantees?

    Performance guarantees are contractual commitments by the EPC contractor that the completed plant will meet specific measurable targets. These targets are set in the contract, usually based on the front-end engineering and bidding phase, and confirmed through performance tests before the owner takes over the plant.

    If the plant fails to meet these targets, the contractor is usually required to either:

    • Correct the deficiency at their own cost, or
    • Pay liquidated damages as compensation for the shortfall.

    In some cases, both remedies apply. The contractor may attempt a fix first, and if the fix fails, financial compensation is triggered.

    Guarantees vs. warranties. Performance guarantees are distinct from warranties. A guarantee commits the contractor to achieving specific measurable targets. A warranty covers defects in equipment or workmanship for a defined period. Both matter, but they address different risks.

    Common Performance Metrics

    Key performance metrics for industrial plant EPC contracts

    Different plant types use different metrics, but most EPC contracts include some combination of the following:

    Metric What It Measures Typical Application
    Net Power Output Electrical output delivered at the plant boundary, after deducting the plant’s own auxiliary consumption Power plants
    Heat Rate Fuel input per unit of electrical output (lower is better) Thermal and combined cycle plants
    Steam Flow and Quality Steam production rate and purity Boilers and process plants
    Emissions Levels NOx, SOx, particulate matter Plants with environmental permits
    Availability Percentage of time the plant is operational All plant types
    Reliability Frequency of forced outages All plant types

    For small to medium-scale plants, the most common guarantees are net output, heat rate, and availability. These three metrics together determine whether the plant is commercially viable. Note that availability and reliability cannot be proven in a short test. They are usually demonstrated through a reliability run or an extended period of operation.

    How Performance Guarantees Are Structured

    A typical performance guarantee section in an EPC contract includes several distinct elements.

    Guaranteed Values

    These are the specific numerical targets the contractor commits to. For example: “Net power output shall be no less than 25 MW at reference conditions.” Output-type guarantees are stated as minimums, while heat rate and emissions guarantees are stated as maximums.

    Most guarantees apply at full load or a specified reference load. If the plant is expected to operate frequently at part load, consider whether separate part-load guarantees are appropriate.

    Guaranteed values must also be expressed in clearly defined units. For heat rate, for example, the contract should state whether it is based on the lower heating value (LHV) or higher heating value (HHV) of the fuel, since the two differ significantly. Ambiguity in units can lead to disputes.

    Reference Conditions

    Performance depends heavily on ambient temperature, humidity, altitude, fuel composition, and cooling water temperature. The contract must specify the exact conditions under which the guarantee applies. A guarantee at 15°C ambient is very different from one at 35°C. Because tests rarely happen at exactly the reference conditions, the contract should also define the correction curves used to adjust measured results back to them.

    Test Procedures

    The contract should define how performance will be measured. This includes which instruments are used, who witnesses the test, and how data is recorded. Recognized industry standards such as ASME PTC, ISO, or IEC are often referenced.

    Test timing. Performance tests are typically conducted after commissioning, when the plant is stable and can be operated at full load. The contract should specify how long after completion the tests must occur, and what happens if conditions are not suitable for testing.

    Tolerance Bands and Measurement Uncertainty

    Most guarantees allow for a small margin to account for measurement uncertainty. This is usually expressed as a percentage. For example: “Net output shall be no less than 25 MW; the guarantee is met if corrected test output is at least 99.5% of that value.”

    All performance measurements have some uncertainty. The contract should define how uncertainty is handled: whether it is subtracted from the guaranteed value, added to the measured value, or treated separately. This affects how much margin the contractor must build into the design.

    Remedies for Shortfall

    If the plant fails to meet the guarantee, the contract specifies what happens next. This may include:

    • A defined period for the contractor to investigate and correct the issue
    • Liquidated damages calculated per unit of shortfall
    • A cap on total liquidated damages
    • Minimum performance levels, below which the owner can reject the plant entirely

    Correction vs. buy-down. Some contracts allow the contractor to “buy down” a shortfall, that is, pay liquidated damages instead of correcting the deficiency. This can be acceptable if the shortfall is small and the owner is compensated fairly. But for significant shortfalls, correction should be required.

    Liquidated Damages: How They Work

    Liquidated damages concept for EPC contract performance shortfall

    Liquidated damages (LDs) are pre-agreed financial amounts. They are not meant to punish the contractor but to compensate the owner for losses caused by underperformance.

    A typical LD formula for power output might look like this:

    LD = (Guaranteed Output − Corrected Test Output) × LD Rate per kW

    The LD rate is negotiated based on the value of the revenue the owner would lose from the shortfall over the plant’s evaluation period, so the rate already reflects the lifetime impact. For heat rate, the formula is similar, but the rate reflects the present value of additional fuel costs over the plant’s expected life.

    For international projects, ensure that LD rates are stated in a defined currency and that any currency conversion is specified. Ambiguity in currency can lead to disputes.

    Important: Most contracts include a cap on total liquidated damages, often expressed as a percentage of the contract price. Caps commonly fall somewhere between 5% and 20%, depending on the project and market. Owners who push for much higher caps often find that contractors price in extra risk or decline to bid.

    Common Pitfalls for Plant Owners

    Performance guarantees are only valuable if they are enforceable. Here are the most common mistakes owners make:

    1. Vague or missing reference conditions. If the contract does not clearly define the conditions under which performance is measured, the contractor can argue that the guarantee does not apply to actual site conditions.

    2. Weak test procedures. If the contract does not specify which standards apply or who witnesses the test, disputes are likely.

    3. Low liquidated damages. If the LD rate is too low, the contractor may simply pay the penalty rather than invest in fixing the problem. The LD rate should reflect the real cost of underperformance to the owner.

    4. No deadline for correction. Without limits, a contractor could repeatedly attempt fixes while the plant remains non-compliant. The contract should set a deadline for achieving compliance.

    5. Missing long-term guarantees. Some contracts only guarantee performance at initial testing. If performance degrades after six months, the owner may have no recourse. Consider whether a longer-term guarantee is appropriate, and how it fits alongside the warranty.

    The Role of Japanese EPC Practices

    Japanese engineering firms are often known for a conservative approach to performance guarantees. This can mean:

    • More margin in design: Equipment is specified with more headroom, reducing the risk of falling short.
    • Thorough pre-test preparation: Performance tests are rehearsed and instrumented carefully.
    • Transparent communication: Potential shortfalls tend to be disclosed early rather than discovered during testing.
    • Long-term mindset: Many Japanese firms place a high priority on meeting guarantees because their reputation depends on repeat business.

    For plant owners, this can mean fewer disputes during the performance test phase, though the initial design may appear more conservative than competitors’ proposals.

    What to Negotiate Before Signing

    If you are reviewing an EPC contract, pay close attention to these areas:

    Area What to Check
    Guaranteed values Are they realistic? Do they match your business case?
    Units and basis Are units clearly defined (e.g., LHV or HHV for heat rate)?
    Part-load performance Do you need separate part-load guarantees?
    Reference conditions Do they match your actual site conditions?
    Test procedures Are they clearly defined and based on recognized standards?
    Test timing When must tests occur, and what if conditions are unsuitable?
    Measurement uncertainty Is it handled explicitly, and in whose favor?
    LD formula Does the rate reflect your actual revenue loss?
    LD cap Is it high enough to incentivize performance?
    Correction and buy-down Is there a firm deadline, and are buy-down rights limited to small shortfalls?
    Currency Are LD rates and any conversions clearly specified?
    Long-term guarantees Are there provisions for performance degradation over time?

    Conclusion

    Performance guarantees are the mechanism that ensures an EPC contractor delivers what was promised. For plant owners, they are not just a legal formality. They are the primary protection against a plant that fails to meet its commercial objectives.

    Understanding the structure, the common metrics, and the pitfalls helps owners negotiate better contracts and avoid costly disputes. Whether you are building a small biomass plant or a medium-scale thermal facility, the principles are the same: clear targets, clear tests, and clear consequences.

    Key Takeaways

    • Performance guarantees commit the contractor to measurable targets, while warranties cover defects
    • Common metrics include net output, heat rate, and availability
    • Reference conditions and test procedures must be clearly defined
    • Liquidated damages compensate the owner for shortfalls
    • Weak guarantees lead to disputes; strong ones protect the owner
    • Japanese EPC firms often take a conservative approach to guarantees
  • EPC Contracts Explained: A Beginner’s Guide for Plant Owners

    EPC Contracts Explained: A Beginner’s Guide for Plant Owners

    When a company decides to build an industrial plant, whether it’s a biomass facility, a small thermal power plant, or a process plant, one of the first major decisions is how to structure the contract with the engineering firm. For many plant owners, the term “EPC” appears early in discussions, but its full implications are not always clear.

    This guide explains what an EPC contract is, how it differs from other delivery models, and what owners of small to medium-scale plants should consider before signing.

    What Does EPC Stand For?

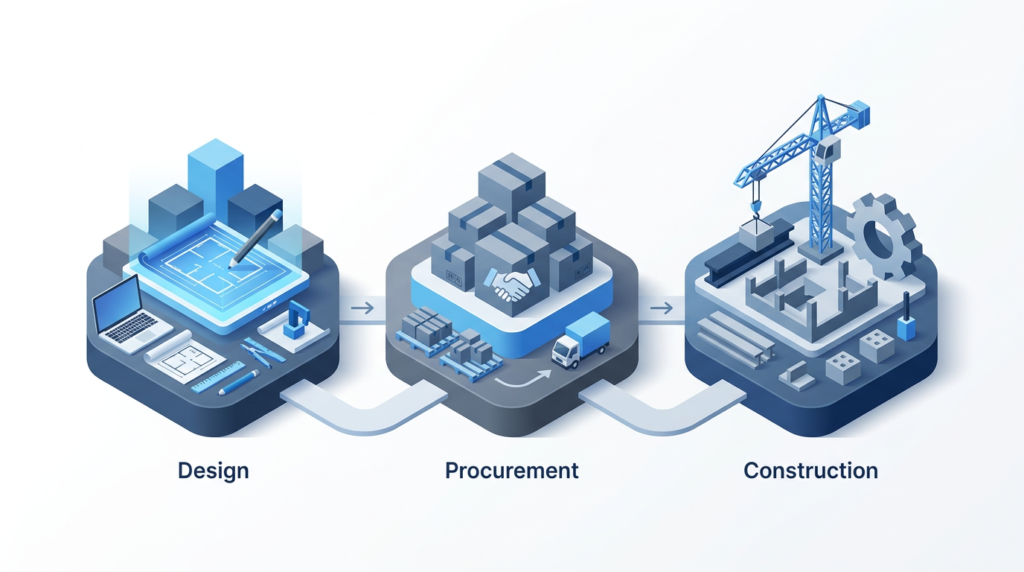
    Three phases of EPC contract delivery illustration

    EPC stands for Engineering, Procurement, and Construction. It is a contract model in which a single contractor takes responsibility for the entire project delivery, from detailed design through to commissioning.

    Under a traditional EPC arrangement, the contractor is responsible for:

    • Engineering: Detailed design, technical specifications, drawings, and engineering calculations.
    • Procurement: Sourcing and purchasing all equipment, materials, and components.
    • Construction: Civil works, erection, installation, testing, and commissioning.

    The owner receives a facility that is ready to operate, often described as “turnkey” delivery. In many cases, the EPC contractor also carries responsibility for performance guarantees, such as output capacity or efficiency targets.

    EPC vs. Turnkey

    While EPC and turnkey are often used interchangeably, they are not identical. Turnkey implies the contractor hands over a fully operational facility, while EPC may allow for some owner involvement or retained responsibilities. In practice, most EPC contracts are turnkey, but the terms should be confirmed in the contract.

    Why EPC Emerged

    EPC emerged as a response to the complexity of large industrial projects, where coordinating multiple contractors often led to delays, cost overruns, and disputes. By consolidating responsibility under one contractor, EPC reduces the owner’s coordination burden and provides a clearer path to completion.

    How EPC Differs From Other Delivery Models

    EPC is not the only way to deliver a plant. Understanding the alternatives helps clarify why EPC is often chosen for industrial projects.

    Delivery Model Contractor Responsibility Owner Risk
    EPC / Turnkey Design, procurement, construction Lower (single point of responsibility)
    EPCM Engineering, procurement, and construction management; owner holds the construction contracts Medium
    Design-Bid-Build Separate contracts for design and construction High (coordination risk)
    Design-Build Design and construction combined Medium

    Comparison of EPC and other plant project delivery models
    EPC concentrates responsibility with a single contractor, reducing owner risk.

    EPC concentrates responsibility with a single contractor, reducing the owner’s interface and coordination risk.

    For small to medium-scale plants, EPC is often attractive because the owner does not need to manage multiple contractors or coordinate interfaces between design and construction. This reduces administrative burden and transfers much of the risk to the contractor.

    Why EPC Is Common for Small to Medium-Scale Plants

    Large utility-scale projects sometimes use EPCM or multi-contract models because owners have in-house engineering teams. For smaller plants, however, the owner may not have the technical staff to manage multiple contractors.

    EPC offers several practical advantages:

    • Single point of responsibility: If something goes wrong, there is one party accountable.
    • Predictable cost and schedule: Lump-sum pricing (see below) fixes the price for a defined scope, although approved changes can still adjust it.
    • Reduced owner staffing needs: The contractor manages day-to-day coordination.
    • Performance guarantees: The contractor is often contractually bound to meet output or efficiency targets.

    How EPC Contracts Are Awarded

    EPC contracts are usually awarded through a competitive bidding process. Contractors receive a detailed scope and technical specification, then submit technical and commercial proposals. Evaluation typically considers technical compliance, price, schedule, and the contractor’s track record.

    Key Elements of an EPC Contract

    EPC contract document with engineering drawings and safety equipment

    While every contract is negotiated, most EPC agreements share common elements. These include:

    • Scope of Work: A detailed definition of what is included, and excluded, from the contract.
    • Price and Payment Terms: Typically milestone-based payments tied to progress.
    • Schedule and Milestones: Key dates for design completion, equipment delivery, and commissioning.
    • Performance Guarantees: Targets for capacity, heat rate, emissions, or other metrics.
    • Liquidated Damages: Pre-agreed compensation if the contractor misses deadlines or performance targets.
    • Warranty and Defect Liability: The period during which the contractor must fix defects at no cost.
    • Bonds and Insurance: Financial protections provided by the contractor.
    • Dispute Resolution: How disagreements are handled and under which law.
    • Force Majeure: Provisions for events beyond either party’s control.

    For owners, the most important sections are often the scope definition and the performance guarantees, because these determine what the contractor is actually obligated to deliver.

    Lump-Sum vs. Reimbursable Pricing

    Most EPC contracts use lump-sum pricing, where the contractor agrees to a fixed price for a defined scope. Some contracts use reimbursable or cost-plus pricing, where the owner pays actual costs plus a fee. Lump-sum transfers more risk to the contractor but usually costs more; reimbursable shifts risk to the owner but may be less expensive if the scope is uncertain.

    Bonds and Insurance

    EPC contracts typically require the contractor to provide performance bonds, advance payment guarantees, and insurance. These protect the owner if the contractor fails to perform or becomes insolvent.

    Dispute Resolution

    EPC contracts typically include provisions for dispute resolution, often through arbitration or expert determination before litigation. The choice of governing law and dispute resolution forum should be considered carefully, especially for international projects.

    The Owner’s Representative

    Even in EPC delivery, the owner typically retains an owner’s representative or project manager to monitor progress, review designs, and approve milestones. This role is lighter than in EPCM delivery but still important.

    Common Pitfalls for Plant Owners

    Even with a well-drafted contract, problems can arise. Some common issues include:

    • Incomplete scope definition: Leading to disputes over what is included.
    • Unrealistic schedules: Causing pressure to cut corners during commissioning.
    • Weak performance guarantees: Allowing the contractor to avoid accountability.
    • Insufficient owner review: Failing to verify design assumptions before construction begins.
    • Poor interface management: Especially when the owner supplies certain equipment or services.

    These issues are not unique to EPC contracts, but they are more consequential because the owner has less direct involvement in day-to-day execution.

    How Japanese EPC Practices Differ

    Japanese engineering team reviewing plant design drawings

    Japanese engineering firms are known for their emphasis on quality, safety, and long-term reliability. In EPC delivery, this often translates into:

    • Detailed front-end engineering: More time spent on design before construction begins.
    • Strong documentation: Comprehensive records for operation and maintenance.
    • Conservative design margins: Equipment sized with more margin for reliability.
    • Long-term client relationships: A focus on repeat business rather than one-off transactions.

    For plant owners, working with a Japanese EPC firm or EPC support partner can mean a slower start but fewer surprises during commissioning and operation.

    What to Look For in an EPC Partner

    When evaluating EPC contractors or support firms, consider:

    • Experience with similar plant types and scales
    • Track record in your region or country
    • Depth of engineering staff, not just project managers
    • Willingness to share references and past project data
    • Understanding of local regulations and standards
    • Ability to provide long-term support after handover

    For small to medium-scale plants, a specialized EPC support firm may offer more flexibility than a large contractor focused on utility-scale projects.

    Conclusion

    EPC contracts are a proven delivery model for industrial plants, particularly when the owner wants a single point of responsibility and predictable outcomes. Understanding the structure, risks, and key contract terms helps owners make better decisions and avoid common pitfalls.

    If you are planning a small to medium-scale plant and considering an EPC approach, the most important step is to define your requirements clearly and select a partner with relevant experience and a commitment to quality.

    Key Takeaways

    • EPC stands for Engineering, Procurement, and Construction.
    • A single contractor takes responsibility for design, procurement, and construction.
    • EPC is common for small to medium-scale plants because it reduces owner coordination burden.
    • Most EPC contracts are lump-sum; reimbursable pricing shifts more risk to the owner.
    • Contracts are usually awarded through competitive bidding on a detailed scope and specification.
    • Key contract elements include scope, price, schedule, performance guarantees, and liquidated damages.
    • Performance bonds, advance payment guarantees, and insurance protect the owner.
    • The owner still needs a representative to monitor progress, review designs, and approve milestones.
    • Common pitfalls include incomplete scope, unrealistic schedules, and weak guarantees.
    • Japanese EPC firms emphasize front-end engineering, documentation, and long-term relationships.