Most industrial plants are designed for a finite life, typically 20 to 40 years depending on the industry, the equipment and the design basis. Many plants operate well beyond that. Equipment is replaced, systems are upgraded, and the plant continues to produce. Others reach a point where life extension is no longer economic, and replacement becomes the better option.
Plant life extension (PLEX) is the process of assessing, planning, and executing the work needed to keep an aging plant operating safely, reliably, and economically beyond its original design life. It is a strategic decision that affects capital investment, operating cost, safety, and regulatory compliance.
For small to medium-scale industrial plants, life extension decisions are especially important because there is less redundancy and fewer resources to absorb the consequences of a wrong decision. Extending the life of a plant that should be replaced wastes money. Replacing a plant that could be extended safely wastes capital.
This article covers the key considerations in plant life extension, from assessment to execution.
What Is Plant Life Extension?
Plant life extension is the set of activities required to continue operating a plant beyond its original design life while maintaining safety, reliability, and compliance.
It is worth separating two terms. Design life is the period the plant was originally designed and analyzed for. Useful life is how long the plant can actually operate safely and economically. Design life is a starting assumption, not a hard limit. Some equipment fails earlier because of poor operation or maintenance, and well-maintained equipment often lasts much longer.
Life extension is not simply “keeping the plant running.” It involves:
- Assessment: Evaluating the condition and remaining life of equipment and systems.
- Planning: Identifying what work is needed and when.
- Investment: Funding the required repairs, replacements, and upgrades.
- Execution: Performing the work, often during turnarounds.
- Monitoring: Tracking performance and condition over time.
Life extension can range from a few years of incremental work to a major program of replacement and upgrade.
Why Life Extension Matters
Life extension decisions have significant consequences.
| Factor | Impact of Good Life Extension | Impact of Poor Life Extension |
|---|---|---|
| Safety | Equipment maintained within safe limits | Aging equipment creates safety risks |
| Reliability | Failures managed before they occur | Increasing failures and unplanned outages |
| Cost | Capital deployed where it adds most value | Money wasted on the wrong equipment |
| Compliance | Regulatory requirements met | Non-compliance, fines, or forced shutdown |
| Production | Output maintained or improved | Declining performance and output |
| Business case | Investment justified and returns achieved | Poor returns; capital stranded |
| Insurance and financing | Insurers and lenders confident in the plant’s condition | Higher premiums, restricted cover, or difficulty financing |
For small plants, life extension is often the main alternative to building a new plant, which may be prohibitively expensive.
The Case for Life Extension
Life extension is often justified when:
- The plant is in good condition: Equipment has been well maintained.
- The remaining life is sufficient: The plant can operate for years with targeted investment.
- Replacement is expensive: Building a new plant is not economically viable.
- Demand exists: The plant’s output is still needed.
- Regulatory compliance is achievable: The plant can meet current and foreseeable requirements.
- Upgrades add value: Efficiency, capacity, or flexibility improvements justify investment.
Life extension is not always the right choice. Sometimes replacement is better, especially if the plant is in poor condition, compliance is not achievable, or demand is declining.
The Case Against Life Extension
Life extension may not be justified when:
- The plant is in poor condition: Equipment is degraded beyond economic repair.
- Compliance is not achievable: The plant cannot meet current or foreseeable regulations.
- Replacement is cheaper: The cost of life extension, including the risk of future outages, exceeds the cost of a new plant.
- Demand is declining: The plant’s output is no longer needed.
- Technology is obsolete: Spare parts, expertise, and support are unavailable.
- Safety risks are unacceptable: The plant cannot be operated safely.
The decision requires an honest assessment of both the plant and the business case.
Key Drivers of Plant Aging
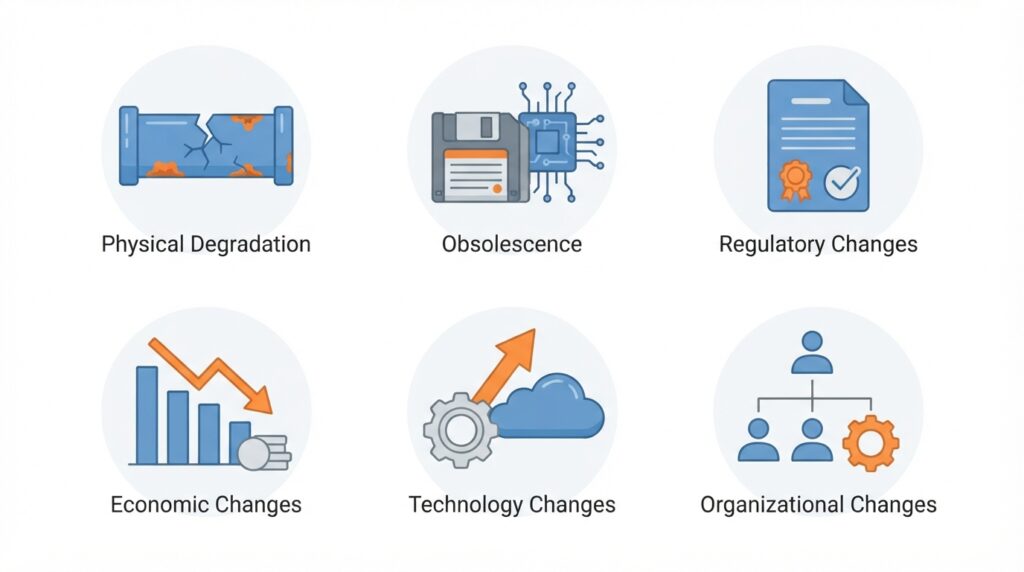
Plants age for several reasons.
| Driver | Description | Examples |
|---|---|---|
| Physical degradation | Wear, corrosion, fatigue, erosion, and other damage mechanisms | Pipe wall thinning, bearing wear, refractory degradation, creep in high-temperature piping, thermal fatigue, embrittlement, hydrogen damage |
| Obsolescence | Technology no longer supported | Control systems, instrumentation, spare parts |
| Regulatory changes | New or stricter requirements | Emissions limits, safety standards |
| Economic changes | Market, fuel, or cost changes | Fuel price increases, competition |
| Technology changes | New technology makes old obsolete | More efficient equipment, digital controls |
| Organizational changes | Loss of expertise, changing priorities | Retirement of experienced staff |
Understanding which drivers apply to your plant helps focus life extension efforts. Physical degradation is the one most people think of first, but obsolescence and organizational change can cause problems sooner than expected.
Assessing Remaining Life
The first step in life extension is assessing the condition and remaining life of equipment and systems.
| Method | Description | Application |
|---|---|---|
| Condition assessment | Physical inspection and testing | Piping, vessels, structures |
| Remaining life analysis | Engineering calculations based on condition | Pressure vessels, piping, turbines |
| Failure history review | Analysis of past failures and repairs | All equipment |
| Performance testing | Measuring current performance | Turbines, compressors, heat exchangers |
| Obsolescence review | Identifying equipment at risk of obsolescence | Control systems, instrumentation |
| Compliance review | Identifying regulatory gaps | All systems |
Assessment should cover all major equipment and systems, not just the most visible ones. It also depends on good records. Original design data, as-built drawings, operating history, inspection reports, and repair records are the baseline against which condition is judged. If they are missing or unreliable, rebuilding them is the first job of the assessment.
Design Basis and Code Gap Review
A plant built 30 years ago was designed to the codes, standards, and practices of that time. Before committing to life extension, compare the original design basis with current requirements. Common gaps include pressure equipment codes, fire protection and electrical standards, safety instrumented system requirements, structural and seismic criteria, and environmental limits.
Not every gap must be closed. Legal requirements for older plants vary by jurisdiction and by whether the work is a modification or a continuation of existing operation. A documented gap review helps the owner and the regulator agree on what must be upgraded, what can be justified by other measures, and what is acceptable as is. Skipping this review is a common way for hidden compliance costs to surface mid-program.
Fitness-for-Service Assessment
Fitness-for-service (FFS) assessment evaluates whether equipment with known defects or degradation can continue to operate safely. Standards such as API 579-1/ASME FFS-1 provide methodologies for assessing remaining strength and life. FFS is especially useful for pressure equipment with corrosion, cracking, or wall loss. It can show that equipment is acceptable as is, acceptable with a reduced operating envelope or a shorter inspection interval, or in need of repair or replacement. That often avoids unnecessary replacement and supports a defensible decision.
Risk-Based Inspection
Risk-based inspection (RBI) prioritizes inspection based on the likelihood and consequence of failure. It helps direct limited inspection resources to the equipment that matters most. Recognized practices such as API 580 and API 581 provide the framework. For small plants with limited inspection budgets, RBI helps ensure the highest-risk equipment gets the most attention while low-risk items are inspected less often.
Using Remaining Life in Maintenance Planning
Remaining life assessment should feed directly into maintenance planning and drive decisions: equipment approaching the end of its remaining life should be scheduled for replacement or refurbishment, not just monitored. Remaining life estimates are not fixed. They should be updated as new inspection data, operating history, and changes in operating conditions become available.
Inspection, Testing, and Monitoring Techniques
Remaining life estimates are only as good as the data behind them. Common techniques include:
| Technique | Typical Use |
|---|---|
| Visual and remote inspection (borescope, drones, crawlers) | Vessels, tanks, stacks, boilers, hard-to-reach areas |
| Ultrasonic thickness and flaw detection | Wall loss, cracking, weld quality |
| Radiography and magnetic particle / dye penetrant testing | Welds, surface cracks |
| Metallurgical methods (hardness, replication, sampling) | Creep damage, embrittlement, material degradation in high-temperature service |
| Vibration, thermography, oil analysis | Rotating equipment, electrical connections, lubrication condition |
| Electrical testing (insulation resistance, partial discharge, transformer oil analysis) | Transformers, motors, cables, switchgear |
| Structural surveys and concrete/steel testing | Foundations, pipe racks, buildings, stacks |
| Online and continuous monitoring | Tracking trends between inspections |
Where data is limited, inspect more or use more conservative assumptions. For equipment with significant temperature or pressure cycling, track accumulated damage (starts, stops, and load changes), because operating history consumes life as well as calendar age.
Critical Equipment and Systems
Some equipment and systems are more critical to life extension than others. Common critical items include:
- Pressure vessels and piping: Subject to corrosion, fatigue, creep, and regulatory inspection.
- Rotating equipment: Turbines, compressors, pumps, and motors.
- Boilers and heat exchangers: Subject to fouling, corrosion, and thermal fatigue.
- Electrical systems: Transformers, switchgear, motors, and cables, including insulation aging.
- Control systems: Often the first to become obsolete.
- Structures and foundations: Subject to corrosion and structural degradation.
- Safety systems: Must be maintained and updated to current standards.
- Long-lead and non-redundant items: Equipment that is hard to replace quickly or whose failure stops the whole plant.
Critical items should be assessed first and in more detail. A useful way to rank them is by combining the consequence of failure (safety, environment, production, cost) with the likelihood of failure based on condition.
Equipment-Specific Life Considerations
| Equipment | Typical Life-Limiting Mechanisms | Typical Life Extension Actions |
|---|---|---|
| Boilers and heat recovery equipment | Tube wall loss, creep, thermal fatigue, fireside and waterside corrosion | Tube replacement, header and weld inspection, water chemistry improvement |
| Steam and gas turbines | Creep, low-cycle fatigue, erosion, blade damage | Major overhauls, component replacement, rotor life assessment |
| Pressure vessels and piping | Corrosion, cracking, creep (high temperature), fatigue | FFS assessment, repair, re-rating, replacement of sections |
| Pumps, compressors, motors | Wear, vibration, bearing and seal failure, insulation aging | Refurbishment, rewinding, re-rating or replacement |
| Transformers and switchgear | Insulation degradation, contact wear, moisture | Testing, oil treatment, refurbishment, replacement |
| Control and instrumentation | Obsolescence, component failure | Phased or full migration to modern systems |
| Structures and foundations | Corrosion, concrete deterioration, settlement | Surveys, repair, strengthening, protective coatings |
This table is a starting point. The right actions depend on the equipment’s condition and duty.
Life Extension Strategies
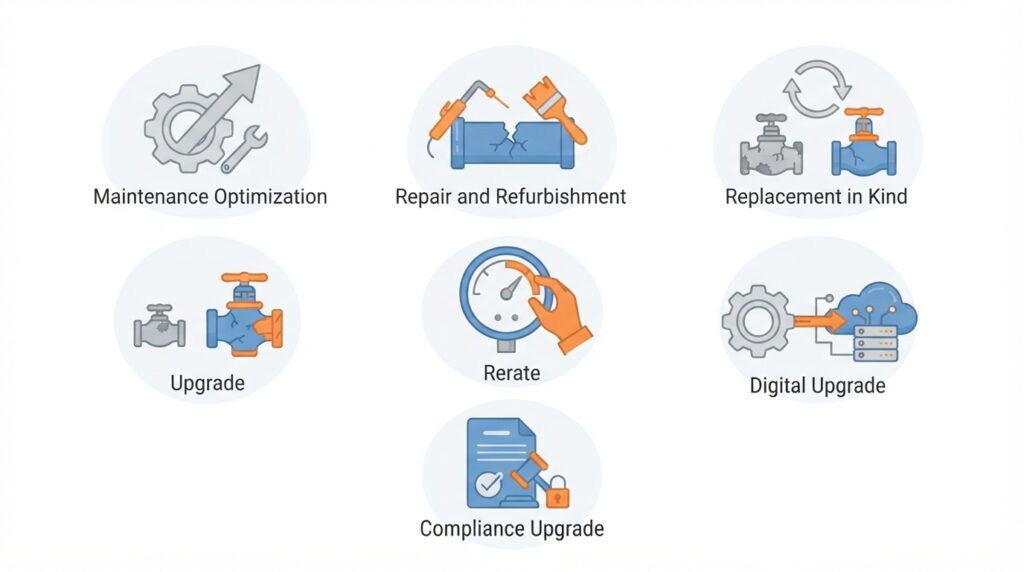
Several strategies can be used to extend plant life.
| Strategy | Description | When to Use |
|---|---|---|
| Maintenance optimization | Improve maintenance to extend equipment life | When equipment is in reasonable condition |
| Repair and refurbishment | Repair or refurbish degraded equipment | When repair is cheaper than replacement |
| Replacement in kind | Replace with identical or equivalent equipment | When the original design is still suitable |
| Upgrade | Replace with improved equipment | When improvements justify investment |
| Rerate | Increase capacity or efficiency | When demand or economics justify |
| Digital upgrade | Modernize controls and monitoring | When obsolescence is a concern |
| Compliance upgrade | Meet new regulatory requirements | When regulations require it |
A rerate changes the conditions the plant was designed for, so pressure relief, piping, electrical, and control systems must be rechecked against the new operating envelope.
Strategies can be combined. A life extension program may include maintenance optimization, targeted replacement, and control system upgrades. Any change to equipment, design, or operating conditions should go through a formal management of change (MOC) process. Major work should be followed by a pre-startup safety review (PSSR) before the plant returns to service.
Planning Life Extension
Life extension should be planned as a program, not a series of individual projects.
Planning elements:
- Objectives: What is the target life extension (for example, 10 years or 20 years)?
- Scope: What work is required to achieve the objectives?
- Schedule: When will the work be performed?
- Budget: What is the cost, and how will it be funded?
- Resources: Who will do the work, and what skills are needed?
- Risk: What are the risks, and how will they be managed?
- Approvals: Who approves the plan, and what is the process?
Planning should begin well before the plant reaches the end of its original design life. Many owners find a staged approach practical:
- Screening: A high-level review of condition, compliance, obsolescence, and economics to decide whether life extension is worth pursuing.
- Detailed assessment: Inspection, testing, remaining life analysis, and FFS work on critical equipment.
- Program definition: Scope, schedule, budget, and risk plan based on the assessment.
- Execution: Work performed in a controlled way, usually during turnarounds.
- Monitoring and review: Condition and performance tracked, and the program updated as findings change.
Staging lets the owner stop early if the screening or assessment shows that replacement is the better option, before large sums are spent.
Spare Parts Strategy
Life extension programs should include a spare parts strategy. Parts for aging equipment may have long lead times or may be obsolete, and should be identified and procured well before they are needed. A good strategy identifies critical spares, reviews what is in stock, checks supplier availability, and decides which parts to buy now, which to source on demand, and which to replace through upgrades. It should be built into the program budget from the start, not discovered when a failure occurs.
Life Extension and Turnarounds
Turnarounds are often the best opportunity to perform life extension work.
Advantages:
- The plant is already shut down.
- Access to equipment is available.
- Contractors and resources are mobilized.
- Work can be coordinated with other maintenance.
Considerations:
- Turnaround scope may need to be expanded.
- Planning must begin earlier.
- Budget must be secured in advance.
- Work must be sequenced with other turnaround activities.
- Long-lead items must be ordered well before the shutdown.
Life extension work that is not done during a turnaround may require a separate outage, which adds cost and lost production. Turnaround inspection findings should also feed back into the remaining life assessment.
Executing Life Extension: Contracting, Contingency, and Quality
Life extension work differs from new construction because the full scope is not known until equipment is opened up. This affects how work should be organized:
- Scope growth is normal. Discovery work (additional repairs found during inspection) should be expected. Budgets and schedules need larger contingency than for comparable new work, and contracts should say how additional scope is priced and approved.
- Phase the work. Early phases (inspection and assessment) can confirm scope before major purchases or contracts are committed.
- Control quality. Materials, welding, and repair procedures should meet applicable codes, with traceability and qualified personnel. Repairs to aging equipment often involve older materials, so compatibility and welding procedures need care.
- Plan restart carefully. After major work, a PSSR, commissioning checks, and performance testing confirm the plant is ready and that expected benefits were achieved.
- Choose the delivery model deliberately. Depending on the owner’s own engineering capability, the work may be self-managed, split among specialist contractors, or given to an EPC contractor.
Life Extension and Obsolescence
Obsolescence is one of the biggest challenges in life extension.
Common obsolescence issues:
- Control systems: Older systems may no longer be supported.
- Instrumentation: Older instruments may be discontinued.
- Spare parts: Parts may no longer be available.
- Software: Older software may not run on modern platforms.
- Expertise: Fewer people know how to maintain older systems.
Obsolescence strategies:
- Identify at-risk items: Which equipment is at risk of obsolescence?
- Last-time buy: Purchase spare parts before discontinuation.
- Alternate sources: Identify substitute parts or suppliers.
- Upgrade: Replace obsolete equipment with modern equivalents.
- Reverse engineering: Manufacture equivalents when needed, with attention to material qualification, quality, and intellectual property.
- Redesign: Modify systems to use available technology.
Obsolescence should be addressed proactively, not reactively.
Digital Upgrades and Cybersecurity
Replacing obsolete control systems usually brings networked, software-based equipment into the plant. This improves monitoring and reliability, but it also brings cybersecurity risk that older standalone systems did not have. A digital upgrade should include network segmentation, access control, patch management, backup and recovery, and training for operations and maintenance staff.
Life Extension and Regulatory Compliance
Regulatory requirements often drive life extension decisions.
Common regulatory issues:
- Emissions limits: New or stricter limits may require equipment upgrades.
- Safety standards: New standards may require safety system upgrades.
- Inspection requirements: Older equipment may require more frequent inspection.
- Environmental requirements: New requirements may affect water, waste, or emissions.
- Operating permits and licenses: Some jurisdictions require formal review or renewal to operate beyond the design life.
Compliance strategies:
- Identify gaps: What requirements does the plant not currently meet?
- Assess options: What are the options for achieving compliance?
- Plan upgrades: When and how will upgrades be performed?
- Monitor changes: Keep track of regulatory developments.
Compliance should be addressed as part of the life extension program, not as a separate effort.
Safety and Risk Review
Life extension must not only keep the plant running but also keep its risk acceptable. Aging increases the likelihood of some failures, and changes made during life extension can introduce new risks.
Good practice includes:
- Revalidating hazard studies (such as HAZOP) for the plant as it now exists, including past modifications.
- Reviewing safety systems. Check that relief devices, alarms, interlocks, and safety instrumented functions still meet their required performance, and re-verify them where components are replaced or conditions have changed.
- Reviewing fire protection and emergency response against the current plant layout and inventory.
- Controlling work hazards. Older plants may contain hazardous materials such as asbestos, lead paint, or PCB-containing oil, which require proper handling during repair and demolition.
- Maintaining a risk register that tracks aging-related risks and the actions taken to manage them.
People and Knowledge
Aging plants often come with an aging workforce. Experienced operators and maintenance staff know the quirks of the plant, the history of repairs, and the workarounds that keep it running. When they retire, that knowledge leaves with them. A life extension program should capture this knowledge through documented procedures, interviews, and training of newer staff. It should also make sure the skills needed for upgraded systems, such as modern control systems and condition monitoring, are available.
Contracts, Permits, and Commercial Alignment
Technical life must match commercial life. Before committing capital, confirm that the extended operating period is supported by:
- Operating permits and licenses valid for the extended period.
- Offtake or supply agreements (for example, power purchase agreements or product supply contracts) that run long enough to recover the investment.
- Land, lease, and site rights that extend to the planned end date.
- Insurance and financing terms consistent with the plan.
A plant that is technically sound but has no contract or permit beyond the next few years may not justify major investment.
Economic Analysis
Life extension decisions should be based on economic analysis.
Analysis elements:
- Capital cost: What is the cost of the life extension work?
- Operating cost: How will operating costs change?
- Revenue: What revenue will the plant generate?
- Remaining life: How long will the plant operate after extension?
- Alternatives: What are the alternatives (replacement, shutdown)?
- Risk: What are the risks, and how are they valued?
Analysis methods:
- Net present value (NPV): Present value of future cash flows minus investment.
- Internal rate of return (IRR): The discount rate at which NPV equals zero; a measure of return on investment.
- Payback period: Time to recover the investment. It is easy to understand but ignores the time value of money and what happens after payback.
- Levelized cost of product: Cost per unit of output over the plant’s life. For power plants this is the levelized cost of electricity (LCOE).
When comparing alternatives with different lives, such as extending for 10 years versus building a plant that lasts 30, use a method that puts them on a comparable basis, such as equivalent annual cost. Include the cost of outages, the cost of risk, and decommissioning costs in the comparison. The economic analysis should be honest and comprehensive. Optimistic assumptions can lead to poor decisions.
Decision Framework: Extend, Partially Replace, Replace, or Retire
Life extension is rarely a yes/no decision. A practical framework considers a range of options:
| Option | When It Fits |
|---|---|
| Extend as is, with maintenance optimization | Condition is good and risks are manageable |
| Targeted repair and replacement | Most equipment is sound; specific items limit life |
| Major refurbishment or rerate | Core equipment is sound and added capacity or efficiency adds value |
| Replace with a new plant or unit | Condition, compliance, or technology makes extension uneconomic |
| Mothball or retire | Demand, economics, or safety no longer support operation |
Compare options on the same basis: cost, risk, performance, schedule, and what happens at the end. An exit plan for decommissioning, including cost and responsibilities, belongs in every option, because life extension only postpones that obligation, and a realistic end date makes the economics more honest.
Common Mistakes in Life Extension
Even experienced organizations make mistakes. Common ones include:
- Deferring assessment: Waiting until problems occur.
- Underestimating scope: Discovering more work than expected.
- Underestimating cost: Budget overruns.
- No contingency for discovery work: Treating inspection findings as a surprise instead of an expectation.
- Ignoring obsolescence: Discovering too late that parts are unavailable.
- Ignoring compliance: Discovering too late that regulations have changed.
- Ignoring commercial limits: Investing in a plant whose permits, contracts, or site rights end soon.
- Optimistic assumptions: Overestimating remaining life or revenue.
- Poor records: Making decisions without reliable design, inspection, or repair data.
- Treating safety as a side issue: Not revalidating hazards and safety systems after years of change.
- Overlooking cybersecurity: Adding networked controls without protecting them.
- Skipping MOC and PSSR: Making changes without proper review.
- No plan: Performing work reactively instead of strategically.
- No follow-through: Failing to complete planned work.
These mistakes can turn a viable life extension into a failed program.
How Japanese EPC Firms Approach Life Extension
Japanese engineering firms are often noted for a disciplined approach to plant life extension. Common characteristics include:
- Thorough assessment: Equipment condition and remaining life are assessed carefully.
- Detailed planning: Life extension is planned as a program, not a series of projects.
- Conservative assumptions: Remaining life and performance are typically estimated conservatively.
- Comprehensive documentation: Assessment, planning, and execution are documented.
- Disciplined execution: Work is performed as planned, with tight control.
- Long-term focus: Life extension is treated as an investment in the plant’s future.
For plant owners, this often means life extension programs that deliver the intended results.
How to Evaluate Life Extension Readiness
When considering life extension for your plant, ask:
| Question | Why It Matters |
|---|---|
| Has equipment condition been assessed? | You cannot plan without knowing condition |
| Has remaining life been estimated, and is it kept up to date? | Determines how long the plant can operate |
| Are design, inspection, and repair records reliable? | Decisions depend on good data |
| Has the design basis been compared with current codes? | Identifies hidden compliance costs |
| Have fitness-for-service and risk-based inspection been considered? | Supports defensible decisions on degraded equipment |
| Have hazard studies and safety systems been revalidated? | Keeps risk acceptable as the plant ages |
| Has obsolescence been reviewed? | Identifies equipment at risk |
| Is there a spare parts strategy? | Prevents delays from long lead times |
| Has compliance been reviewed? | Identifies regulatory gaps |
| Do permits, contracts, and site rights cover the extended life? | Ensures investment can be recovered |
| Is there a life extension plan? | Provides a roadmap for the work |
| Is the economic case sound, with alternatives compared fairly? | Justifies the investment |
| Is there an exit plan for decommissioning? | Makes the economics realistic |
| Are turnarounds planned to include life extension? | Provides the opportunity to perform work |
| Is knowledge being captured from experienced staff? | Protects against loss of expertise |
| Is there a process for monitoring and adjusting? | Keeps the program on track |
A plant that addresses these questions is ready to plan and execute life extension.
Key Takeaways
- Life extension keeps aging plants operating safely, reliably, and economically beyond design life
- The decision requires an honest assessment of both the plant and the business case
- Design life is a starting assumption, not a hard limit; useful life depends on condition and operation
- Key drivers of aging include physical degradation, obsolescence, regulatory changes, and loss of knowledge
- Reliable records and a design basis and code gap review are the foundation of assessment
- Remaining life assessment is the foundation of life extension planning, and it should feed directly into maintenance planning
- Fitness-for-service assessment (for example, API 579) and risk-based inspection help focus effort and avoid unnecessary replacement
- Plan life extension as a staged program; staging allows early exit if replacement is the better option
- Strategies include maintenance optimization, repair, replacement, upgrade, and compliance upgrade, all under MOC and followed by PSSR
- Turnarounds are often the best opportunity to perform life extension work
- Obsolescence and compliance should be addressed proactively, including a spare parts strategy and cybersecurity for digital upgrades
- Revalidate hazards and safety systems; life extension must keep risk acceptable
- Technical life must be supported by permits, contracts, and site rights
- Capture knowledge from experienced staff before it is lost
- Economic analysis should be honest and comprehensive and include alternatives, risk, and end-of-life costs
- Japanese EPC firms emphasize thorough assessment and disciplined planning
Conclusion
Plant life extension is a strategic decision that affects safety, reliability, cost, and compliance. For small to medium-scale industrial plants, it is often the main alternative to building a new plant.
By assessing condition and remaining life, planning as a program, addressing obsolescence and compliance, and executing disciplined work, owners and operators can extend the life of their plants safely, reliably, and economically.